POLYURETHANE PROTOTYPES & SMALL BATCHES
Vacuum Casting
Services
Bridge the gap between a single prototype and production tooling. Get polyurethane parts made from silicone molds, with material, appearance and fit reviewed around your application.
Confidential file handling. Optional NDA ↗
Repeat your design.
Refine the details.
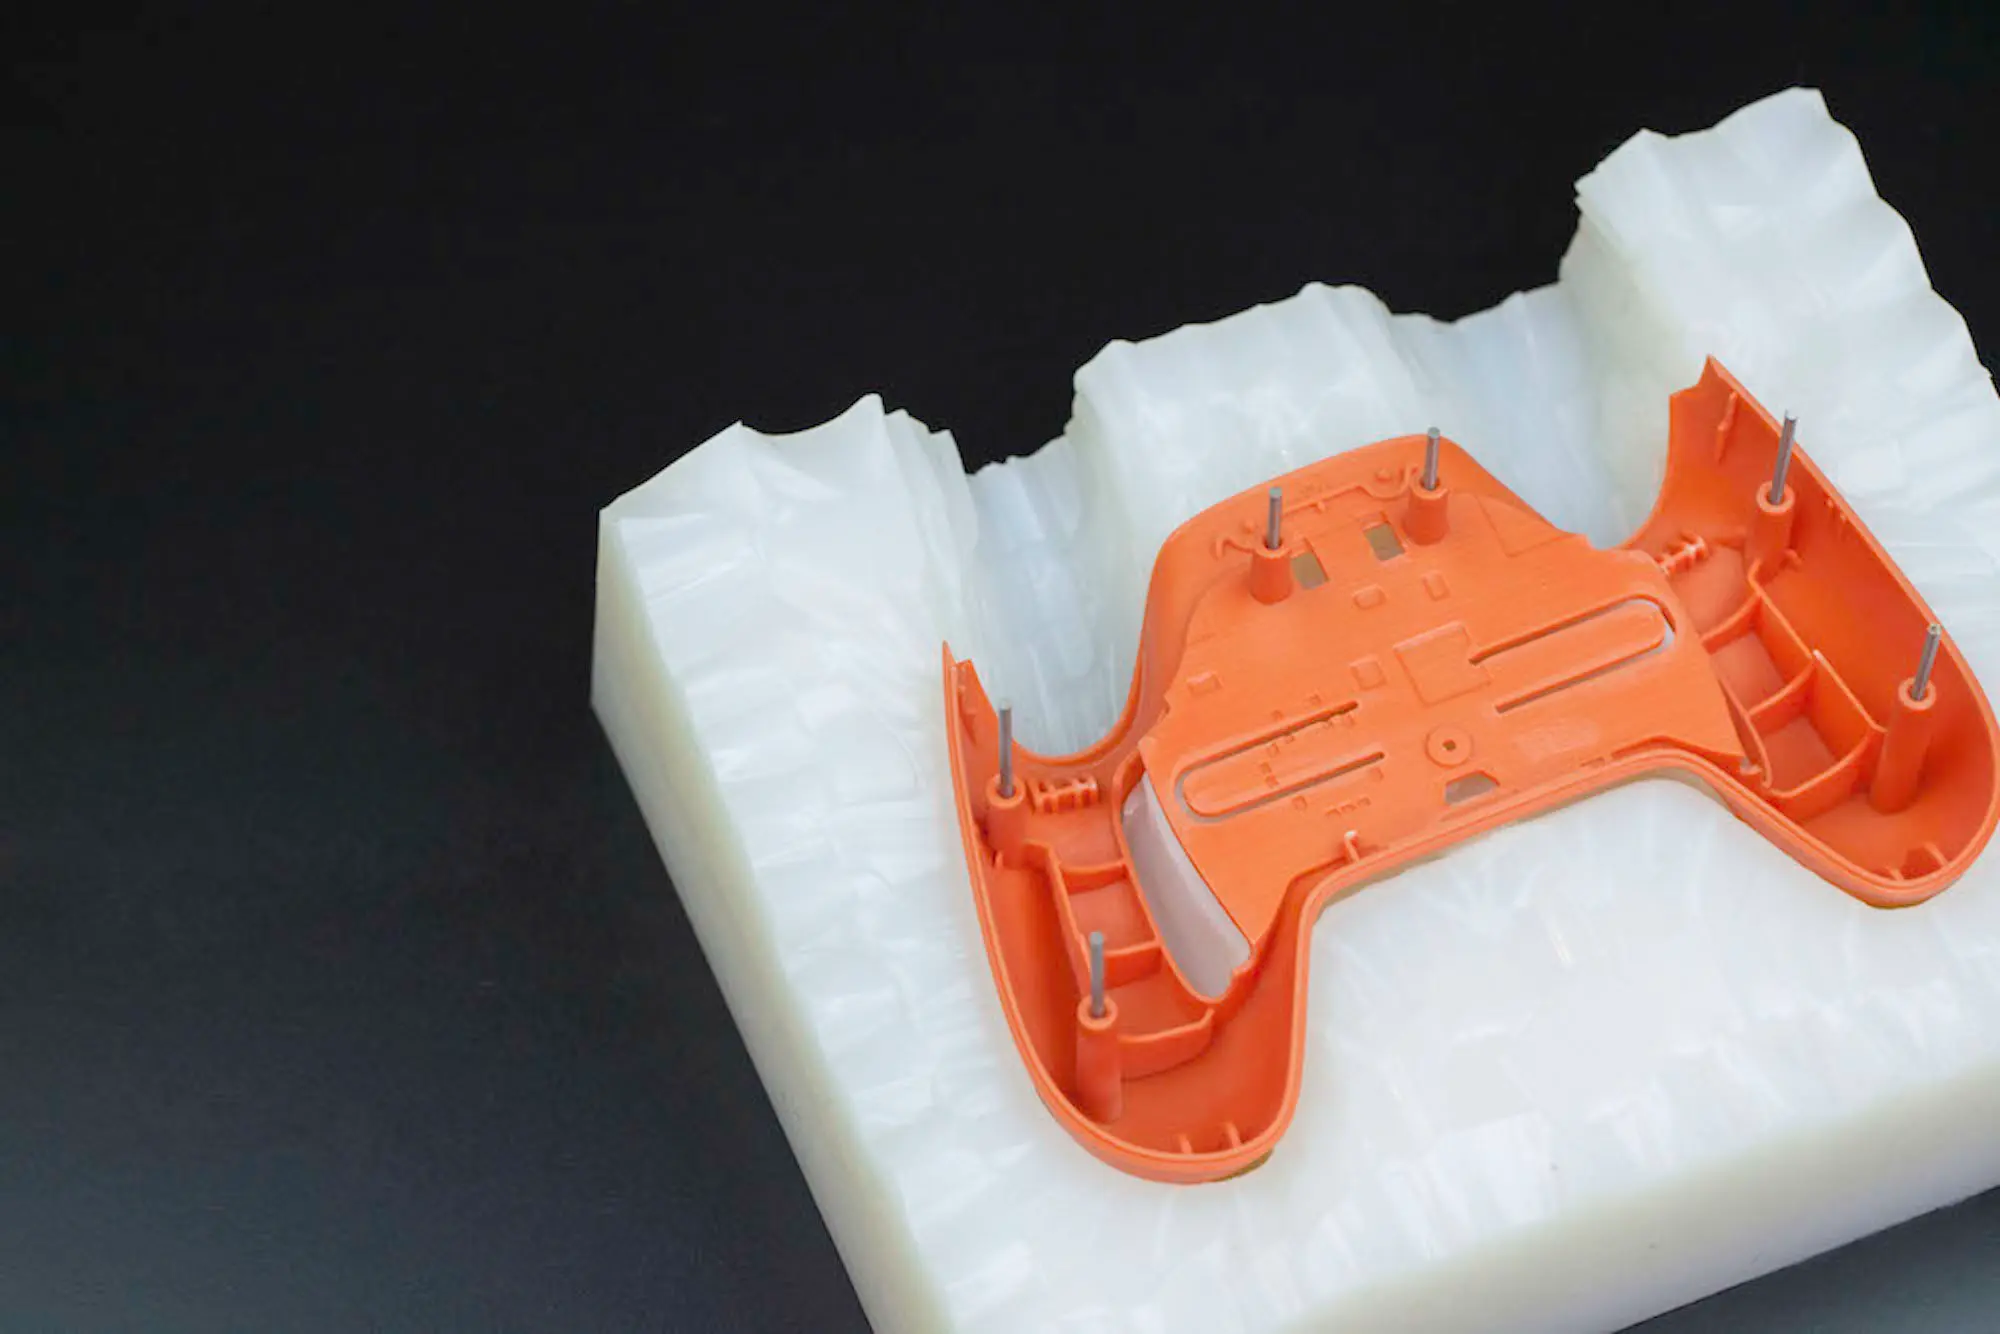
Vacuum casting uses a finished master pattern to create a flexible silicone mold. A liquid resin is mixed, vacuum processed and cured to reproduce the geometry. For polyurethane parts, it is also called urethane casting or polyurethane casting.
Built for a useful next batch
ProleanTech’s vacuum casting service combines master-pattern preparation, silicone tooling, casting and finishing. CNC machining or 3D printing can be used to produce the master, depending on geometry and surface requirements.
Use this route when you need several consistent parts to assess assembly, presentation or an early product launch before investing in production tooling.
Product development teams
Appearance models and repeated enclosure sets for fit reviews, user trials and stakeholder demonstrations.
Procurement & pilot production
A short-run supply option when the design is sufficiently stable and the selected resin meets the actual service conditions.
Engineering validation
Review interfaces and assembly behavior. When tests depend on the final thermoplastic, use parts made in that material and process.
Tell us what the parts need to prove.
Share the use case, quantity and delivery date so the process can be assessed against the project.
Choose the resin by its job.
Then confirm the grade.
“ABS-like” describes a useful comparison, not identical chemistry or performance. Most urethane casting resins are thermosetting polyurethane systems. Select the exact grade from the properties your application needs.
| Material family | Useful for | What to confirm before ordering |
|---|---|---|
| Rigid / ABS-like PU | Housings, covers, handles and assembly prototypes. | Impact strength, stiffness, heat resistance, dimensional stability and post-cure. |
| Tough / PP-like PU | Parts needing more compliance or toughness than a rigid appearance model. | Elongation, fatigue and snap behavior. A PP-like resin does not establish PP living-hinge performance. |
| Clear rigid PU | Transparent appearance models, covers and visualization parts. | Transparency, haze, wall thickness, polish, color stability and UV exposure. |
| Flexible / rubber-like PU | Grips, compliant covers and flexible prototypes. | Shore hardness scale and value, tear strength, compression set and chemical exposure. |
| Specialty resin request | Heat, flame, environmental or other project-specific requirements. | Exact grade availability, supplier datasheet and relevant test documentation before quotation approval. |
Material families are selection guidance. The quotation confirms the resin system and availability; no named supplier grade is implied.
What to send with your material request
Operating temperature and duration, loads, impact, indoor or outdoor use, fluids, required life and any regulatory requirement. For flexible parts, include the target hardness and how the part deforms.
Use the datasheet as a starting point
Resin properties depend on cure and test conditions. Prototype test results must be interpreted against your actual application. Medical contact, food contact and flame classifications need specific evidence.
Need help selecting a casting resin?
Send the target production material and the properties that matter most.
From master pattern
to a repeatable part.
The quality of a cast part starts before the resin enters the mold. Surface preparation, mold layout and cure conditions all influence the result.
-
Review the model and acceptance criteria
Check geometry, quantity, resin needs, visible faces and critical interfaces. Agree the drawing revision and where parting lines or gate marks can be placed.
-
Make and finish the master
Produce a pattern by a suitable CNC or additive route. Remove unwanted build marks and prepare the required texture or gloss before molding.
-
Create the silicone mold
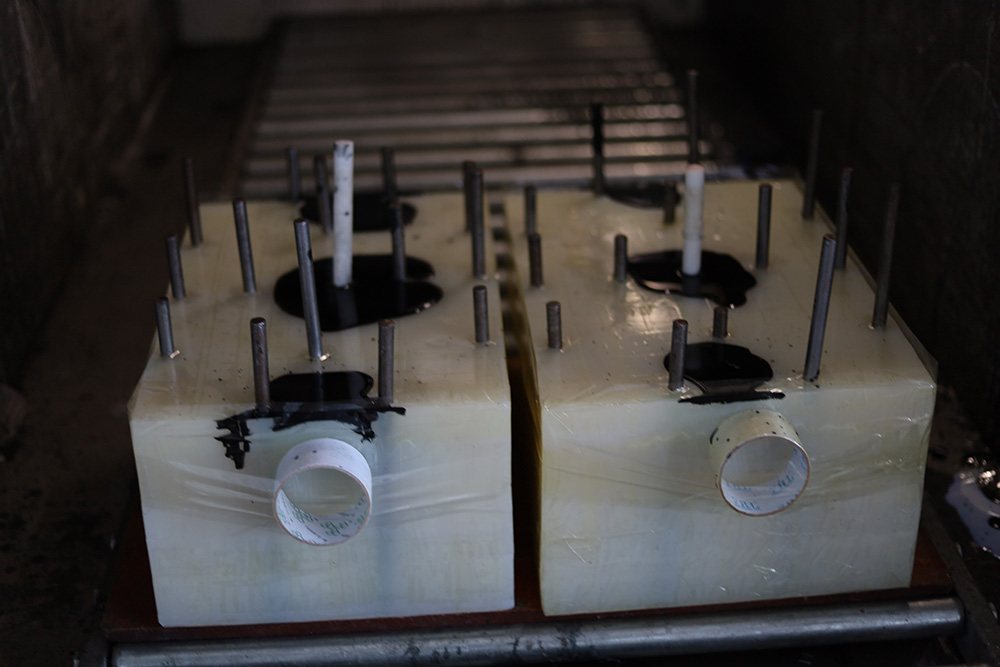
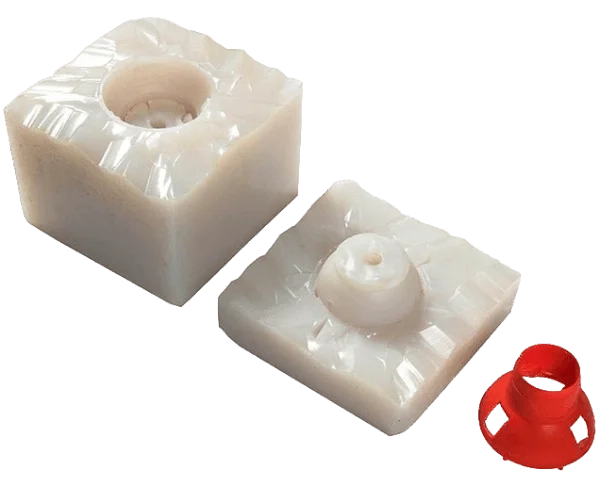
Cure silicone around the prepared pattern, open the mold and remove the master. Plan registration, gates and vents so resin can fill the cavity and the part can be released.
-
Mix, cast and cure
Process the selected resin using its specified mixing and cure conditions. Vacuum processing helps manage entrapped air; filling and cure controls remain important.
-
Trim, finish and inspect
Remove gates and flash, apply the agreed finish, then inspect the required dimensions and cosmetic surfaces before packing.
Define the specification
before the batch.
A useful quote confirms what will be made and how it will be accepted. A universal tolerance or fixed number of mold cycles cannot describe every resin and geometry.
- Quantity & tooling plan
- Provide the initial batch and expected repeat demand. Mold quantity, cavity layout and replacement tooling affect total cost.
- Part size & wall thickness
- Send the overall dimensions and CAD model. Large spans, thin details and thick masses need individual fill, cure and distortion review.
- Tolerances & shrinkage
- Mark critical dimensions, datums and fits. Pattern accuracy, silicone tooling, resin shrinkage and post-cure influence the final part; achievable tolerances are confirmed on review.
- Mold life & repeat orders
- Life depends on geometry, resin, demolding stress and surface requirements. Confirm the planned acceptable yield and any replacement-mold allowance.
- Lead time
- Allow for pattern preparation, molding, casting, cure, finishing and inspection. The quotation confirms production timing separately from transit.
- Delivery & documentation
- Specify destination, packaging, inspection reports, resin documentation and first-article approval requirements with the RFQ.
Appearance is part
of the specification.
Silicone can reproduce the master’s surface detail. Specify which faces matter and approve a finish reference so texture, color and gate cleanup are assessed consistently.
As-cast texture
A prepared master establishes the surface texture. Discuss parting lines, flash removal and acceptable witness marks on visible faces.
Pigmented resin & painted surfaces
Specify the color reference, gloss level and whether color is in the resin or applied as a coating. Agree a sample for appearance-critical parts.
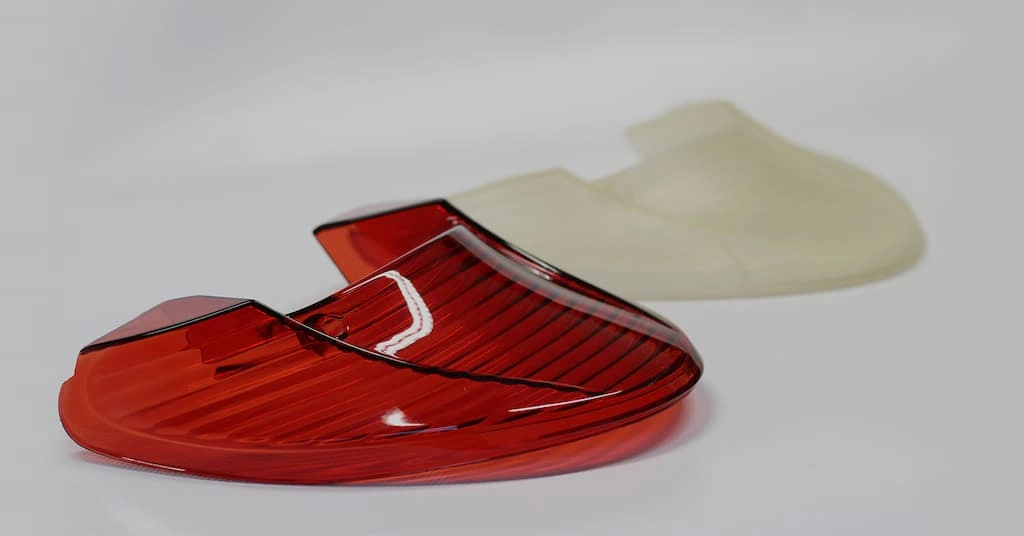
Clear or translucent appearance
Confirm the resin, surface preparation and polish. Visible clarity alone does not establish optical performance, UV stability or suitability as a regulated lamp component.
Metallic appearance & secondary work
Request coating, marking, inserts or assembly as part of the review. Confirm compatibility and masking instead of carrying metal-finishing specifications over to PU.
Quote the finished component.
Include color, texture, visible-face annotations and a reference sample where available.
Resolve the details
that change the outcome.
Use the drawing to identify what matters. These are review topics rather than universal design limits; the selected resin and actual geometry determine the practical solution.
Keep section changes controlled
Flag thin walls, heavy masses and abrupt thickness transitions. They influence filling, heat during cure, shrinkage and distortion.
Review undercuts and fragile details
Flexible molds can release some undercuts, but deep locks and delicate projections can tear the silicone or damage parts.
Identify the assembly interfaces
Call out mating faces, hole locations, threads, bosses and inserts. Discuss secondary machining where the required fit justifies it.
Choose gates and visible faces together
Deep pockets and enclosed features can trap air. Agree venting, mold splits and cleanup locations around the cosmetic requirements.
Keep the model revision, approved resin, cure, color reference and accepted sample linked. A geometry change may require a revised master and mold.
Trust starts with
clear acceptance criteria.
The published ISO 9001:2015 certificate names PROLEAN MFG (SHENZHEN) CO LTD and covers production of hardware accessories. Confirm the scope required for your project, alongside the inspection plan and delivery documents.
Material and revision control
Record the agreed resin grade, model revision and finish reference. Request supplier technical data and batch documentation where required and available.
Dimensions and functional interfaces
Specify datums and critical features. Choose measurement methods that suit the part; flexible geometry may need an agreed support and measurement condition.
Appearance and first-article approval
Agree color, texture, acceptable bubbles, parting-line marks and visible-face criteria. Request sample approval before completing the batch when needed.
Reports and protective packing
Define sampling, report format and traceability requirements with the order. Protect finished surfaces and distortion-sensitive parts during shipment.
Use the process that matches
the next decision.
Compare the complete route: tooling, parts, finishing, validation and repeat demand. The economic crossover depends on the design and material, not a universal order quantity.
| Decision factor | Vacuum casting | 3D printing | Plastic CNC machining | Injection molding |
|---|---|---|---|---|
| Tooling | Master and silicone mold | No dedicated mold | Machining setup and workholding | Production mold investment |
| Material basis | Cast PU selected for target properties | Process-specific polymers | Selected machinable stock grade | Specified molding-grade polymer |
| Useful project stage | Repeated prototypes and small batches | Early geometry changes and complex one-offs | Stock-material tests and critical features | Stable designs and repeat demand |
| Key tradeoff | Mold wear and resin equivalence | Finish, orientation and process properties | Tool access, stock removal and geometry | Tool cost, tooling changes and molding DFM |
What drives a vacuum casting quote?
Pattern complexity and finish, resin volume and grade, mold count, demolding difficulty, cure time, secondary work and inspection all contribute. Ask for price breaks by quantity and clarify whether replacement molds and finishing are included.
Parts for product development.
Requirements for the real application.
Equipment housings & electronics
Evaluate covers, control panels and enclosure assemblies. Specify mounting features, heat exposure and any electrical or flame requirements.
Automotive & mobility development
Review trim and appearance prototypes. Confirm temperature, UV and chemical exposure; production vehicle use requires the appropriate validation.
Medical equipment development
Explore equipment covers and nonclinical development models. Patient contact, sterilization and regulated use require a separate material and compliance review.
Industrial & consumer products
Compare grips, handles, protective covers and presentation samples. Define load, wear and contact requirements before selecting a resin.
Vacuum casting
questions, answered.
Practical answers for sourcing, design review and the next production decision.
What is the difference between vacuum casting and urethane casting?
For polyurethane prototype parts, the terms often describe the same route: resin is cast in a silicone mold using vacuum processing. Urethane casting describes the material family; vacuum casting describes the process. Vacuum forming of a heated plastic sheet and vacuum metal casting are different processes.
Are ABS-like and PP-like cast resins the same as ABS and PP?
No. These labels describe selected comparable properties. Cast PU is generally a thermoset, while ABS and PP are thermoplastics. Check the exact resin data and use the intended production material when material-specific validation is required.
How many parts can one silicone mold make?
There is no fixed acceptable yield for every mold. Resin chemistry, geometry, undercuts, release stress and finish criteria affect mold life. The tooling plan should identify expected yield, inspection criteria and replacement molds for your order.
What tolerance and shrinkage should I specify?
Identify critical dimensions and datums on the drawing rather than assuming one blanket tolerance. The pattern, mold, resin, cure and geometry all influence the finished result. Request achievable tolerances and any shrinkage compensation to be confirmed during engineering review.
Can vacuum casting produce clear or flexible parts?
Clear rigid and rubber-like PU resin families can be considered. For clear parts, specify haze, color, polish and exposure conditions. For flexible parts, specify hardness, deformation and service environment. Exact grade and suitability require confirmation.
How much does vacuum casting cost, and how long does it take?
Cost and schedule depend on the master, resin, mold count, batch quantity, cure, finishing and inspection. Include your required date and destination in the RFQ. The quotation confirms tooling, part costs and production lead time; delivery transit is assessed separately.
When should I choose injection molding instead?
Consider injection molding for a stable design with repeat demand, or when validation requires the specified injection-molded material and process. Compare tooling, lifetime quantity and change risk with vacuum casting before deciding.
What files and documents are needed for a quote?
Send a 3D model, a dimensioned drawing for critical features, quantity, intended use, material requirements and finish references. Include inspection documents, first-article approval, delivery destination and target date. An NDA is optional and can be arranged for the project.
START WITH YOUR REQUIREMENTS
Make the next batch
the right batch.
Send your design and explain what the parts need to do. The engineering review can then address resin choice, tooling, finish and inspection together.
Confidential enquiries. Optional NDA ↗
For a more complete quotation
- 3D CAD model and drawing revision
- Critical dimensions, mating parts and visible faces
- Quantity now and expected repeat demand
- Target resin properties and service conditions
- Color, texture and finish reference
- Inspection documents, destination and required date
Need a preliminary process review? Include your target production material and the tests you plan to run.