CUSTOM ZINC ALLOY PARTS
Zinc Die Casting
Services
Complex details. Consistent parts.
A clear path to production.
Bring your housings, hardware and precision components to ProleanTech for zinc die casting, with tooling, CNC post-machining and surface finishing reviewed as one manufacturing plan.
Share CAD + a dimensioned drawing. Optional NDA available →
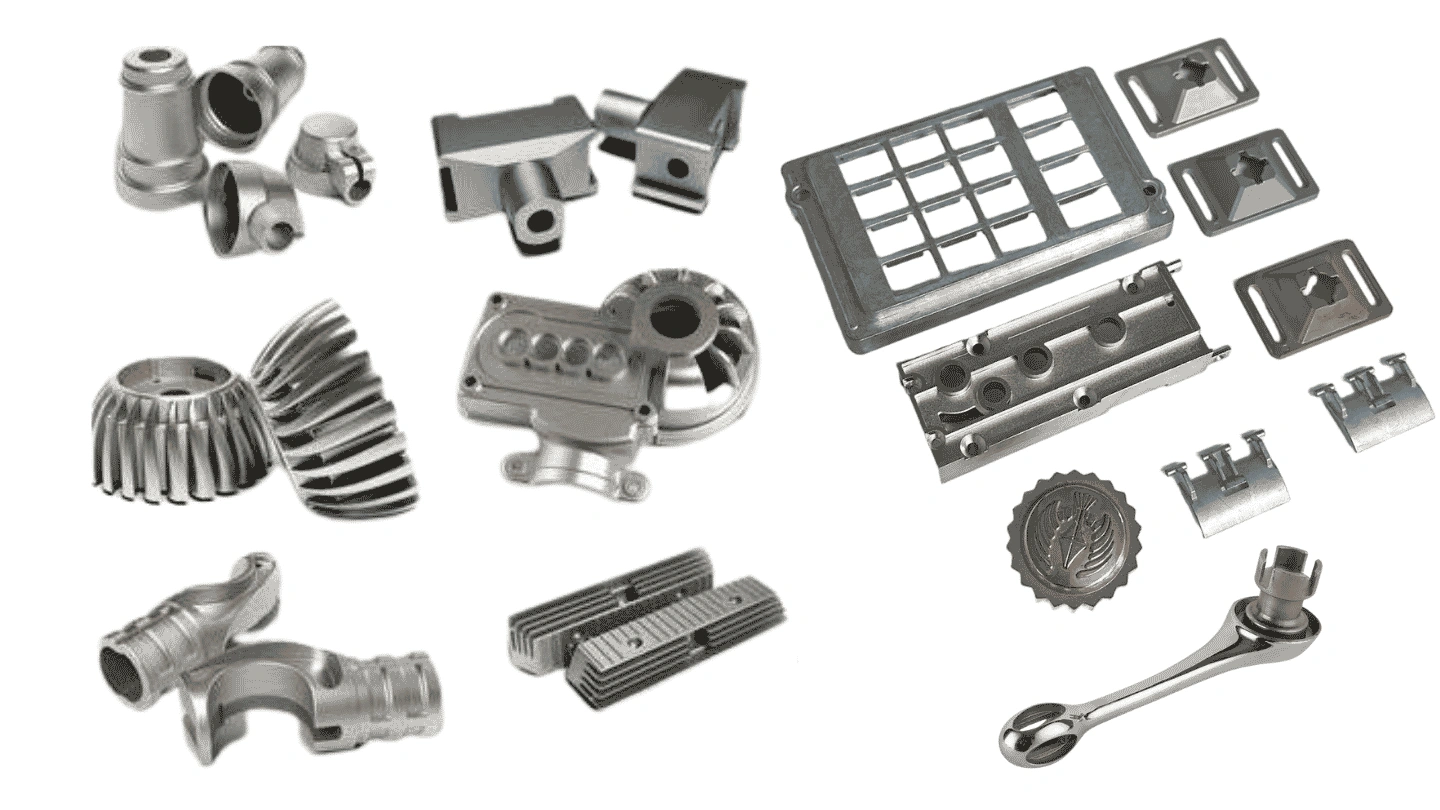
Tooling to finished partDFM, casting and secondary operations
Alloy selected for the applicationZamak and zinc-aluminum alloy review
Drawing-led acceptanceCritical features and first-sample approval
Is zinc die casting right for your part?
Zinc die casting injects molten zinc alloy into a reusable steel die. It is a strong candidate for detailed metal components made repeatedly, when the expected demand justifies dedicated tooling.
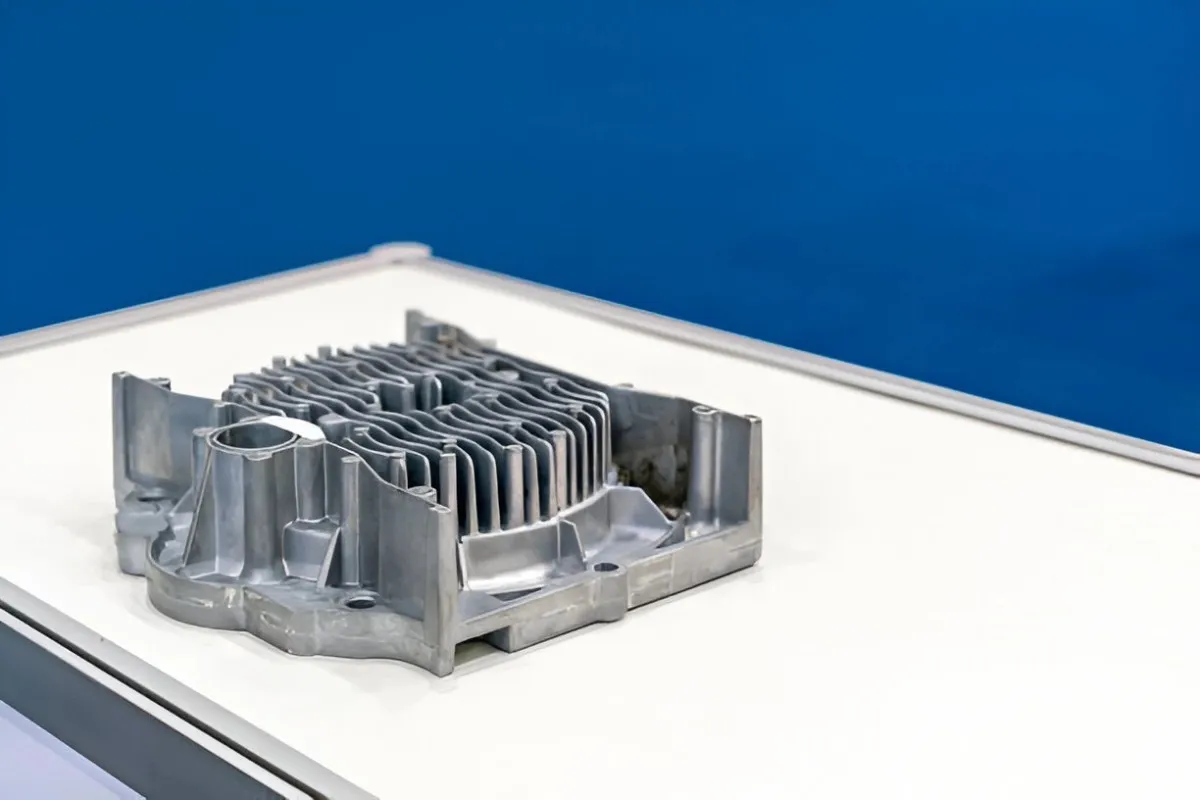
Housings & enclosures
Integrate mounting points, ribs and other features into one casting. Identify mating faces and any sealing requirements before tooling.
Hardware & decorative components
Consider zinc for handles, fittings and visible parts that need detailed geometry and a defined plated or painted finish.
Mechanical & assembly parts
Review brackets, connectors and small mechanisms against load, wear and fit requirements. Machine critical interfaces where needed.
Compare tooling plus piece price over the expected production program. A low-volume prototype or a design still changing may suit another manufacturing route.
Have a zinc part in mind?
Send your CAD, drawing and expected quantity to review the manufacturing route.
Select the zinc alloy before finalizing the tool.
The right grade balances strength, dimensional behavior, finishing and service conditions. Specify the alloy and material standard, or send your application requirements for review.
| Alloy candidate | Why consider it | Key selection check |
|---|---|---|
| Zamak 3 | Balanced castability, dimensional stability and finishing behavior. | A general-purpose starting point for many zinc parts. |
| Zamak 5 | Greater strength and hardness than Zamak 3. | Lower ductility matters if the part will be bent, riveted or crimped. |
| Zamak 2 | High strength and hardness among conventional Zamak alloys. | Account for dimensional and property changes with aging. |
| ZA-8 | A higher-aluminum zinc alloy with useful strength and creep performance. | Confirm the casting route and grade availability for the project. |
Selection guidance: International Zinc Association ↗. Grade availability and project suitability are confirmed with the quotation.
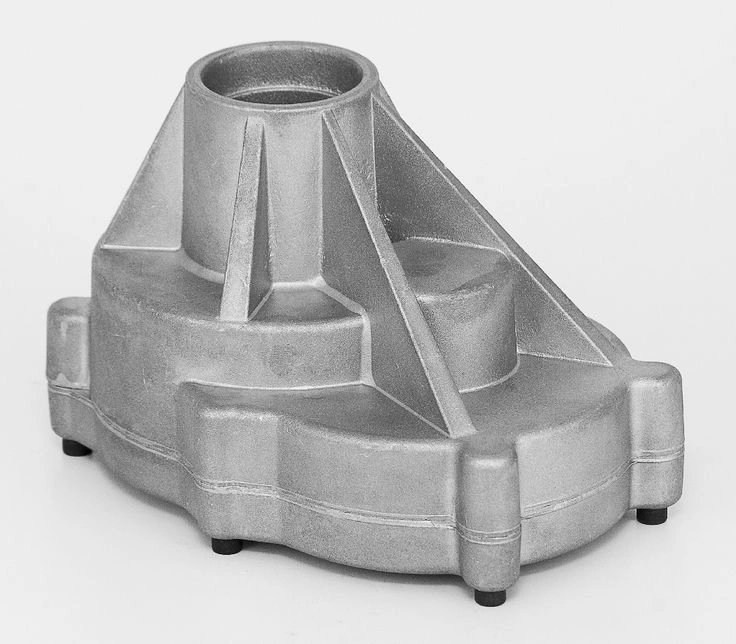
Zinc or aluminum die casting?
Zinc supports detailed geometry and multiple finish options, but it is denser than aluminum. If weight is a primary constraint, compare an aluminum route.
For either material, evaluate service temperature, sustained load, corrosion exposure and total manufacturing cost. Room-temperature strength alone does not determine suitability.
Need help selecting a zinc alloy?
Share the loads, service temperature and finish requirements with your quote request.
Design the casting and the finished part together.
The most useful DFM review connects what the die can form with what the final assembly needs. Resolve these details before committing to steel.
01 / Walls, ribs & transitions
Aim for consistent wall sections and smooth transitions. Review filling and shrinkage risk around local thick areas; minimum wall thickness depends on the complete geometry.
02 / Parting, draft & ejection
Agree the pull direction, parting line and any side actions. Mark visible faces and areas where gate or ejector marks are unacceptable.
03 / Datums, fits & threads
Separate as-cast dimensions from machined features. Identify the functional datums, thread specification and critical-to-quality dimensions.
04 / Porosity, sealing & appearance
Flag pressure-containing parts, sealing faces and cosmetic zones at quotation. Define leak tests or visual acceptance criteria where required.
Secondary operations turn the casting into an assembly-ready part.
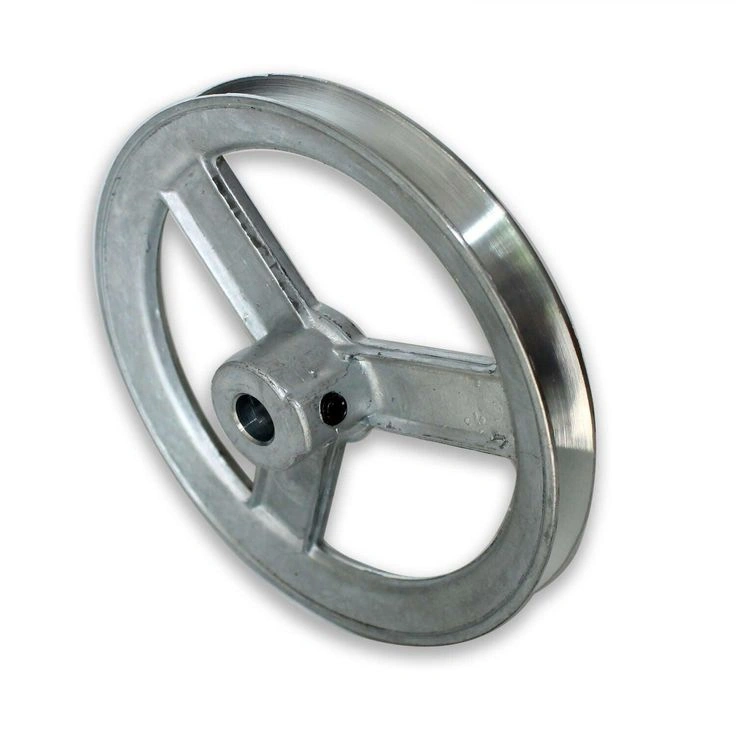
Trimming and deburring address gates, flash and edge condition. CNC machining and tapping can produce critical holes, threads, mating faces and sealing features.
For plating, painting or powder coating, specify the coating system, thickness, color or gloss, exposure and test requirements. Agree masking so coating buildup does not compromise fits.
Ready for a design review?
Send your drawing with critical fits, cosmetic faces and finish requirements marked.
Agree acceptance. Approve samples. Release production.
A clear approval sequence keeps tooling decisions, inspection and delivery tied to the same drawing revision.
Define quality in measurable terms.
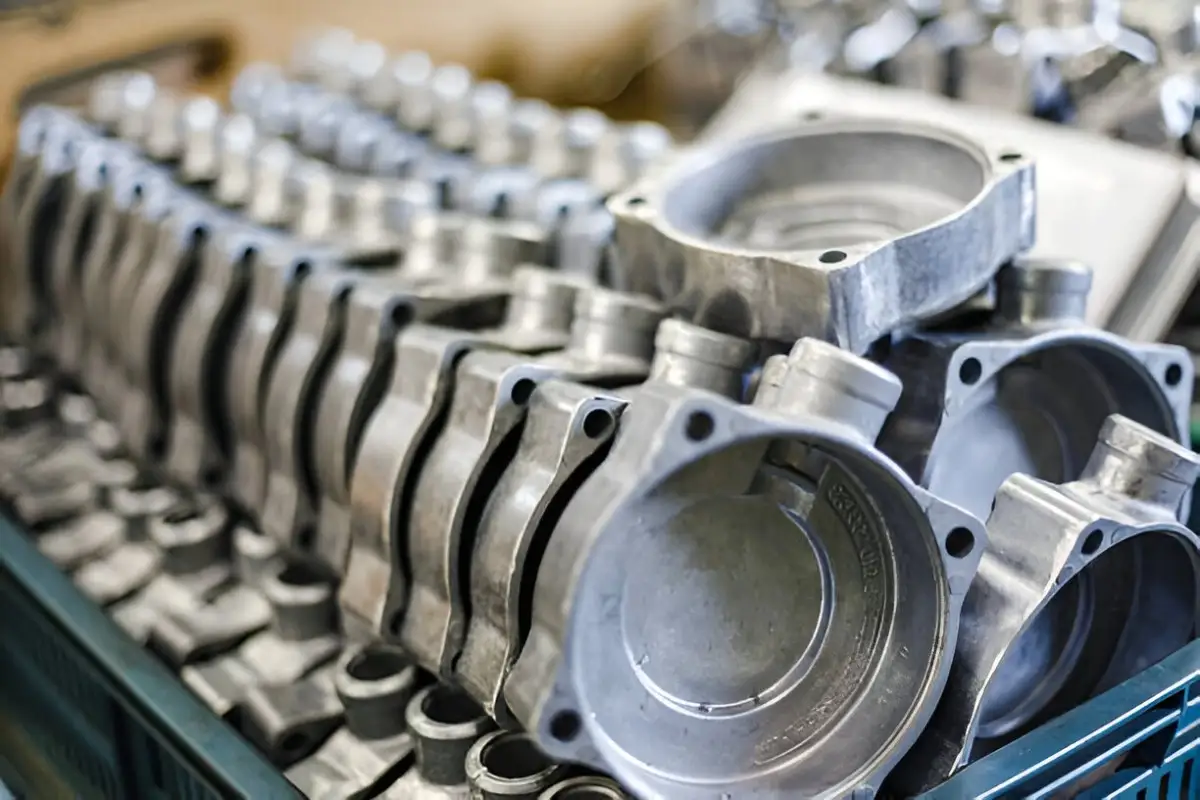
Identify dimensions that affect fit and function, visible surfaces that need cosmetic approval, and documentation required at delivery.
Agree sampling, traceability and any material, coating or leak-test requirements before quotation. Casting tolerances and secondary-machining tolerances should be specified separately.
- 01 / REVIEW
Scope the project
Confirm CAD and drawing, alloy, quantities, finish and critical requirements. Resolve DFM actions and agree tooling scope.
- 02 / SAMPLE
Validate first parts
Review samples against the agreed dimensional, functional and appearance criteria. Approve or resolve changes before production release.
- 03 / PRODUCE
Control the repeat order
Manufacture to the approved revision with the agreed inspection plan, packaging and delivery requirements.
What affects cost and lead time?
Tool complexity, cavity count, alloy, order volume, secondary machining, finish and inspection all matter. Ask for tooling, sample and production timing separately, including any sample iteration allowance.
Zinc die casting service FAQs.
Which zinc die casting alloy should I choose?
Zamak 3 is a common general-purpose candidate. Zamak 5 offers greater strength and hardness with reduced ductility; Zamak 2 and ZA-8 suit selected performance needs. Send the loads, service temperature, finish and assembly requirements so the grade can be reviewed for your part.
Is zinc die casting economical for small orders?
Dedicated tooling can dominate the cost of a small order. Compare total tooling and production cost over the expected program. For early prototypes or a design that is not yet stable, machining or another prototype route may be a better starting point.
What tolerances can you achieve?
Tolerance depends on feature size, geometry, the parting line and tool design. Supply a dimensioned drawing with datums and critical features. The quotation should distinguish as-cast requirements from tighter features needing secondary machining.
Can zinc die cast parts be machined, plated or painted?
Yes. Machining or tapping can create critical interfaces; suitable coating systems can provide appearance or surface protection. Confirm the alloy, preparation, coating thickness, masking and acceptance tests before production.
Can zinc die castings be used for load-bearing or sealing applications?
These uses require application-specific review. For sustained loads, consider creep and service temperature. For sealing, define allowable porosity, sealing faces and leak-test requirements rather than assuming every casting is leak-tight.
What files and quantities are needed for a quote?
Send 3D CAD and a dimensioned PDF, the alloy or application requirements, order and annual quantities, finish, critical dimensions and target date. Include required reports and details of any existing tooling.
START WITH YOUR DRAWING
Let’s review your
next zinc part.
Share the geometry, quantity and requirements that matter. We can then review the alloy, tooling route and secondary operations for quotation.
Optional NDA available · Your files stay confidential.
For a more complete quote
- 3D CAD + dimensioned PDF
- Alloy or application requirements
- Order quantity + annual demand
- Finish, fits + critical dimensions
- Inspection documents + target date