Materials · Polyethylene (PE)
Polyethylene (PE) CNC Machining Service
Machined and molded UHMW-PE and HDPE — the 2 grades published here, with the tolerance, minimum wall and lead time the shop holds.
Specifications
Polyethylene specifications: ±0.125 mm tolerance, 0.80 mm wall, 3 to 10 days lead time
Six numbers a buyer asks for before sending a drawing — the process, the
tolerance we hold, the minimum wall, the largest envelope, the lead time and the price band.
identical on all 23 material pages — they describe the shop, not the material. Tolerance,
minimum wall and price band are the three that change from one material to the next.
Machining routes
Machining routes for polyethylene: milling, turning, cutting and molding
Milling and turning are what this page is quoted on. The routes below are the ones the same material takes when the stock form, the volume or the lead time changes — each one is a service page on this site.
Published grades
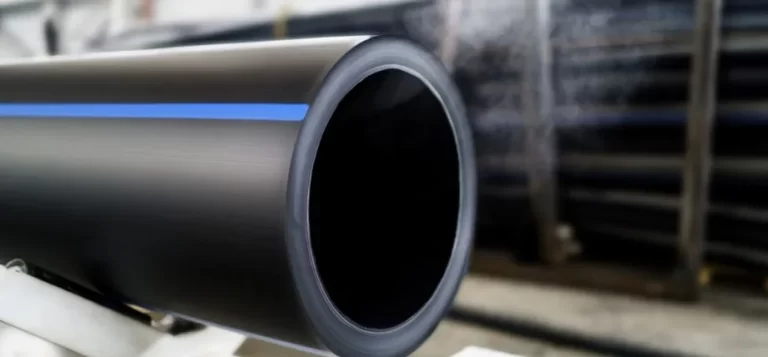
The two polyethylene grades: UHMW-PE and HDPE
The two grades published for polyethylene, the polymer family each one belongs to, and the applications each is normally specified for.
Grades · the two published for polyethylene
| Grade published | Polymer family | Applications named on this page |
|---|---|---|
| UHMW-PE | Ultra-high-molecular-weight polyethylene | Food processing, packaging and conveying surfaces |
| HDPE | High-density polyethylene | Cables, pipes and fittings, agricultural products |
weight is what separates them — UHMW-PE is bought for sliding wear and impact, HDPE for
stiffness and pressure service. A drawing that says only "PE" leaves that choice open,
so name the grade or the property you need and it is confirmed in writing before the
first cut.
hardness move with the grade and the melt index, so a single figure per row would
mislead. Ask for the datasheet, or state the property on the drawing.
Which polymer?
UHMW-PE, HDPE or polypropylene: choosing by wear, pressure and moisture
Each answer points at a page on this site that covers it in more depth — a
comparison, a grade guide or a process page.
Machining & tolerance
Tolerancing and inspecting polyethylene parts to ISO 2768
The published tolerance on this page is Not lower than ±0.125mm (±0.005″)
on the drawing, to ISO 2768. Where a feature needs better than that, say so on the
drawing — that conversation belongs before the tool goes in, not after.
Finishes
Finishing a polyethylene part: polishing, blasting and deburring
This is the polymer set of finishes: polishing, blasting, sanding and fine machining. The metal pages list the plating and heat-treatment routes instead.
Applications
Where UHMW-PE and HDPE parts go: food, pharma and pipework
- Food processingParts and surfaces in food-handling equipment
- PharmaceuticalsComponents for pharmaceutical process equipment
- PackagingPackaging machinery parts and wear surfaces
- Cables, pipes & fittingsCable components and pipework fittings
All of it cut on the same floor —
see CNC machining and
how we hold tolerance.

Further reading
Polyethylene in context: the HDPE guide, machinability and tolerances
Deeper reading from around this site — the comparisons, the standards and the
process notes behind this material.
FAQ
Polyethylene machining: two grades, tolerance, lead time and files
Straight answers to the questions that come up most often on a CNC quote —
with the figures published for this material, and a link for each point.
Which polyethylene grades can you machine?
What tolerance can you hold?
What is the smallest wall and the largest part?
How fast is a polyethylene part?
Which finish should I ask for?
What files should I send?
Is my drawing kept confidential?
Next step
Send the drawing — we come back with the material call and the price
Upload the model and the 2D PDF. You get a manufacturability note, a note on the resin if the drawing leaves it open, and a price.
All uploads are secure and confidential.
- Quoted in 1 business day on a clean drawing
- The resin and fill stated in writing on the quote
- First article inspected before the run