? What do you need marked?
SURFACE FINISHING
Laser Engraving Service
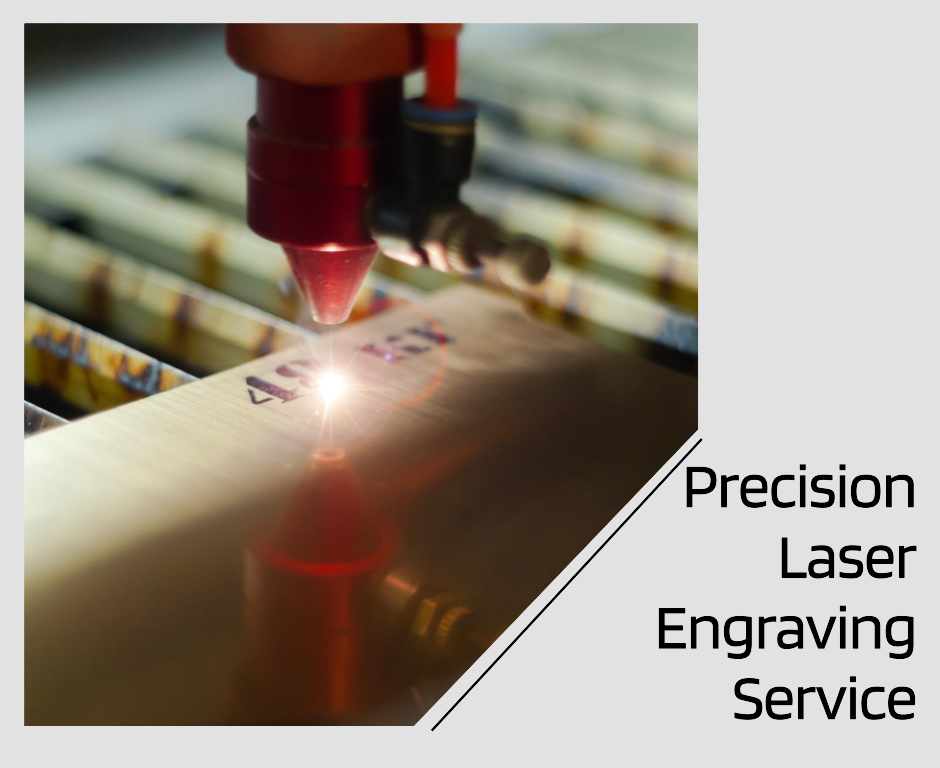
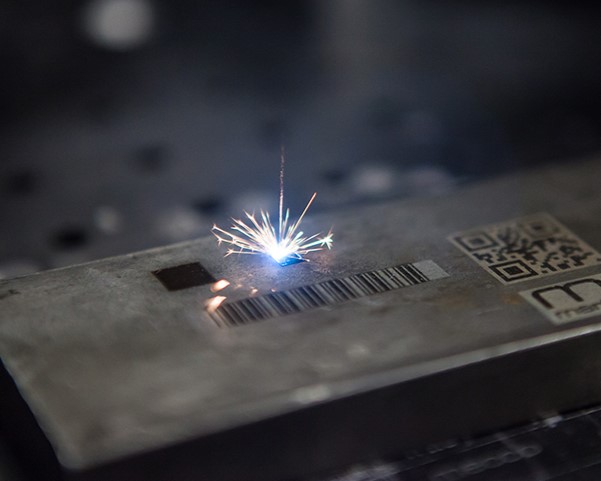
A subtractive process that uses a focused laser beam to cut a permanent mark into a surface — graphics, text, serial numbers, barcodes and QR codes. Unlike a coating, it removes material instead of adding it, so the dimensional effect is far smaller than any plated or painted layer.
Sequence
Marking is last — but which last depends on the coating
If the part is coated as well as marked, the order of the two operations decides what the mark looks like. Get it wrong and the mark is either buried or burnt away.
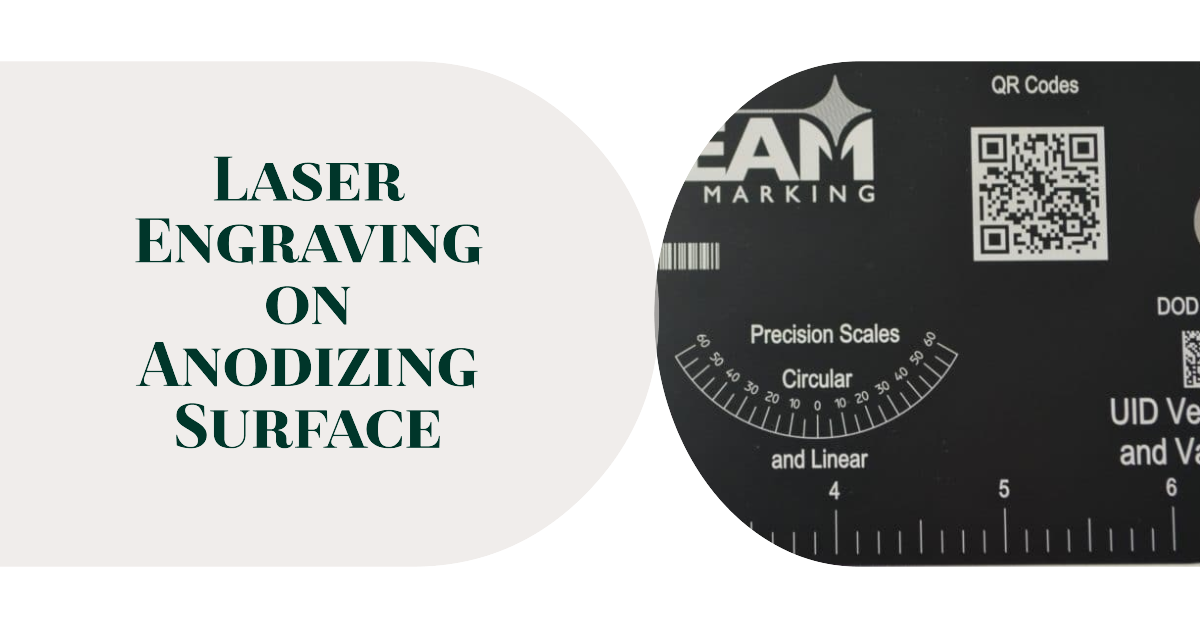
The order matters more than it looks. Engraving after anodizing cuts through the anodized layer and reveals the metal colour underneath — that is how you get a high-contrast mark on anodised aluminium. Engrave first and the anodizing buries it. See materials and mark colour.
Fit check
Can we mark your part? Three things decide it
Substrate, mark area and geometry. The third one is the one that catches people out.
Substrate and mark colour
- Metal — black or dark marks
- Acrylic — frosty white finish; wood and leather — darker
- Glass — frosted appearance; anodised aluminium — mark cuts through to the metal colour below
The colour of the mark is set by the substrate, not by an ink you choose. See the full table.
Size and mark area
- Marking tolerance is ±0.13 mm — position it against a datum, not a free edge
- Kerf is 0–0.2 mm, so the mark is a shallow cut rather than a deep feature
- Maximum part size for the marking bed: To confirm
Give us the dimension from a datum to the mark, not just the text to be marked.
Geometry
- Flat faces mark most predictably — curved and cylindrical surfaces need focus correction
- Deep recesses may be out of the laser's focal range
- Matte and dark substrates give lower contrast than polished metal
Tell us the surface orientation of the mark area — see design constraints.
Specifications
Laser engraving: ±0.13 mm positioning across a 0 – 0.2 mm kerf
These figures come from our published service description for this process.
Mark depth
What engraving takes off — and why it matters where that mark sits
Engraving is subtractive. It removes a shallow layer, which is an order of magnitude less than any coating process adds.
| Comparison | Dimension change | Where that is acceptable | Where it is not |
|---|---|---|---|
| Laser engraving | 0 – 0.2 mm removed | Any surface where a shallow mark is wanted — flat, non-functional faces. | Sealing faces, bearing surfaces, and anywhere a crack could initiate. |
| Laser engraving | ±0.13 mm positioning | Features located from a datum you specify. | Marks positioned from a raw edge or from a feature that moves between parts. |
| For contrast — a coating | Adds material | Shown for scale: plating adds roughly what engraving removes, in the opposite direction. | — |
Kerf and tolerance as published. Engraving removes up to 0.2 mm; a plated or painted layer adds its thickness instead. The two are not interchangeable on a critical fit.
Mark sitting on a sealing face or a bearing surface? Tell us and we will move it — or mark a different face.
Get a quoteCO2 or fiber
Which laser suits your substrate
We run both CO2 and fiber technology. The substrate and the mark you want decide which one is used.
Fiber laser
The route for marking metals and anodised aluminium. Produces the black or dark marks listed for metal substrates, and cuts through an anodized layer to expose the metal colour beneath.
Best for: steel, stainless, anodized aluminium, metal serial numbers
Not for: organic substrates like wood, leather and most clear acrylics.
CO2 laser
The route for acrylic, wood, leather, glass and coated surfaces. Produces the frosty white mark on acrylic and the frosted appearance on glass.
Best for: acrylic, wood, leather, glass, painted surfaces
Not for: bare metal — a CO2 beam is reflected rather than absorbed.
Not sure which laser your substrate needs? Tell us the material and what the mark has to do — traceable serial, logo, or high-contrast text.
Get a quotePick or avoid
When laser engraving is the right call — and when it is not
Pick laser engraving when
- The mark has to be permanent — serial numbers, lot codes, QR or barcodes for traceability.
- The part is metal, acrylic, wood, leather, glass or anodised aluminium.
- The mark has to survive handling, cleaning and the part's own service life.
- You need high-contrast marking on anodised aluminium — engraving exposes the metal colour underneath.
- You want a mark that does not add a layer or a label that could fall off.
Avoid laser engraving when
- The mark sits on a sealing face, bearing surface or fatigue-critical area — engraving removes material and creates a stress riser.
- You need a coloured mark — the colour is set by the substrate, not by the process.
- The substrate is a material that will not mark consistently — see materials.
- The surface is highly polished and any mark would be unacceptable aesthetically — see polishing first.
Need a mark plus a colour finish? Send the drawing and we will sequence the two operations so neither ruins the other.
Get a quoteDesign constraints
Where the mark should and should not go
Three variables: where you put the mark, which surface it sits on, and the order against any coating.
Mark location
Position the mark against a datum, not freehand on a face. The tolerance is ±0.13 mm from whatever reference you give us — and a raw edge is a poor reference.
No-go surfaces
Do not put a mark on a sealing face, a bearing surface, an o-ring groove or a fatigue-critical section. Engraving removes material and creates a stress riser.
Surface orientation
Flat faces mark most predictably. Curved and cylindrical surfaces need focus correction, and deep recesses may fall outside the focal range.
Order against coating
Engrave after anodizing to cut through to the metal colour beneath. Engraving before anodizing buries the mark under the new oxide layer.
Contrast
Mark colour is set by the substrate: black on metal, frosted on glass, darker on wood and leather, frosty white on acrylic. Matte and dark substrates give lower contrast.
Data format
Send the mark as vector art or a font file, plus the exact text and any serial-number format. A screenshot cannot be reproduced accurately.
Drawing notes
What to write on the drawing so the mark lands in the right place
The location and the data format are the two things that decide whether the mark comes back right.
1. LASER ENGRAVE THE FOLLOWING: - PART NUMBER: ____________ - SERIAL NUMBER: ____________ (FORMAT: ____________) - QR / DATAMATRIX: SEE ATTACHED FILE2. MARK POSITION: ____________ mm FROM DATUM ____ (SEE VIEW A. FLAT FACE REQUIRED.)3. MARK TO BE LEGIBLE AFTER FINISHING OPERATIONS. ENGRAVE AFTER ANODIZING / PLATING. (delete if not applicable)4. DO NOT MARK SEALING FACES, BEARING SURFACES OR O-RING GROOVES.5. TEXT HEIGHT: ____ mm. FONT: ____________ SUPPLY VECTOR FILE FOR LOGOS.
Examples only. A mark without a datum and a text height cannot be reproduced to +/-0.13 mm — those two lines are the ones that matter.
Materials
What mark you get, by substrate
The colour of the mark is set by the material and the laser, not by an ink. This table is the published result for each substrate.
| Substrate | Mark result | Laser | Notes |
|---|---|---|---|
| Metal | Black or dark marks | Fiber | Typical for serial numbers, part numbers and QR codes. |
| Anodized aluminium | Mark exposes the metal colour beneath | Fiber | Engraving removes the anodized layer. This is how high-contrast marks are made on anodised parts — so engrave after anodizing. |
| Acrylic | Frosty white finish | CO2 | A bright, high-contrast mark on clear and coloured acrylic. |
| Glass | Frosted appearance | CO2 | Frosted, permanent mark without ink or labels. |
| Wood | Darker | CO2 | The mark darkens with the burn — contrast depends on the species and grain. |
| Leather | Darker | CO2 | Common for personalisation and branding. |
| Not listed | Ask first | — | Some coatings and plastics blister or discolour. Send a sample and we will test it. |
Marking a material that is not on this list? Send a sample part and we will run a test mark before quoting the batch.
Get a quoteApplications
Where laser engraving is used
The common thread is a mark that has to still be there years later, on a part that gets handled.
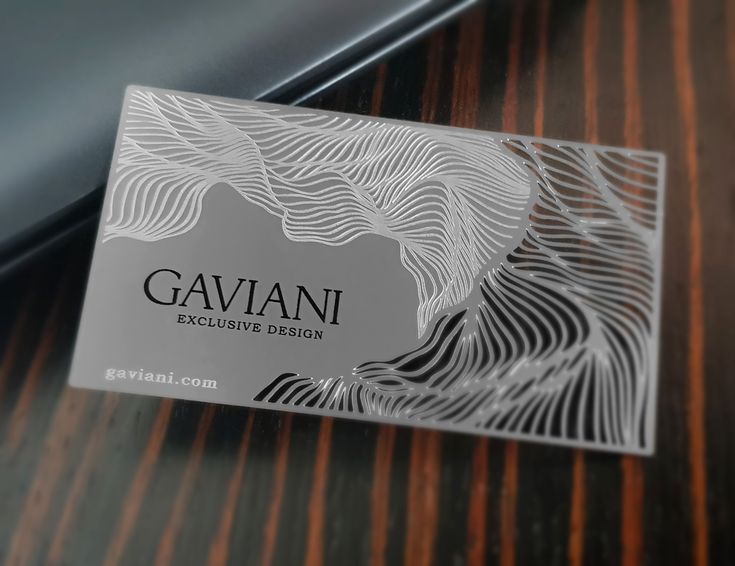
Branding and identification
Logos, ratings and certification marks cut into the part, where a printed label would be rubbed off or counterfeited.
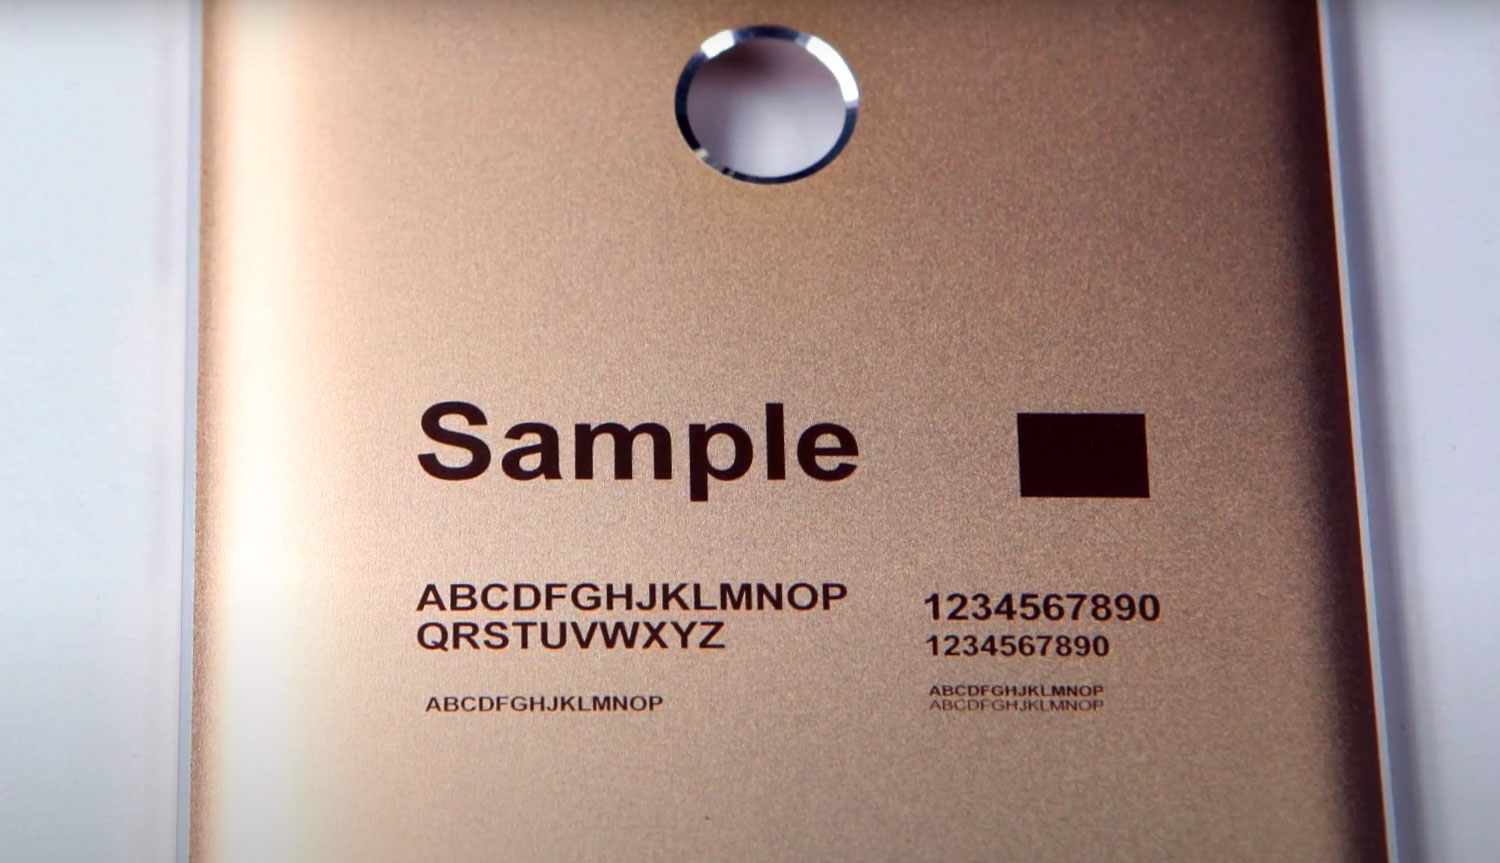
QR and datamatrix codes
Machine-readable codes for tracking and traceability, engraved after anodizing so they stay legible.
QA and documentation
What you get back with the parts
Purchasing usually needs paper as well as parts. Here is what we can issue today and what is still being confirmed.
Legibility and position
Mark checked for legibility and position against the specified datum.
Kerf and tolerance
Cut depth within 0–0.2 mm and position within ±0.13 mm of the datum.
First-article sample
A marked sample part for approval before the batch runs.
Serial number record
A log of the serial numbers marked per batch.
Further reading
Laser marking guides and comparisons
Longer answers on the questions this page only has room to state.
How marking differs from engraving and etching, and where each is used.
Depth, contrast and durability — the three things that separate the two.
Marking metals specifically: contrast, depth and what to specify.
Why stainless marks differently from carbon steel, and what to expect.
The coating that laser marking is usually paired with on aluminium parts.
Compare all 20 finishes by roughness, thickness, corrosion and cost.
FAQ
Laser engraving FAQ: the questions engineers ask us
Does engraving change my part dimensions?
When should I engrave relative to anodizing?
Can I get a coloured mark?
Which materials can you mark?
Can you mark a curved or cylindrical surface?
Is the mark permanent?
Can you mark a serial number that changes per part?
Should I put a part number on a sealing face?
Get your laser engraving quote
Upload the drawing with the mark content, the datum dimension and a vector file for any logo or code. Tell us the substrate so we can pick the laser.
What to send us
- Drawing — 2D and 3D files, with the mark position dimensioned from a datum.
- Mark content — exact text, part number, serial format, or the logo as a vector file.
- Substrate — the material, so we can choose CO2 or fiber.
- Text height and font — a mark without a height cannot be reproduced to ±0.13 mm.
- Quantity — number of units, and whether the serial numbers change per part.
- Coating order — if the part is also anodized, plated or painted, tell us the sequence.
All uploads are secure and confidential. Engineers review and reply with a quotation and lead time.