SPECIALTY MACHINING
Wire EDM
Services
Custom wire EDM machining for tooling, precision through profiles and narrow slots in conductive metals, from prototypes to repeat production.
Get a Quote Explore capabilities ↓
Your files stay confidential. Optional NDA available →
Precision wire cutting.
Requirements defined by your part.
Wire electrical discharge machining uses a continuously fed wire electrode and controlled sparks to remove conductive material. It suits profiles that are difficult to mill, particularly in hardened metals. The wire must pass through the workpiece; blind pockets require another process.
| Feature / requirement | What to consider |
|---|---|
| External and internal contours | Dies, punches, inserts, slots and precision profile components. Closed internal contours need a start hole and a threading path. |
| Straight and tapered cuts | Define top and bottom profiles, taper angle and datum references. Taper feasibility depends on thickness, geometry and machine travel. |
| Tolerance and surface finish | Identify critical dimensions and specify Ra where functional. Achievable results depend on material, thickness, flushing and rough/skim passes; confirmation is part of quotation. |
| Part envelope and volume | Send overall dimensions, cut thickness, quantity and annual demand. Maximum size, wire diameter and delivery date require project-specific confirmation. |
Custom wire-cut parts
for tooling and assemblies.
Is your part a fit?
Conductive material
Through profile or accessible entry
Defined material condition
Measurable acceptance criteria
Share your drawing to confirm the route.
Tooling and die components
Matching punch and die profiles, hardened inserts and wear components. State required clearances, heat treatment condition and mating features.
Precision mechanical parts
Through slots, intricate outlines and narrow features in conductive stock. Minimal mechanical cutting force helps with delicate geometries, while fixturing and slug retention still matter.
Prototype and replacement parts
Supply a controlled drawing revision and the functional datums. For repeat orders, identify the approved sample, inspection requirements and material condition.
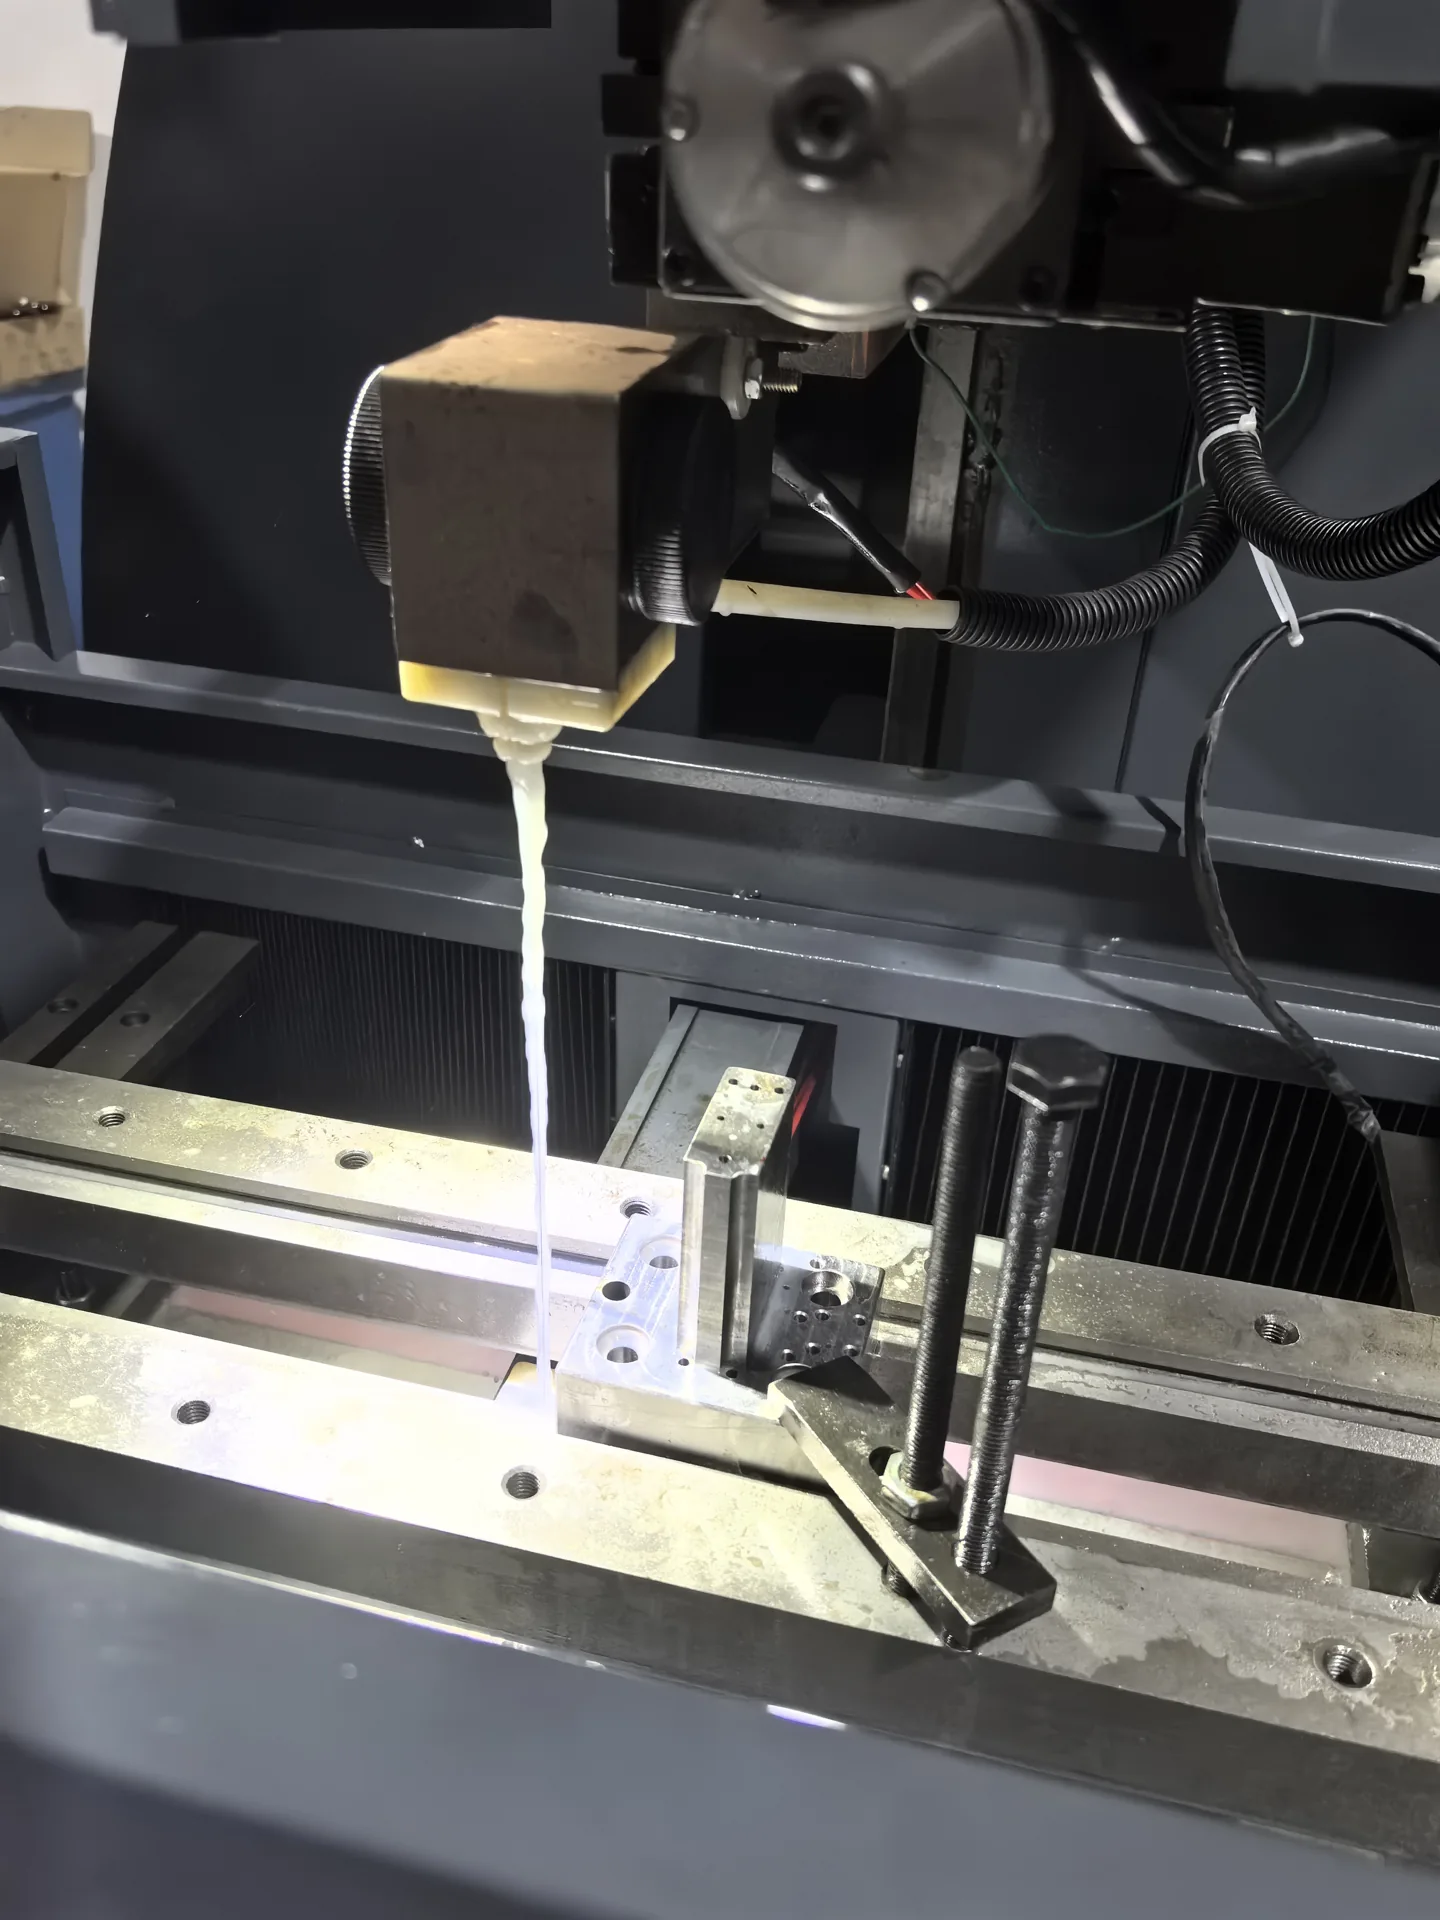
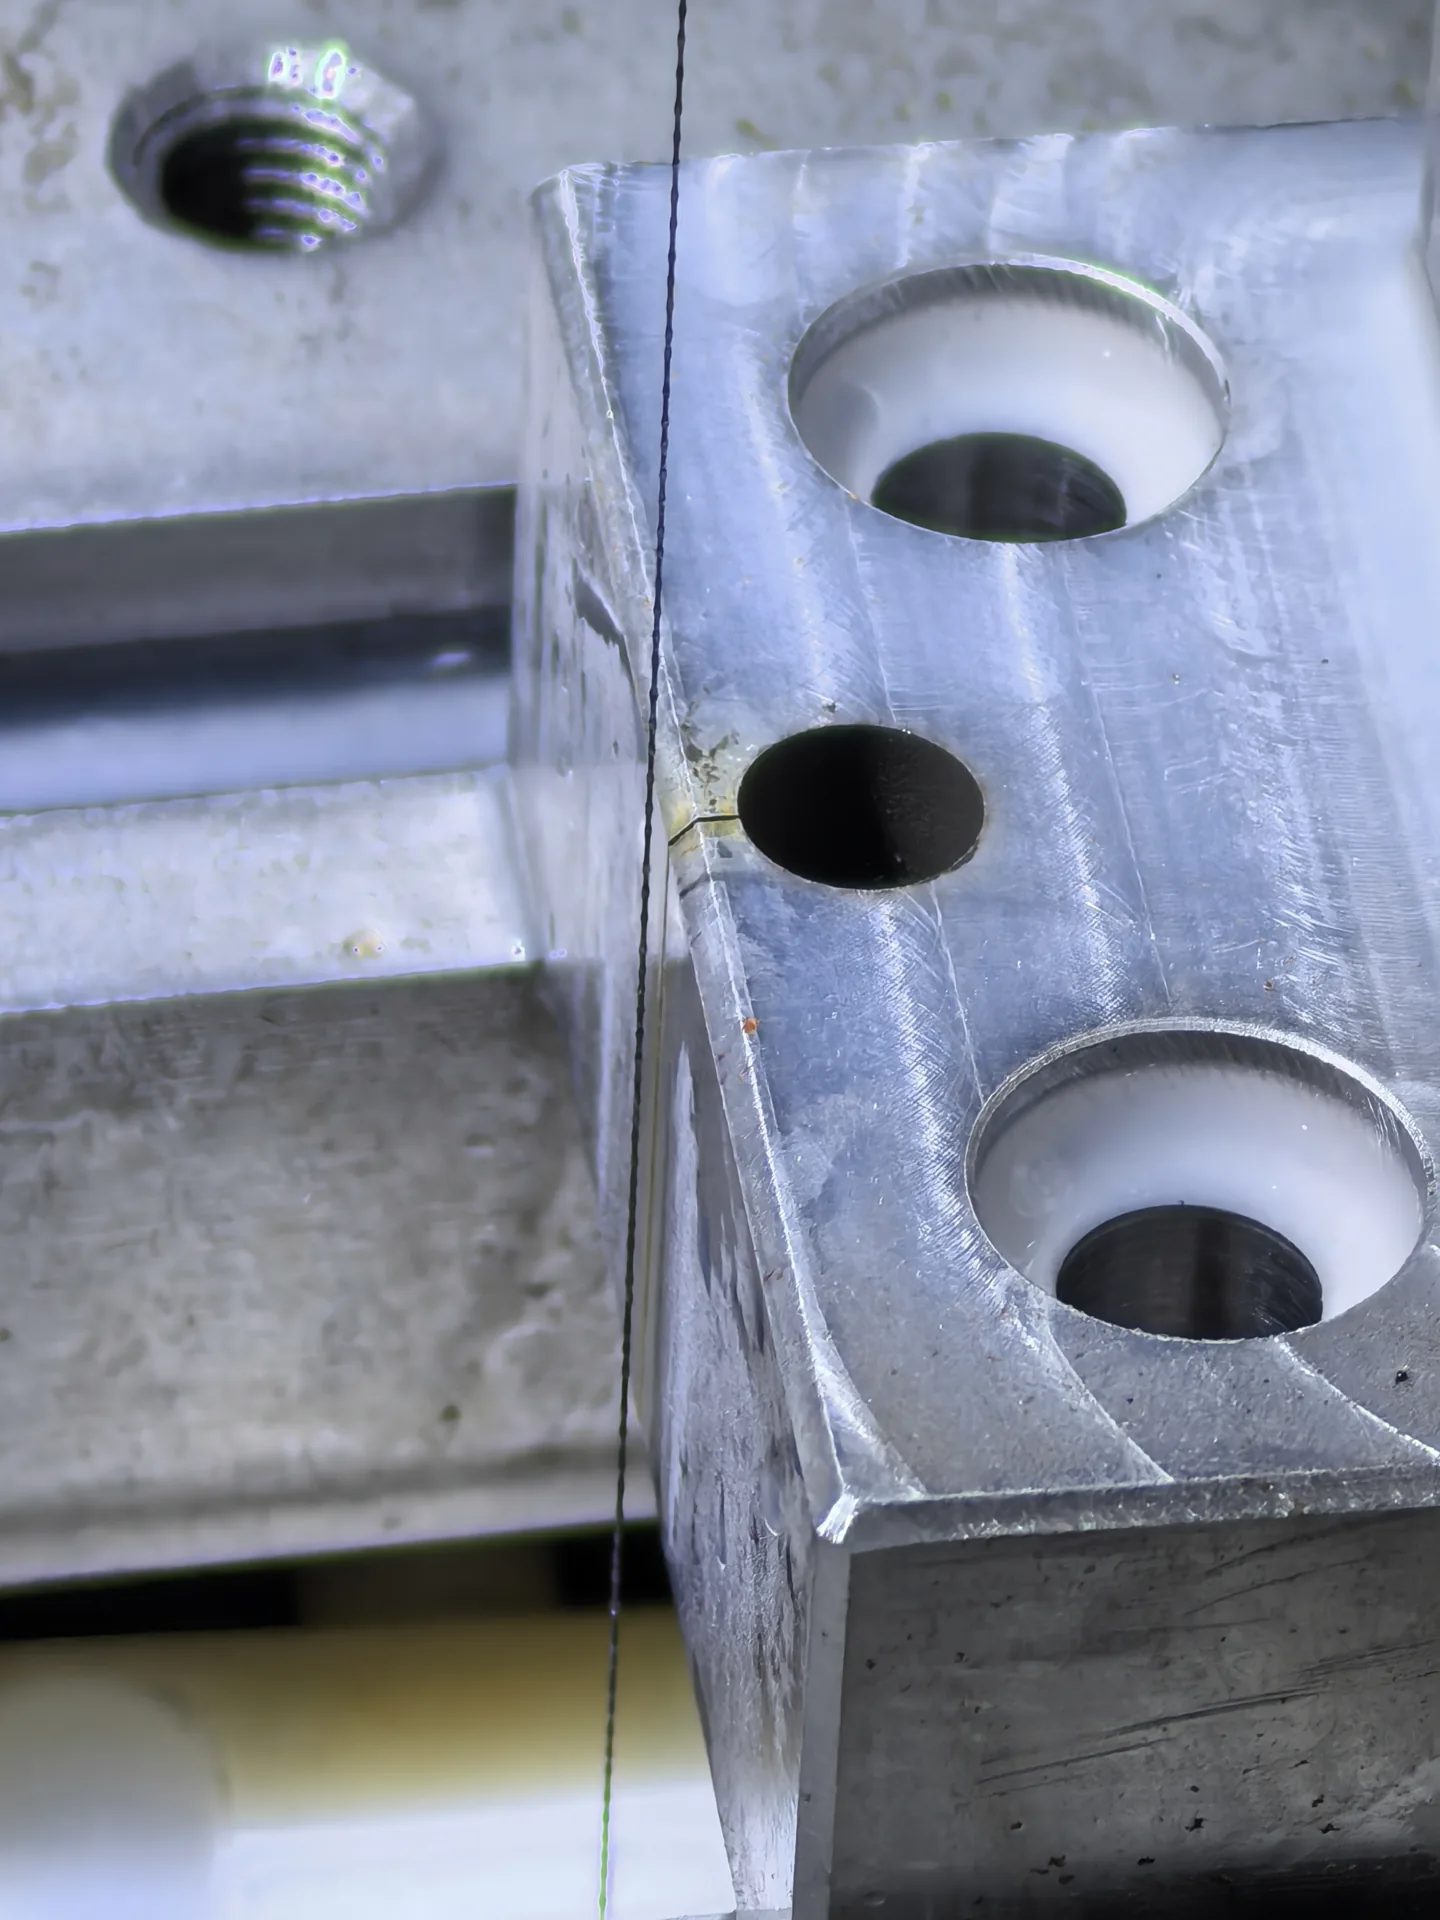
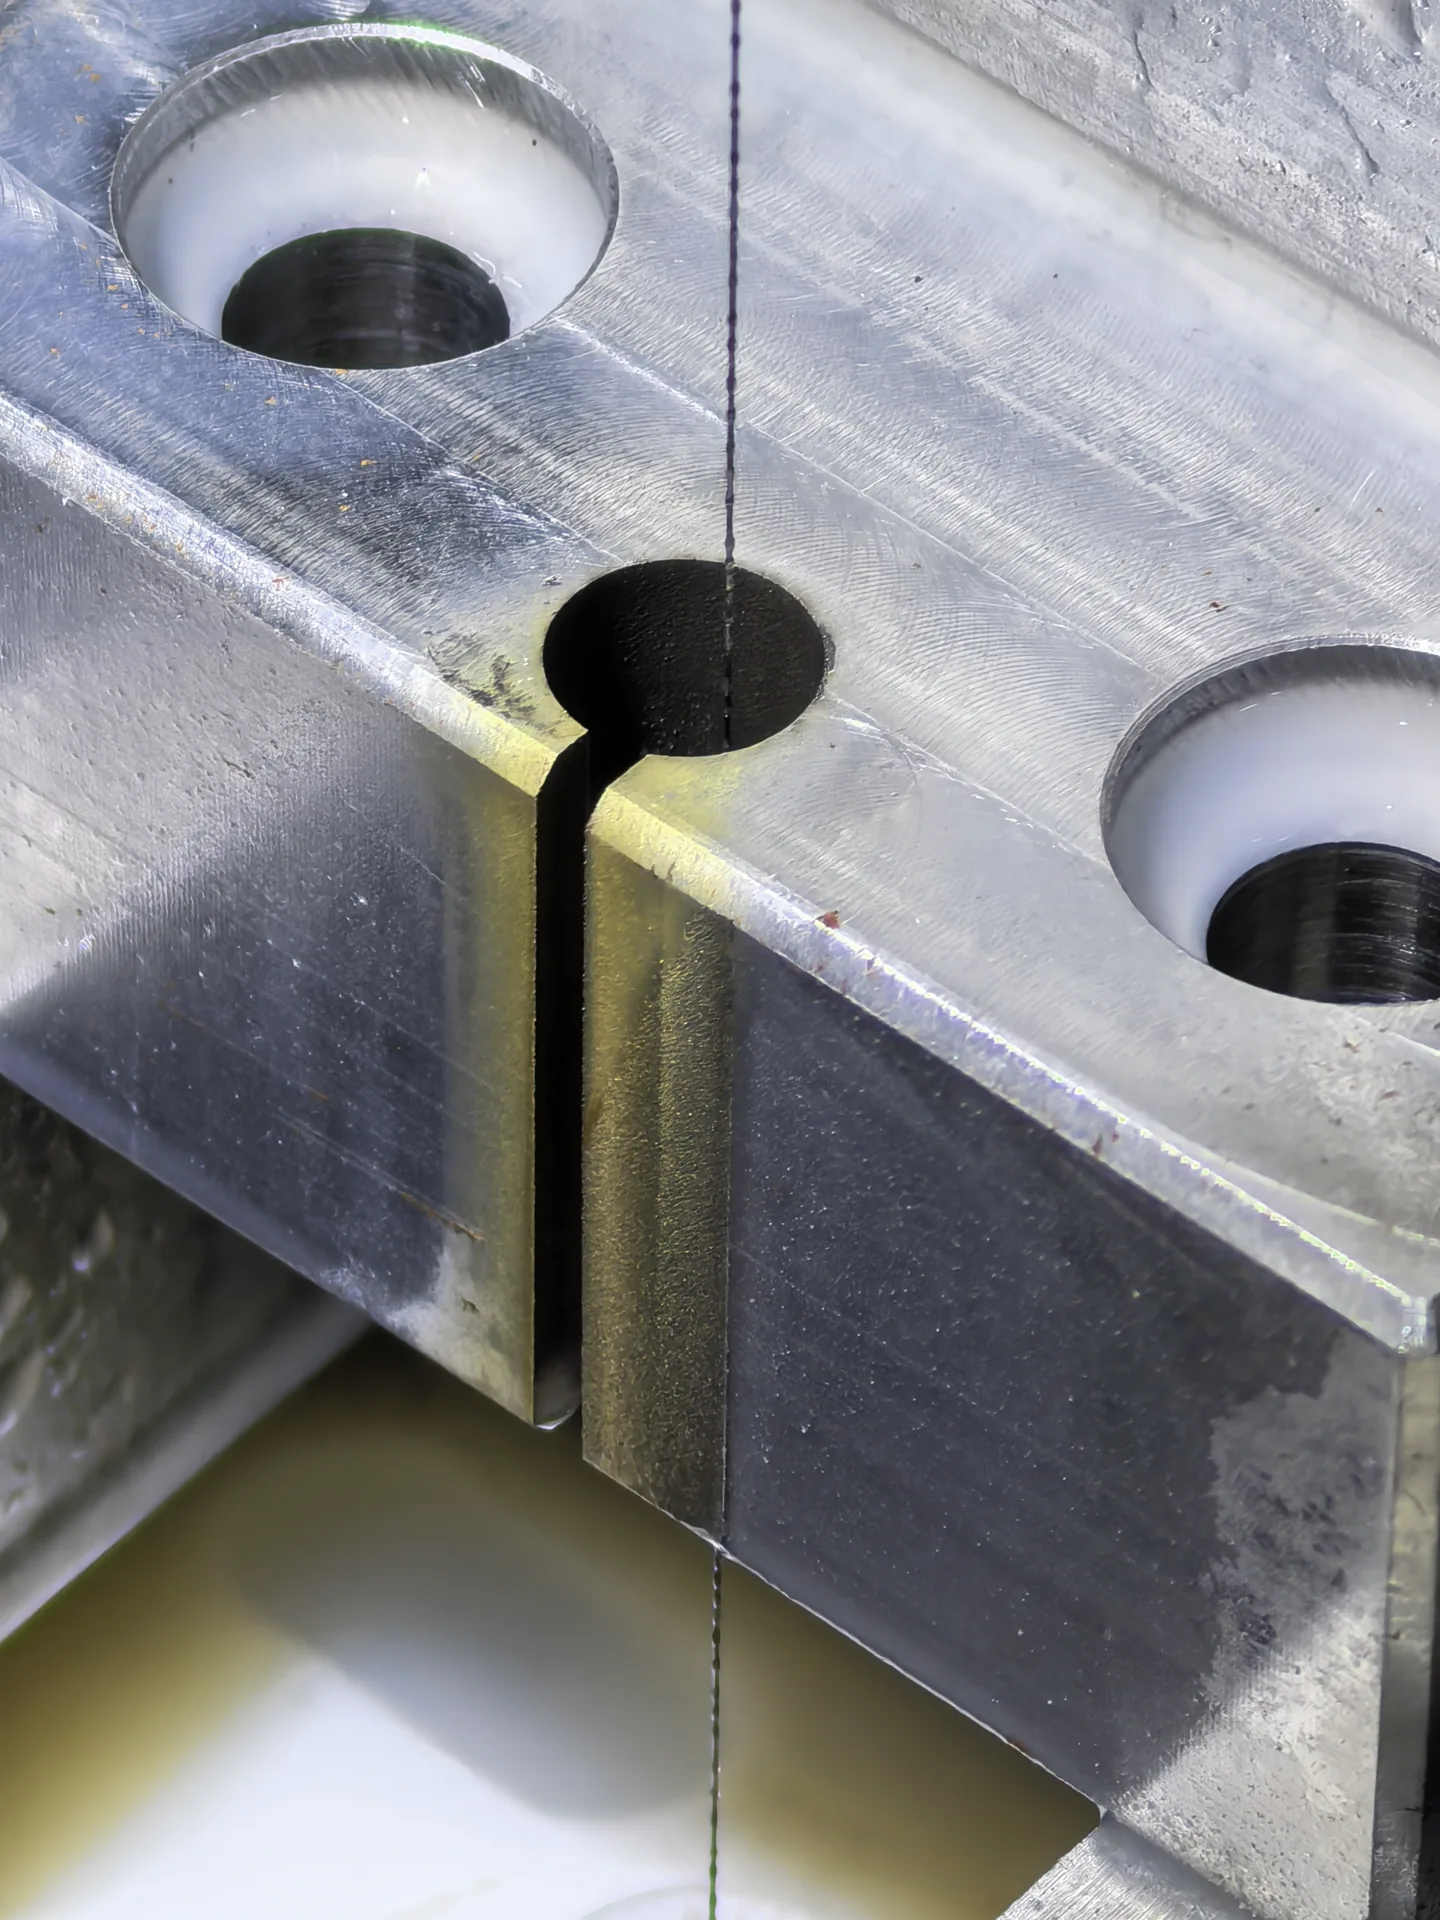
Wire EDM in our workshop.
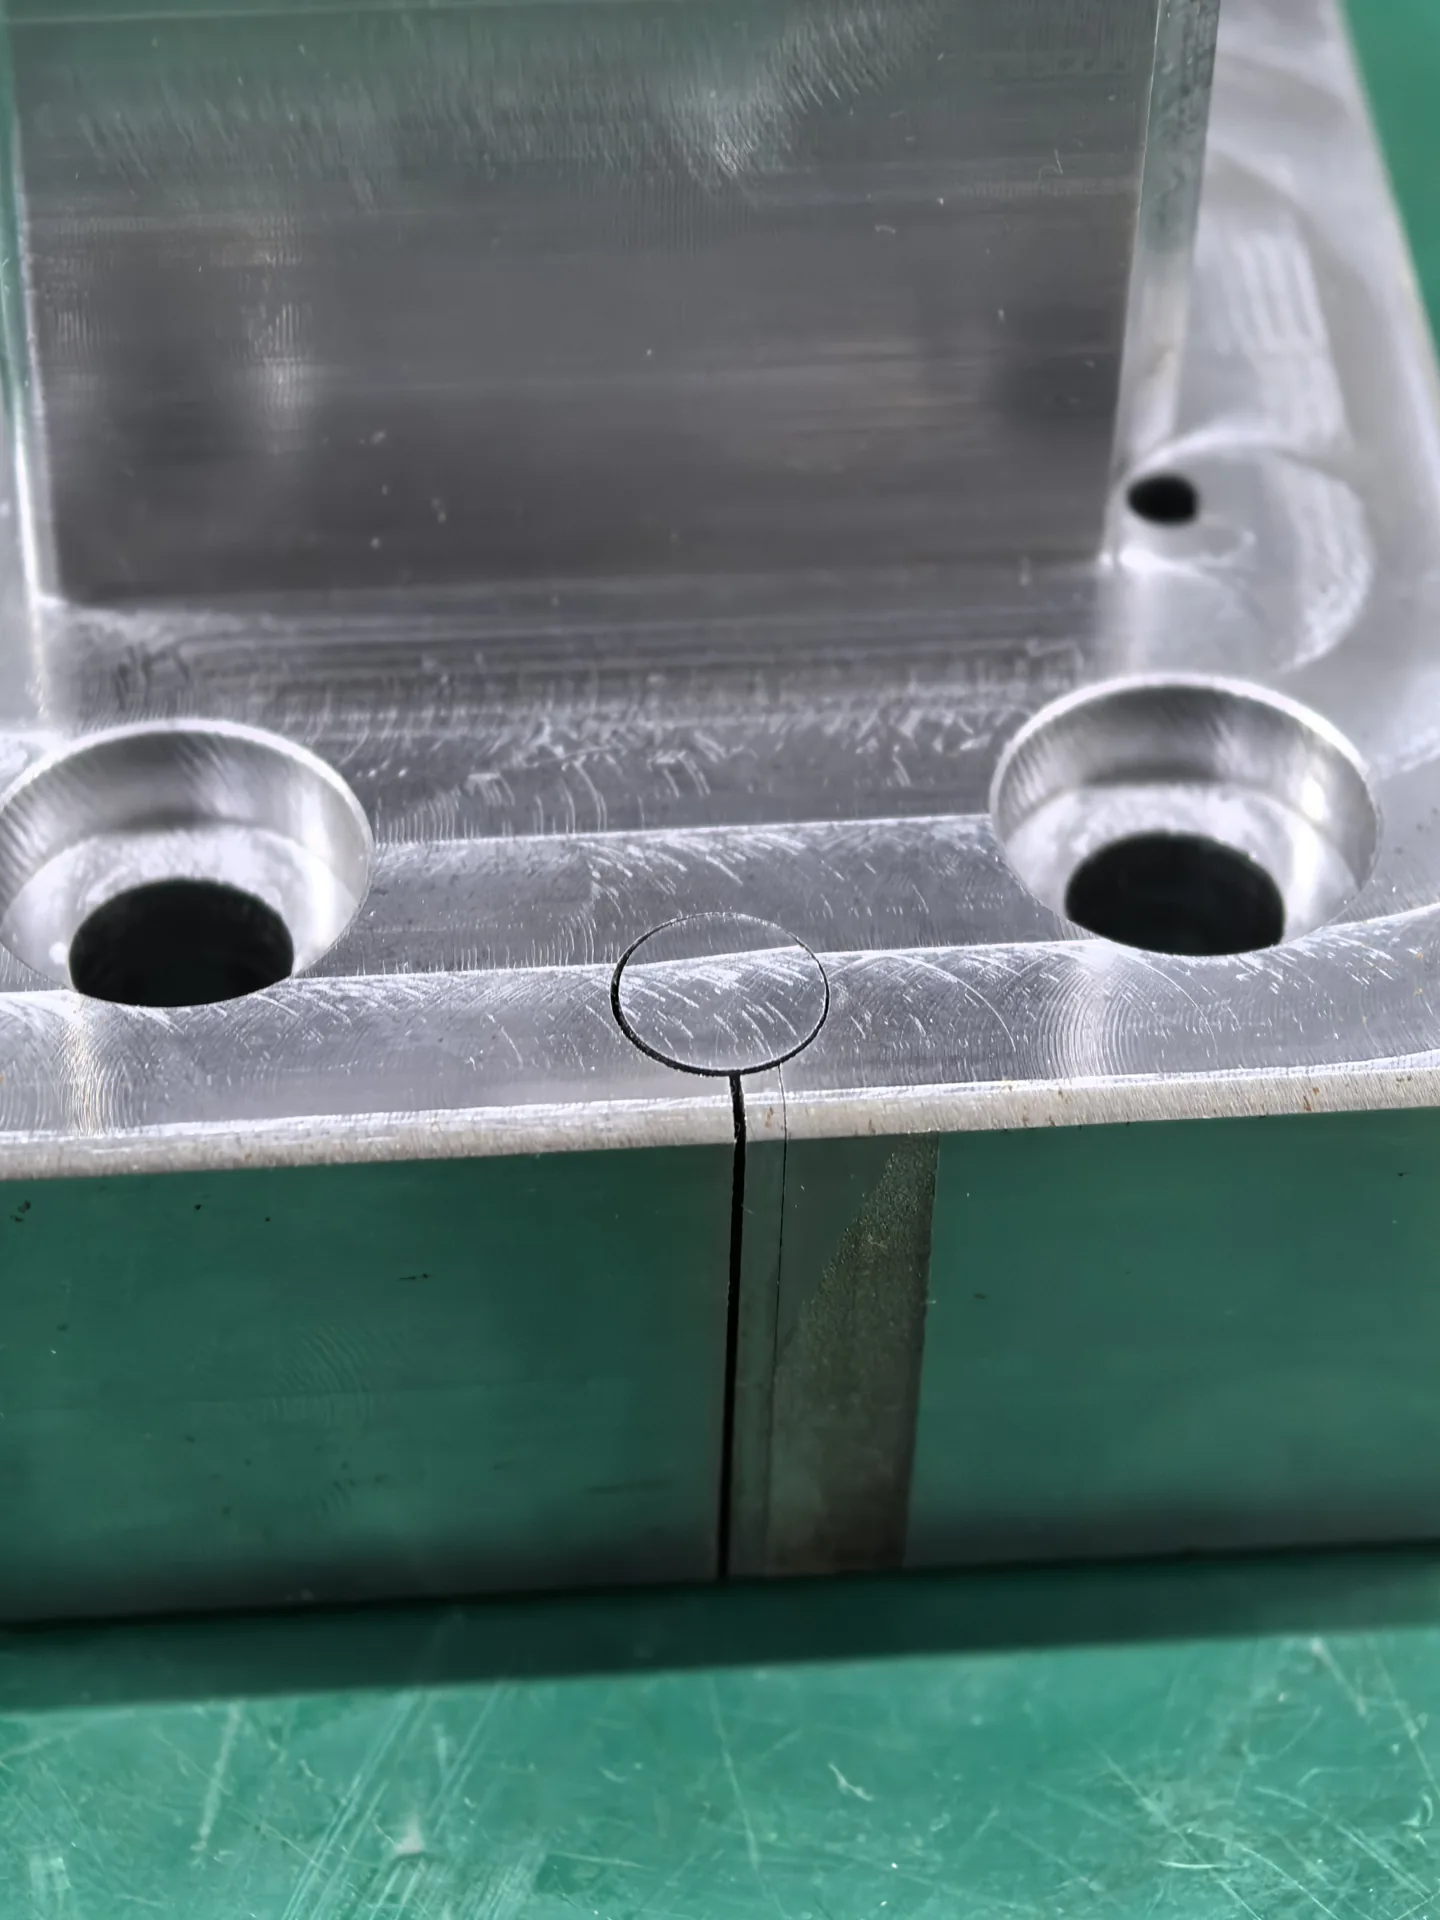
Factory demonstration photographs show the setup, wire path and cut details. These images illustrate the process; dimensional accuracy and surface finish are verified against the agreed inspection requirements.
Wire EDM materials.
Start with conductivity.
Can wire EDM cut plastic?
Electrical conductivity is essential. Ordinary insulating plastics, glass and nonconductive ceramics are unsuitable for conventional wire EDM. Specialty conductive composites require a separate feasibility review.
| Material family | Typical reason to consider wire EDM | Include in your RFQ |
|---|---|---|
| Tool and alloy steels | Hardened tooling, dies and wear profiles | Grade, hardness and heat-treatment sequence |
| Stainless steels | Corrosion-resistant precision profiles | Exact grade, corrosion and passivation requirements |
| Aluminum, brass and copper | Complex outlines in conductive alloys | Alloy, temper, thickness and cosmetic requirements |
| Titanium and nickel alloys | Difficult-to-machine conductive components | Grade, surface-integrity limits and inspection needs |
| Cemented carbide | Wear-resistant tooling; suitability depends on composition | Binder composition, grade and application for feasibility review |
Design details that change the result
Allow for the wire and spark gap
The kerf is wider than the wire. An internal corner cannot be perfectly sharp: its radius depends on wire radius, discharge gap and process control. Dimension the allowable radius rather than assuming a zero-radius corner.
Plan access and support
Closed profiles need a start hole. Identify permitted entry locations, keep-out areas and the required cut direction. Thin walls and released slugs need support; residual stress in the stock can move the part during cutting.
Specify the finished condition
Show datums, profile tolerances, perpendicularity and critical fits. Include heat treatment, coating allowances and the inspection condition. Tighter finish or geometry requirements may require additional skim passes.
Control thermal surface effects
Wire EDM is a thermal erosion process. Recast material and a heat-affected layer may remain despite low mechanical force. Flag fatigue, sealing or safety-critical surfaces so finishing and verification can be agreed before manufacture.
Wire EDM, milling or sinker EDM?
| Process | Best-fit geometry | Key limitation |
|---|---|---|
| Wire EDM | Intricate through profiles in conductive material | Needs a wire path through the part; thermal surface effects |
| CNC milling | Pockets, faces, holes and broad material removal | Tool access, cutting forces and internal tool radius |
| Sinker EDM | Blind cavities and shaped recesses in conductive material | Requires a shaped electrode and separate process planning |
A combined route may be appropriate: mill the stock and reference features, heat treat as required, then wire-cut critical profiles. Explore CNC machining.
Define acceptance before the first cut
Drawing and process review
Confirm material condition, datum strategy, critical dimensions and any surface-integrity constraints. Resolve drawing/model differences before release.
Inspection matched to function
Agree which characteristics need dimensional measurement, profile checks, roughness verification or first-article documentation. Reporting scope and any specialist testing must be confirmed in the quote.
What to request with your order
- Material certification and traceability requirements
- Ballooned drawing and agreed inspection report
- First-article or sample approval where required
- Edge condition, cleaning, protection and packaging
YOUR NEXT WIRE EDM PROJECT
Let us review
your wire-cut part.
Share your drawing and tell us what the part needs to do. We will review the machining route, material, finish and inspection needs with your quote.
Your files stay confidential. Optional NDA available ↗
Wire EDM service questions
Can wire EDM cut hardened steel?
Yes. Electrical conductivity rather than hardness enables spark erosion. Specify the grade and heat-treated condition; residual stress and surface requirements still affect process planning.
What tolerance can you achieve?
Send the dimensions, datums, material and cut thickness for review. Tolerance and roughness are confirmed for the individual feature and inspection plan, rather than guaranteed by a single site-wide number.
Can wire EDM make blind holes or pockets?
Conventional wire EDM requires a through path for the wire. Blind features generally need milling, sinker EDM or another suitable operation.
Does wire EDM leave a heat-affected surface?
Yes. The process uses localized electrical discharges and can leave recast material and a heat-affected layer. Additional passes or finishing may be required for demanding applications.
How can I reduce wire EDM cost?
Apply tight tolerances only to functional features, permit practical corner radii, simplify setups and specify finish only where needed. Include order quantities and inspection needs so the route can be costed accurately.
Can you quote from a 2D drawing?
A clear dimensioned drawing can support initial review of a through profile. Include material, thickness, quantity, tolerances and finish. A model helps clarify taper and more complex geometry.