ADDITIVE MANUFACTURING
3D Printing
Services
Turn a digital model into a part with the right process, material and finishing route for its intended use.
PROCESS ROUTESSLA · FDM · SLS · DMLS
PROJECT SCOPEModels · prototypes · functional parts
ACCEPTANCEMaterial, finish & dimensions agreed
Start with what the part needs to do.
3D printing builds parts layer by layer from a digital model. ProleanTech reviews your application across resin, filament, polymer powder and metal powder routes. A visual model, a loaded fixture and a metal component need different decisions about material, build direction and acceptance.
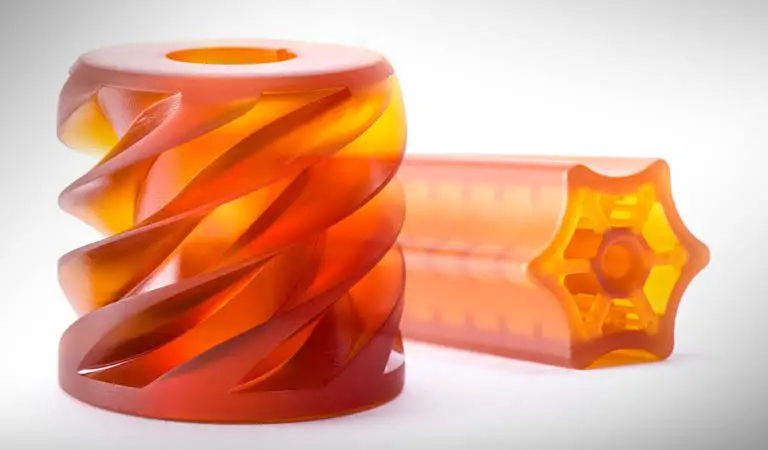
Fine detail & visual models
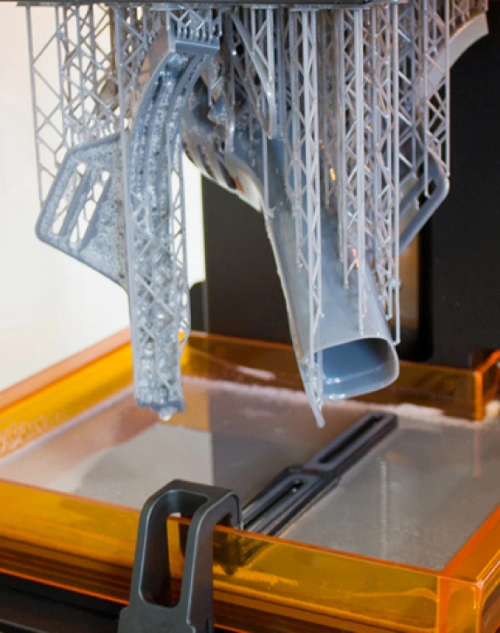
Stereolithography cures a liquid photopolymer resin with light. Consider it for detailed housings, presentation models and fit checks where surface quality matters.
- Material route
- Standard, clear and engineering photopolymer resins; castable formulations for a specified casting workflow.
- Design focus
- Mark cosmetic faces and support-contact exclusions. Hollow sections need drainage and cleaning access. Resin properties depend on the exact formulation and post-cure.
A resin described as ABS-like is not ABS thermoplastic. Compare its data sheet against your temperature, impact and aging requirements.
Thermoplastic prototypes & fixtures
Fused deposition modeling extrudes heated thermoplastic filament along a toolpath. Consider it for concept iterations, handling fixtures and functional prototypes with accessible geometry.
- Material route
- PLA, ABS, PETG, nylon and TPU filament families. PVA, when compatible, is a removable support material.
- Design focus
- Orient the part around load direction, layer bonding and supported surfaces. Define wall construction and infill when they affect the test.
The filament name alone does not establish the properties of the printed part. Review layer direction, moisture conditioning and the actual build settings.
Functional polymer parts & small batches
Selective laser sintering fuses polymer powder with a laser. Surrounding loose powder supports the build, allowing complex shapes without the attached supports used in SLA or FDM.
- Material route
- PA12 and PA11 nylon powders; filled nylon, TPU and PP are process-specific alternatives to discuss.
- Design focus
- Provide powder-escape paths in hollow parts. Review thin walls, long flat sections, clearances and cleaning access. Expect a textured surface before finishing.
A powder-supported build still needs depowdering and cooling. Sealing, smoothness and dimensional fit are separate requirements.
Complex metal geometry
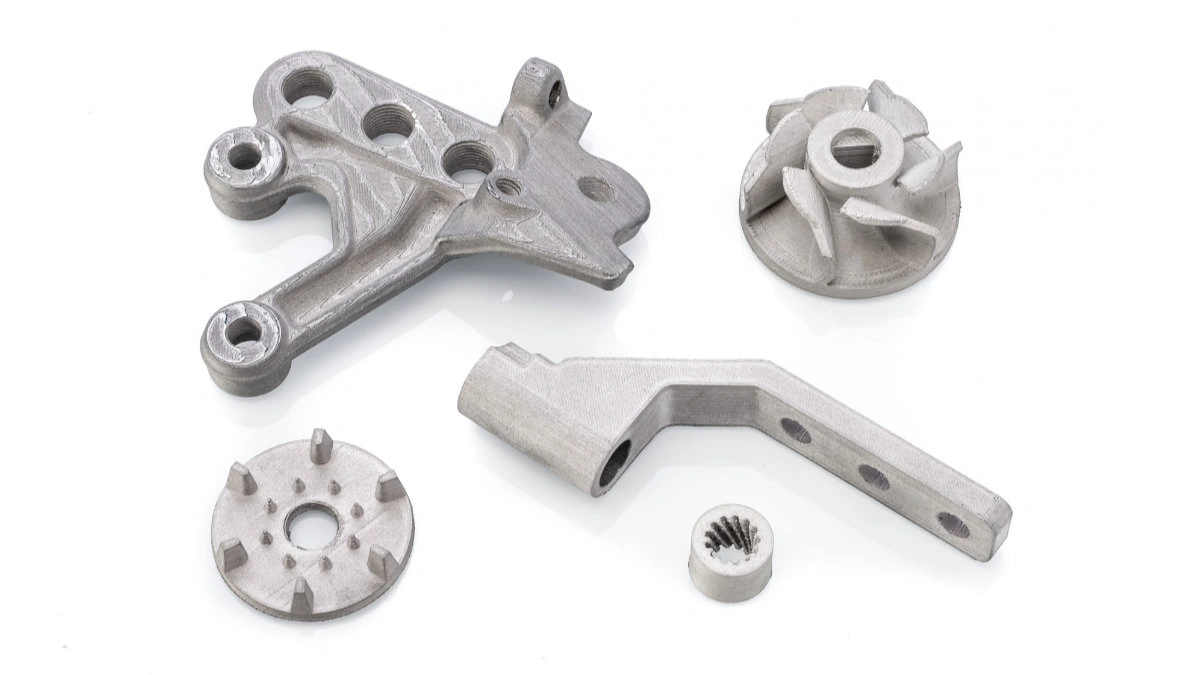
Direct metal laser sintering is a metal laser powder bed fusion route. Common engineering alloys are melted and consolidated layer by layer. Consider it when internal passages or part consolidation justify the complete manufacturing route.
- Material route
- Aluminum, titanium, maraging steel, cobalt-chromium and nickel-alloy powder families, subject to alloy and route confirmation.
- Design focus
- Review orientation, thermal distortion, supports and removal access. Allow stock and locating features for machining critical interfaces.
Include depowdering, heat treatment, support removal, machining and inspection in the scope. Material family does not establish an application qualification.
Process availability, exact material grade, build envelope and achievable dimensions are confirmed for your project. Select a process to see the design considerations.
| Route | Useful starting point | Build / removal constraint | Before acceptance |
|---|---|---|---|
| SLA | Detailed resin models and appearance studies | Support contact, trapped resin and drainage | Cleaning, specified cure and cosmetic work |
| FDM | Thermoplastic iterations and fixtures | Layer direction, overhangs and support access | Support removal, fit and load-direction review |
| SLS | Complex functional polymer geometry | Powder escape, warping and clearances | Cooling, depowdering and specified finish |
| DMLS | Metal geometry with an additive advantage | Thermal effects, support and tool access | Agreed thermal, machining and inspection route |
Specify a material.
Then qualify the printed condition.
Choose from the process-compatible families below as a starting point for review. Request the exact grade and data sheet; a family name does not establish strength, temperature resistance, color, compliance or current stock.
Photopolymer resins
Standard and clear resins suit visual evaluation. Engineering formulations target specific toughness, stiffness or thermal behavior. Castable resins need a compatible burnout and casting route. Specify the property you need rather than a visual resemblance to another plastic.
Thermoplastic filaments
PLA for concept work; ABS or PETG for selected functional requirements; nylon where wear and toughness matter; TPU for compliant geometry. Grade, conditioning and print direction affect performance. A soluble support such as PVA is not a substitute for the part material.
Polymer powders
PA12 and PA11 are nylon starting points. Filled nylon, TPU and PP require a compatible powder system and confirmed availability. Review stiffness, elongation, moisture response and texture. A filled material may trade ductility for stiffness.
Metal alloy powders
Request the exact aluminum, titanium, maraging steel, cobalt-chromium or nickel alloy. Powder specification, processing and heat-treated condition matter. State material documentation and traceability requirements; an alloy name alone does not establish medical or aerospace suitability.
Already have a material specification? Include the grade, required condition and documentation. Any substitution needs your approval.
Design the build.
Leave room to finish it.
Orientation connects strength, surface quality, supports and dimensional behavior. Mark the functional interfaces before the build route is set, including faces that must remain free of support marks.
Load direction & orientation
Identify load paths and the surfaces used to locate the part. FDM layer bonding can make properties direction-dependent; orientation also affects stair-stepping, support contact and distortion in other routes.
Wall thickness & local features
Review unsupported walls, pins, text and thin edges against the selected process and material. Long flat areas and abrupt section changes may distort. Minimum printable detail is not a promise of durable functional wall thickness.
Supports, drainage & escape paths
Allow access to remove supports, resin or powder. Enclosed channels and lattices need a cleaning strategy. Powder support in SLS does not make an inaccessible hollow volume cleanable.
Fits, holes & machining stock
Specify clearance or interference at the assembly. Review small holes, threads and bearing seats individually. Metal parts may need machining stock, datums and tool access to reach the final interface requirement.
AFTER THE BUILD
The finish is part of the process.
Define the delivered condition at quotation. Printing, cleaning, cosmetic finishing and functional machining are separate operations; each can change dimensions, texture and cost.
Clean & stabilize
SLA: remove residual resin and use the specified cure. FDM: remove accessible supports. SLS: cool and depowder. DMLS: plan powder removal and the agreed thermal sequence. Heat treatment manages material condition or stress; it is not a universal surface-smoothing method.
Control the appearance
Discuss sanding, suitable blasting, painting or compatible dyeing for the selected material. Review vapor smoothing only for a validated material/process pairing. Mark visible faces and agree color, texture and acceptable support marks.
Protect the interfaces
Mask surfaces where coating build would affect fit. Specify whether dimensions apply after finishing. Do not assume a coating makes a porous print leak-tight; sealing and chemical resistance require their own acceptance criteria.
Layer thickness is a setting.
Tolerance is an agreement.
A thin layer can improve vertical detail without guaranteeing the location, size or flatness of every feature. Printer resolution, minimum feature size and finished-part tolerance describe different things.
Define the controlled features
Provide units, datums, drawing revision and critical dimensions. Identify appearance requirements and mating parts. Agree deviations before release rather than relying on one blanket tolerance across all processes.
Check the delivered condition
Agree whether measurement follows cure, conditioning, heat treatment, coating or machining. Flexible parts may need a defined fixture and measurement method. Sampling and report scope belong in the order.
Validate what matters in service
Request dimensional, material and process records where needed. Define functional tests for load, leakage or temperature separately. Internal channels may need additional inspection; accessibility and method must be agreed before manufacture.
Choose the route around the finished part.
Compare the complete cost, performance and validation needs. There is no single quantity at which every design should switch processes.
Stay with 3D printing
Design changes, complex geometry or low tooling commitment may favor additive manufacturing. Include supports, build utilization, cleaning, finishing and inspection in the comparison.
Good question: what must this iteration prove?
Compare CNC machining
Consider machining when stock-material properties and accessible precision surfaces are central. Tool access limits geometry, but machining can also finish selected interfaces on a printed metal part.
Compare injection molding
For a stable thermoplastic design and repeat demand, review tooling investment, molded material behavior, cosmetic requirements and revision risk. Printed prototypes do not reproduce every property of molded production parts.
From model to an agreed manufacturing route.
- Send the part definition
Model, controlled drawing, application, quantity and required delivery date.
- Resolve the route
Confirm material, orientation constraints, DFM changes, finish and inspection with the quotation.
- Approve & manufacture
Release the agreed revision. Define sample approval before a repeat batch when needed.
- Verify & deliver
Check the agreed acceptance criteria and documents; protect surfaces and delicate features for transport.
3D printing questions,
answered.
Practical details for your next engineering review.
Which 3D printing processes can I request?
Discuss SLA, FDM, SLS or DMLS with ProleanTech. Send the model, application, material requirements and quantity so the available process, grade, build size and finishing route can be confirmed in your quotation.
Is SLA resin the same as nylon or ABS?
No. SLA uses photopolymer resin. Nylon powders belong to routes such as SLS, while nylon and ABS filaments can be used in FDM. An ABS-like resin describes a formulated property profile; it does not identify ABS thermoplastic.
What tolerance can my printed part achieve?
Tolerance depends on process, material, geometry, orientation, size and post-processing. Send a controlled drawing with datums and critical dimensions. Agree which dimensions apply to the as-printed part and which apply after finishing or machining. Layer thickness and printer resolution are not finished-part tolerance guarantees.
Does SLS need supports?
Loose powder supports the part during a polymer SLS build, so attached support structures are generally unnecessary. Hollow parts still need accessible powder-removal paths. Wall stability, distortion, clearances and surface texture need review for the selected material and geometry.
Can printed parts be sanded, painted or smoothed?
Finishing depends on the material and process. Sanding and painting can improve appearance; suitable polymer grades may support dyeing or a validated smoothing treatment. Metal parts may need blasting, heat treatment or machining. Specify visible faces, color, texture, masking and final dimensions before selecting a route.
Can I use a printed part for a functional test?
Define the load, temperature, environment, duration and acceptance test first. Printed material, orientation, wall construction and post-processing must represent what the test needs to measure. A successful fit check alone does not validate fatigue, sealing, flammability or long-term service.
When should I choose CNC machining or injection molding?
Compare CNC machining when stock-material properties, accessible precision interfaces or machined surfaces are central to the requirement. Compare injection molding for a stable thermoplastic design with repeat demand that supports tooling investment. Compare total finished-part cost and validation needs rather than a fixed quantity threshold.
What files, quantities and delivery information should I send?
Send a 3D model and a revision-controlled 2D drawing with units, quantity breaks, material or target properties, critical dimensions and finish requirements. Add intended use, destination, required date and inspection documents. Include STL mesh units and export quality if using a mesh. Timing and price are confirmed after review.
YOUR NEXT PRINTED PART
Share the model.
Define the requirement.
Tell us what the part needs to demonstrate or do in service. We’ll review the process, material and finished condition with your quotation.
Your files stay confidential. Optional NDA available →