Metal material guide
Brass CNC
Machining
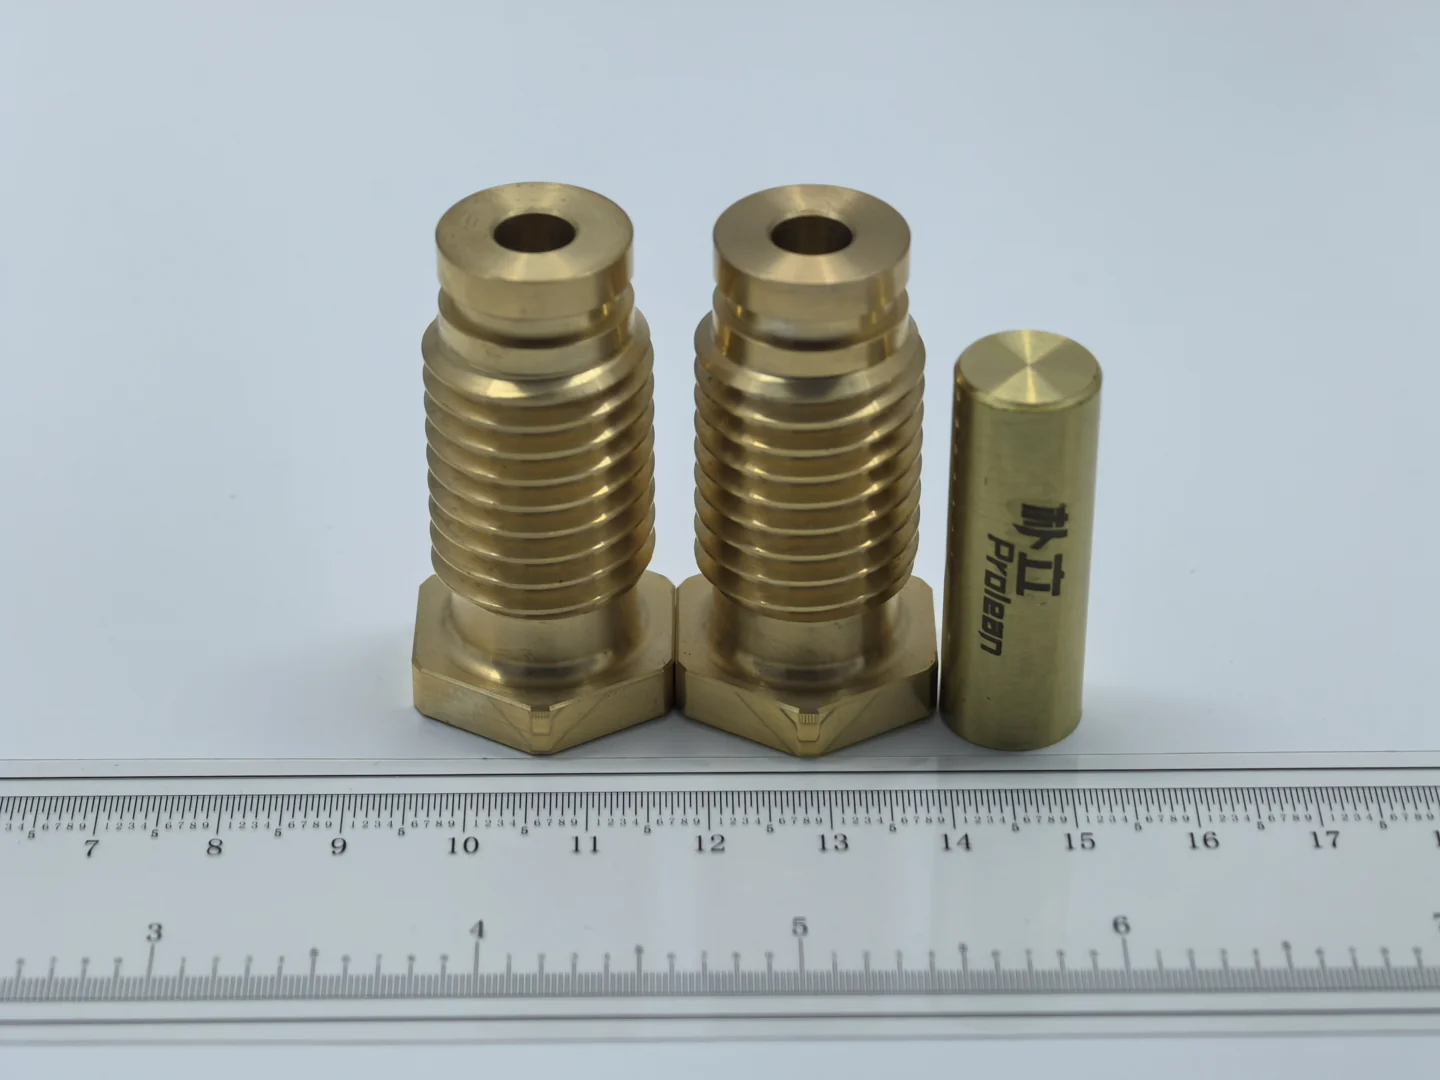
CNC fittings, connectors and small precision components, with the brass alloy, lead restrictions and sealing requirements defined together.
Confidential enquiries. NDA available.
- Specify
- C36000 or named alternative
- Review
- Thread standard and Seal seat
- Confirm
- Final condition and acceptance records
Choose Brass Around The Connection And Its Service.
Brass is often considered for turned geometry and detailed fittings. The selected alloy must also suit fluid contact, joining, corrosion exposure and any restrictions on composition.
Threaded Fittings
Specify thread standard, engagement and the actual sealing feature. A thread fit and a leak acceptance requirement describe different checks.
Electrical Connectors
Identify mating surfaces, required contact performance and plating. Include any restrictions on lead content or restricted substances.
Small Mechanisms
Mark cross holes, slots and burr-sensitive edges. Review wear contacts and whether the part will be formed, soldered or otherwise joined.
Choose The Grade And Stock Together.
Compare the Brass options below against the drawing and service conditions. Specify the complete supplier grade, condition and stock form; material examples do not establish current inventory or permit substitutions.
| Grade or stock | Why consider it | What to resolve |
|---|---|---|
| C36000 | Turned details where the specified free-cutting brass is acceptable. | Confirm whether lead content is permitted for the intended use. |
| C26000 | A brass specification often considered when forming and ductility are relevant. | Review stock form and secondary machining rather than assuming C36000 cutting behaviour. |
| C46400 | A named naval-brass specification for an appropriate corrosion-led design. | Confirm the exact service environment, product form and joining requirements. |
| Named low-lead or lead-free alloy | Applications governed by a composition or end-use restriction. | State the exact alloy, governing requirement and supporting document package. |
Selection examples are subject to material and drawing review. They are not an inventory list.
Already have a grade on the drawing?
Add it to your quotation checklist ↓Make Threads, Seats And Internal Edges Explicit.
For a small turned fitting, the most important requirements can sit inside a bore or at the end of a thread. Include sections or detail views where they clarify acceptance.
Sealing Surfaces
Mark the seat geometry, contact face and finish. Distinguish surface appearance from a required leak or pressure test.
Cross Holes And Burr Control
Identify internal intersections and small slots. Define which edges may be broken and where burr removal must preserve flow or sealing.
Thin Sections
Show wall thickness around threads and ports. Review clamping and the sequence of operations before assuming a universal minimum wall.
Mark critical dimensions on the drawing. Achievable tolerances, wall thickness, part size and delivery are confirmed for the geometry, material, finish and quantity in the quotation.
Finish Brass For The Interface It Serves.
As-Machined
Define marks, edges and any preservation requirement. Agree the appearance of visible areas rather than using colour to identify the alloy.
Nickel Or Other Plating
State the deposit requirement, thickness, contact function and protected surfaces. Dimensions apply in the agreed finished state.
Polished Or Cosmetic Surfaces
Define the visible faces and acceptance sample. Protect threads, seals and identification features from unwanted material removal.
Separate Composition, Dimensions And Functional Tests.
Material Composition
Require the specified alloy and the records needed for any composition restriction. A yellow appearance cannot prove lead content.
Thread And Seat Inspection
Name the thread standard and fit, critical bore dimensions and sealing-surface checks.
Functional Acceptance
If leak, pressure or contact-resistance testing is required, define the method, conditions and acceptance separately from dimensional inspection.
Three Different Checks.
The material record identifies the purchased stock. The inspection report checks the drawing. Application validation checks the part in service.
Review inspection requirements ↗Brass Machining Questions.
Answers to the decisions that affect the material, drawing and finished part.
Is C36000 Lead-Free?
No. It is classified as a leaded free-cutting brass. If lead restrictions matter, specify the applicable requirement and an approved alloy.
Can A Brass Colour Confirm The Alloy?
No. Use the material specification and required records. Colour and plating can disguise composition differences.
Does A Correctly Gauged Thread Prove A Fitting Is Leak-Tight?
No. A thread gauge checks a defined dimensional requirement. Leakage depends on the sealing design, assembly and the agreed test conditions.
Can C26000 Replace C36000?
Only after review. Forming, machining, composition and performance requirements differ; the drawing owner must approve a substitution.
When Should Plating Be Specified?
Include it with the RFQ so the process, thickness, masking and final fits can be considered before machining.
What Helps Quote A Small Brass Fitting?
Provide a section view, alloy, thread standard, internal burr requirements, sealing-face criteria, finish, quantity and any functional test.
Prepare your enquiry
Specify The Brass Alloy And The Finished Connection.
Send the CAD model and dimensioned drawing with quantities, service conditions and the requirements below. If the grade is undecided, describe the function and the constraints.
Your files stay confidential. NDA available.
Brass RFQ Checklist
Material: [brass UNS grade + product form]
Composition restrictions: [requirement + supporting records]
Connections: [thread standard, fit, sealing seat]
Internal details: [cross holes, burr-sensitive locations]
Finish and tests: [plating, final dimensions, leak test if required]
Quantity: [order and repeat quantities]
Material References & Specification Notes
Manufacturer information supports material selection. Use the datasheet for the exact grade, stock form and test conditions. It does not establish Prolean inventory, application approval or a guaranteed machining result.
Prepared October 2026. Final material and manufacturing requirements are agreed in the quotation.