CUSTOM MACHINED FEATURES
Sinker EDM
Services
Custom electrical discharge machining for slots, blind cavities and tooling features in conductive metals, with electrode design and inspection reviewed together.
Your files stay confidential. Optional NDA available →
Sinker EDM for features
that challenge a cutting tool.
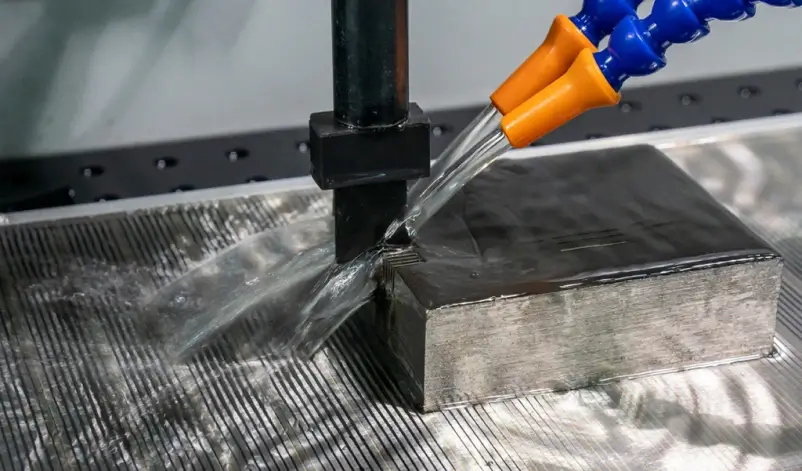
Sinker EDM, also called die-sinking or ram EDM, also known as spark machining, removes material through controlled electrical discharges between a shaped electrode and a conductive workpiece in dielectric fluid. It is useful when tool access, material hardness or cavity geometry makes conventional machining difficult.
| Feature | What we review |
|---|---|
| Blind cavities and recesses | Electrode access, cavity depth, corner radii, flushing and any required finishing allowance. |
| Narrow slots and detailed profiles | Slot width, depth, wall thickness and electrode stiffness. Small features remain subject to electrode manufacture, wear and discharge-gap limits. |
| Mold and die details | Ribs, inserts and shaped recesses in tooling. Supply the heat-treated condition, mating geometry and surface requirement. |
| Prototype and repeat production | Part envelope, weight, quantity, electrode life, replacement needs and inspection scope. Large-part feasibility requires confirmation of machine travel and loading. Tooling effort affects the first-order price and repeat-order economics. |
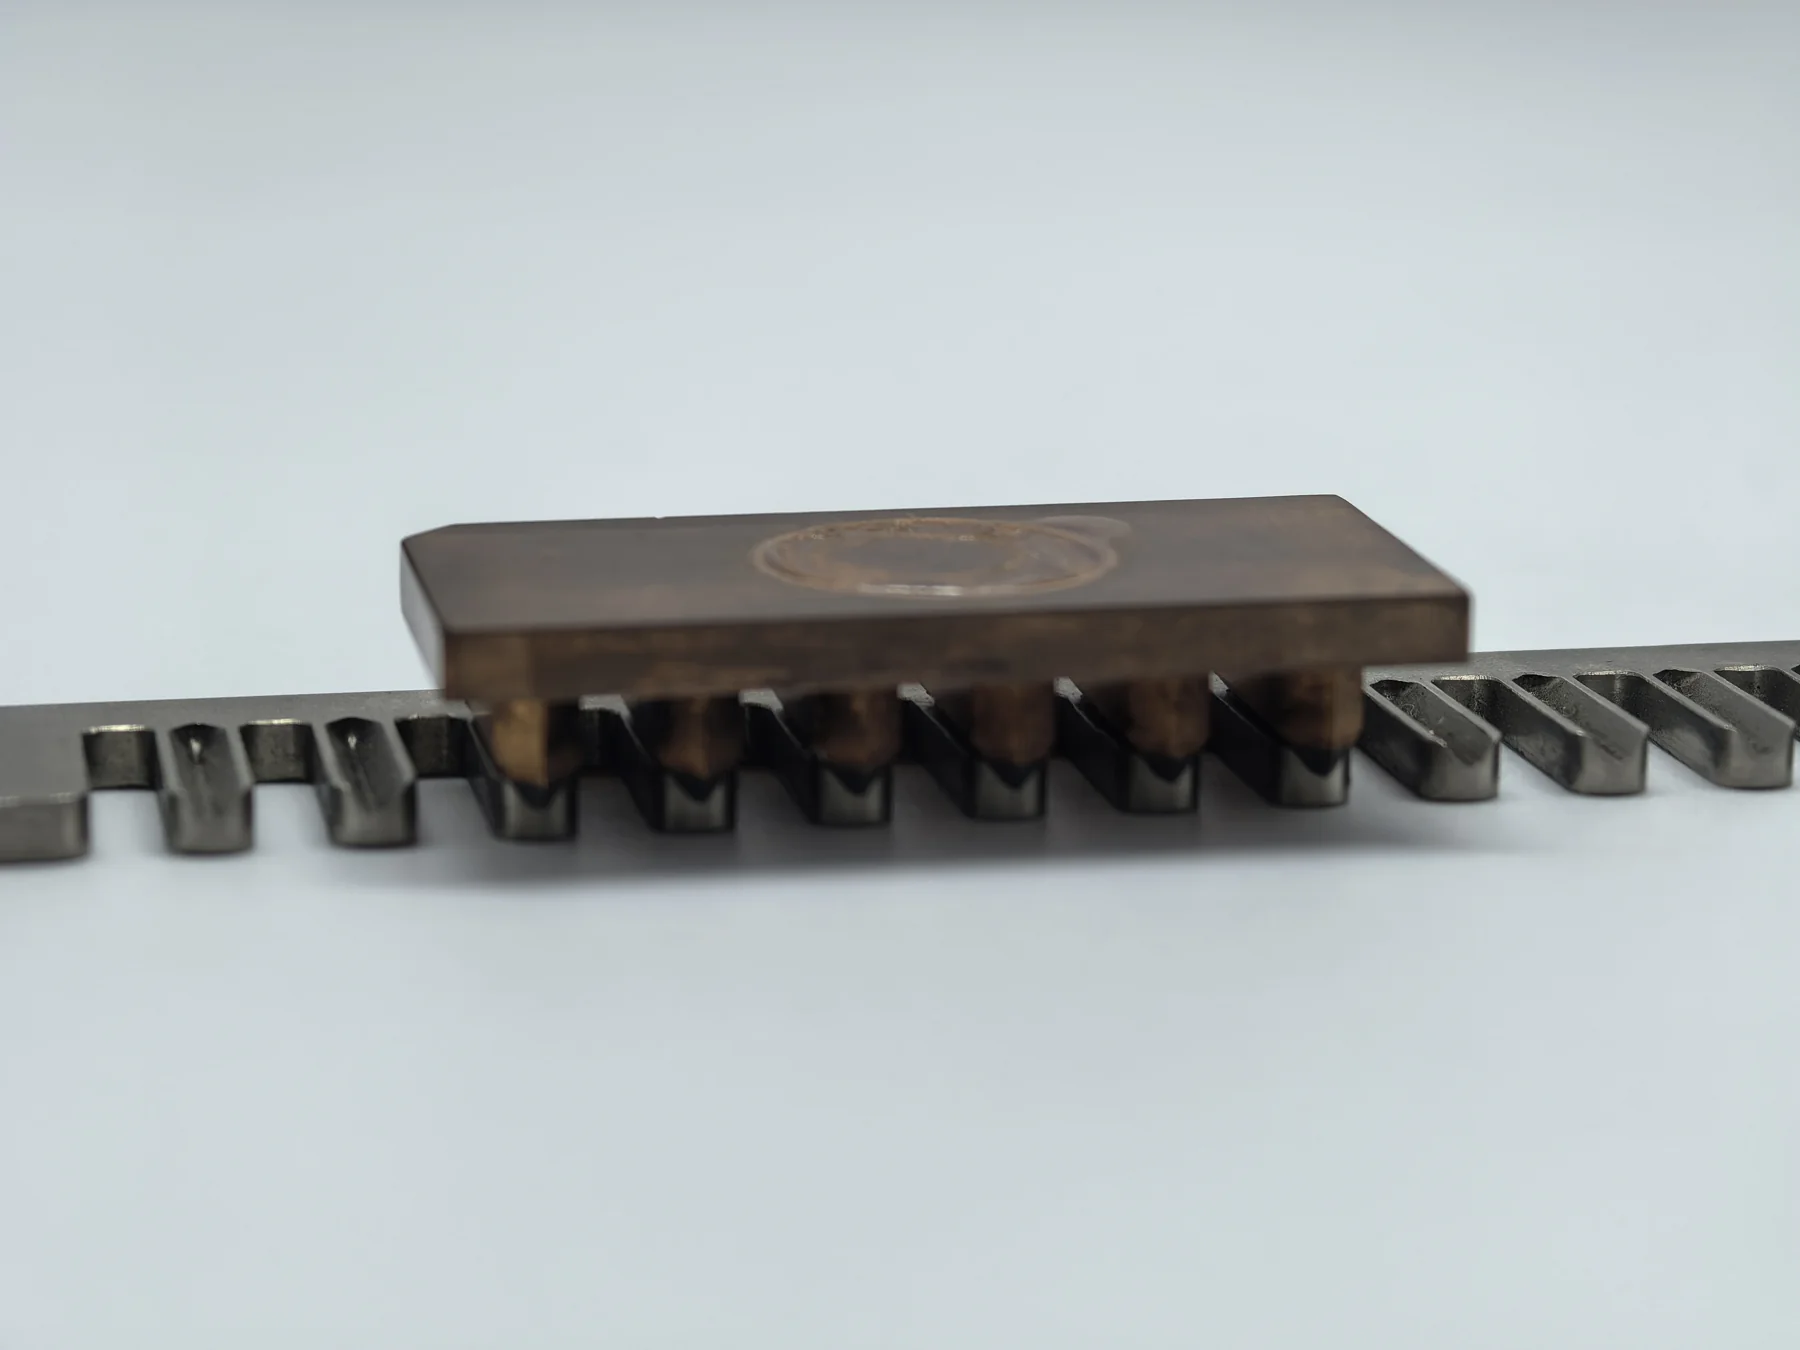
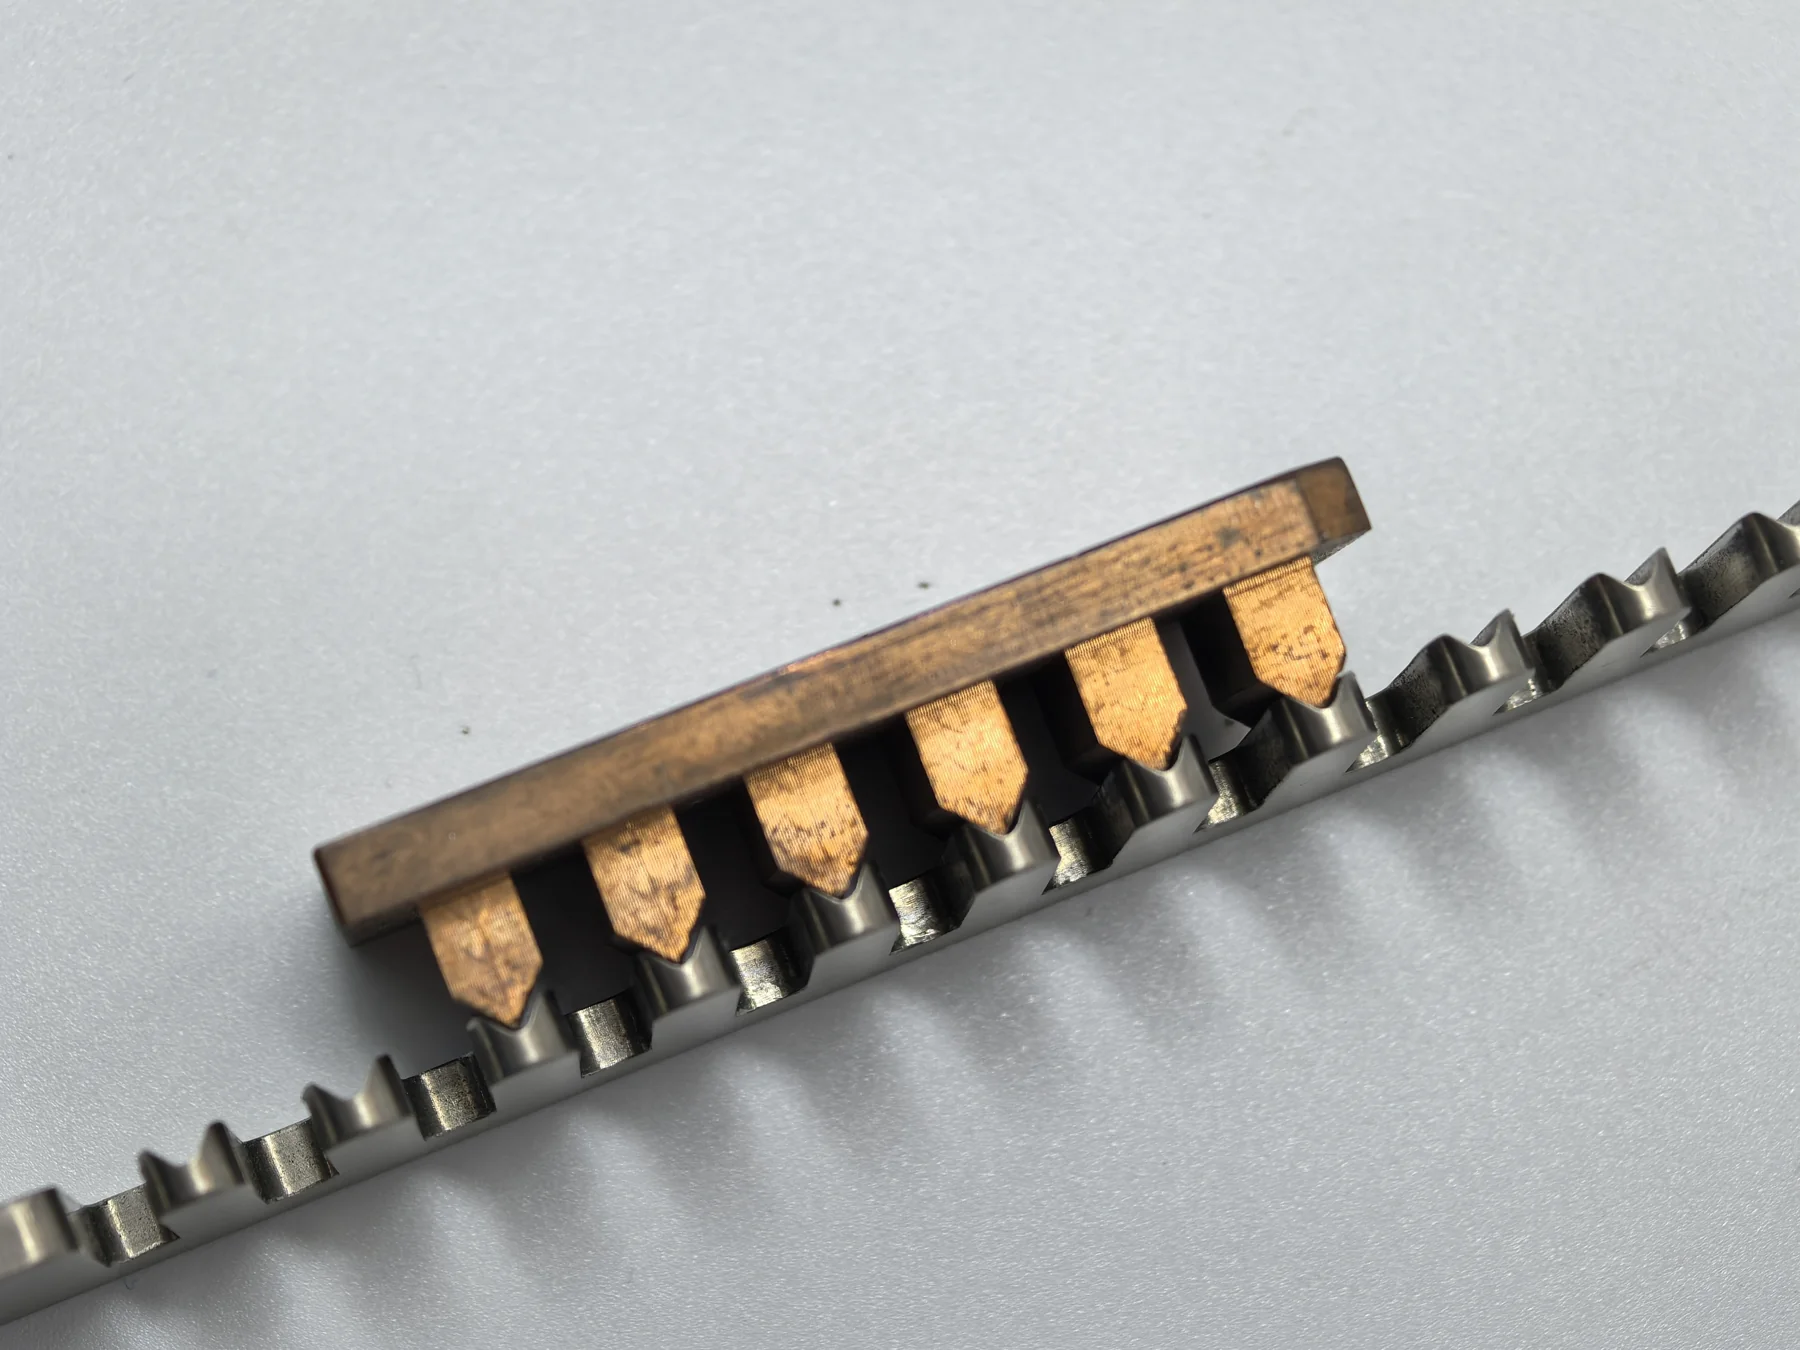
A copper electrode.
A defined slot geometry.
This supplied machining example shows the copper electrode used to machine the slots and the associated workpiece. The two views show how the shaped tool relates to the repeated feature geometry.
Need a similar slot or repeated cavity?
Send the slot section, depth, pitch, corner limits and datum scheme. Electrode offsets compensate for the working gap; the electrode is not simply an exact-size copy of the final cavity.
From electrode design
to a verified feature.
Review the drawing and plan the electrode
Confirm material condition, cavity geometry, datums and acceptance criteria. Choose electrode material and geometry around accessibility, wear and the required finish.
Make and reference the electrode
Copper and graphite are common electrode materials. Manufacture and locate the tool, allowing for the discharge gap, wear and the selected roughing or finishing strategy.
Control the discharge and flushing
The servo maintains a working gap while pulsed discharges erode the workpiece. Dielectric circulation removes debris; poor flushing can limit deep or narrow features.
Finish and inspect
Inspect the agreed features after machining and any specified polishing or surface treatment. Additional electrodes or finishing stages may be needed to meet the drawing.
Choose the EDM process
around the geometry.
| Process | Suitable feature | Planning requirement |
|---|---|---|
| Sinker EDM | Blind cavities, shaped recesses and slots | A custom electrode and accessible approach direction; allow for wear and flushing. |
| Wire EDM | Through profiles, contours and slots | The wire must pass through the workpiece; closed internal contours need a start hole. |
| EDM drilling | Small or deep holes in conductive materials | Hole diameter, depth, breakthrough and surface requirements need separate feasibility review. |
| CNC milling | Accessible pockets, faces and bulk material removal | Tool reach, internal radius and material hardness influence feasibility. |
For through profiles, see our wire EDM services. A combined milling and EDM route may reduce electrode work and overall machining time.
Conductive workpiece materials.
Conductivity is essential for conventional EDM. Hardness alone is not the limiting factor, but alloy condition, thermal behavior and surface requirements still influence the process.
| Material family | Project information required |
|---|---|
| Tool steels and hardened alloy steels | Grade, hardness, heat-treatment history and any distortion-sensitive geometry. |
| Stainless steels | Exact alloy, corrosion requirements and any post-machining treatment. |
| Aluminum, copper and copper alloys | Grade, temper and geometry. Distinguish the workpiece material from the electrode material. |
| Titanium and nickel alloys | Exact grade, service conditions and any fatigue or surface-integrity requirements. |
| Cemented carbide | Grade and binder composition. Suitability, surface damage and finishing need specific review. |
Ordinary plastics and nonconductive ceramics are unsuitable for conventional sinker EDM. Specialty conductive materials require a separate assessment.
Specify the feature.
Leave room for a reliable process.
Depth, ribs and internal corners
Provide a section view showing cavity depth, slot width, draft and wall thickness. Deep narrow details limit flushing and electrode strength. A perfectly sharp internal corner is not a default outcome; agree a practical radius.
Electrode access and datum control
Show the tool approach and any obstructing surfaces. Define the datums that locate the cavity relative to the rest of the part. Electrode location and wear affect the finished geometry.
Tolerance and finish
Mark critical dimensions and specify roughness with units. Achievable tolerance and Ra depend on material, geometry, electrode and finishing strategy. Requirements are confirmed after drawing review.
Recast layer and thermal effects
EDM applies little mechanical cutting force, but it is a thermal process. Recast material, a heat-affected layer and microcracking can matter in demanding service. Identify surfaces requiring removal, polishing or specialist verification.
Agree acceptance before machining.
Match inspection to the feature
Confirm slot size, depth, spacing, profile and datum relationships. Deep cavities may require a specific measurement method; discuss accessibility before choosing acceptance criteria.
Inspect in the final required condition
Specify whether measurement is before or after heat treatment, polishing or coating. Material certificates, first-article reports and specialist surface tests must be included in the agreed order scope.
Define in your purchase order
- Drawing revision and applicable datums
- Material grade and supplied condition
- Critical dimensions and surface finish
- Inspection report and traceability needs
- Edge condition, cleaning and protection
YOUR NEXT SINKER EDM PROJECT
Let us review
your EDM feature.
Share your drawing and tell us what the part needs to do. We will review the machining route, material, finish and inspection needs with your quote.
Your files stay confidential. Optional NDA available ↗
Sinker EDM service questions.
What is the difference between sinker EDM and wire EDM?
Sinker EDM uses a shaped electrode to machine cavities and recesses. Wire EDM uses a moving wire to cut through profiles. The part geometry and access determine which route is appropriate.
Can sinker EDM machine a blind slot?
Yes, a shaped electrode can machine a blind slot when the approach, electrode stiffness and flushing are feasible. Send the width, depth, section and allowable corner radius for review.
Why use a copper electrode?
Copper can be machined into a shaped electrode and offers useful conductivity and wear behavior. Electrode selection also depends on the workpiece, feature detail and finish; graphite is another common option.
What tolerance and finish can you achieve?
Both are feature-specific. Supply the material, cavity dimensions, datums and roughness requirement. The quote should confirm the achievable result and inspection method rather than rely on a universal accuracy claim.
Does EDM change the surface?
EDM removes material thermally and may leave recast material and a heat-affected layer. Additional finishing or verification may be required for fatigue-critical or other demanding surfaces.
What affects sinker EDM pricing and lead time?
Electrode design and manufacture, cavity depth and complexity, number of setups, roughing and finishing cycles, electrode replacement and inspection all affect cost and schedule. Quantity and requested date should be supplied for quotation.