
CUSTOM PROFILES / FINISHED COMPONENTS
Aluminum Extrusion
ServicesOne profile.
More possibilities.
Bring your cross-section to life. Custom aluminum profiles with cutting, CNC machining and surface finishing planned around the requirements of your finished part.
Confidential enquiries · Optional NDA available
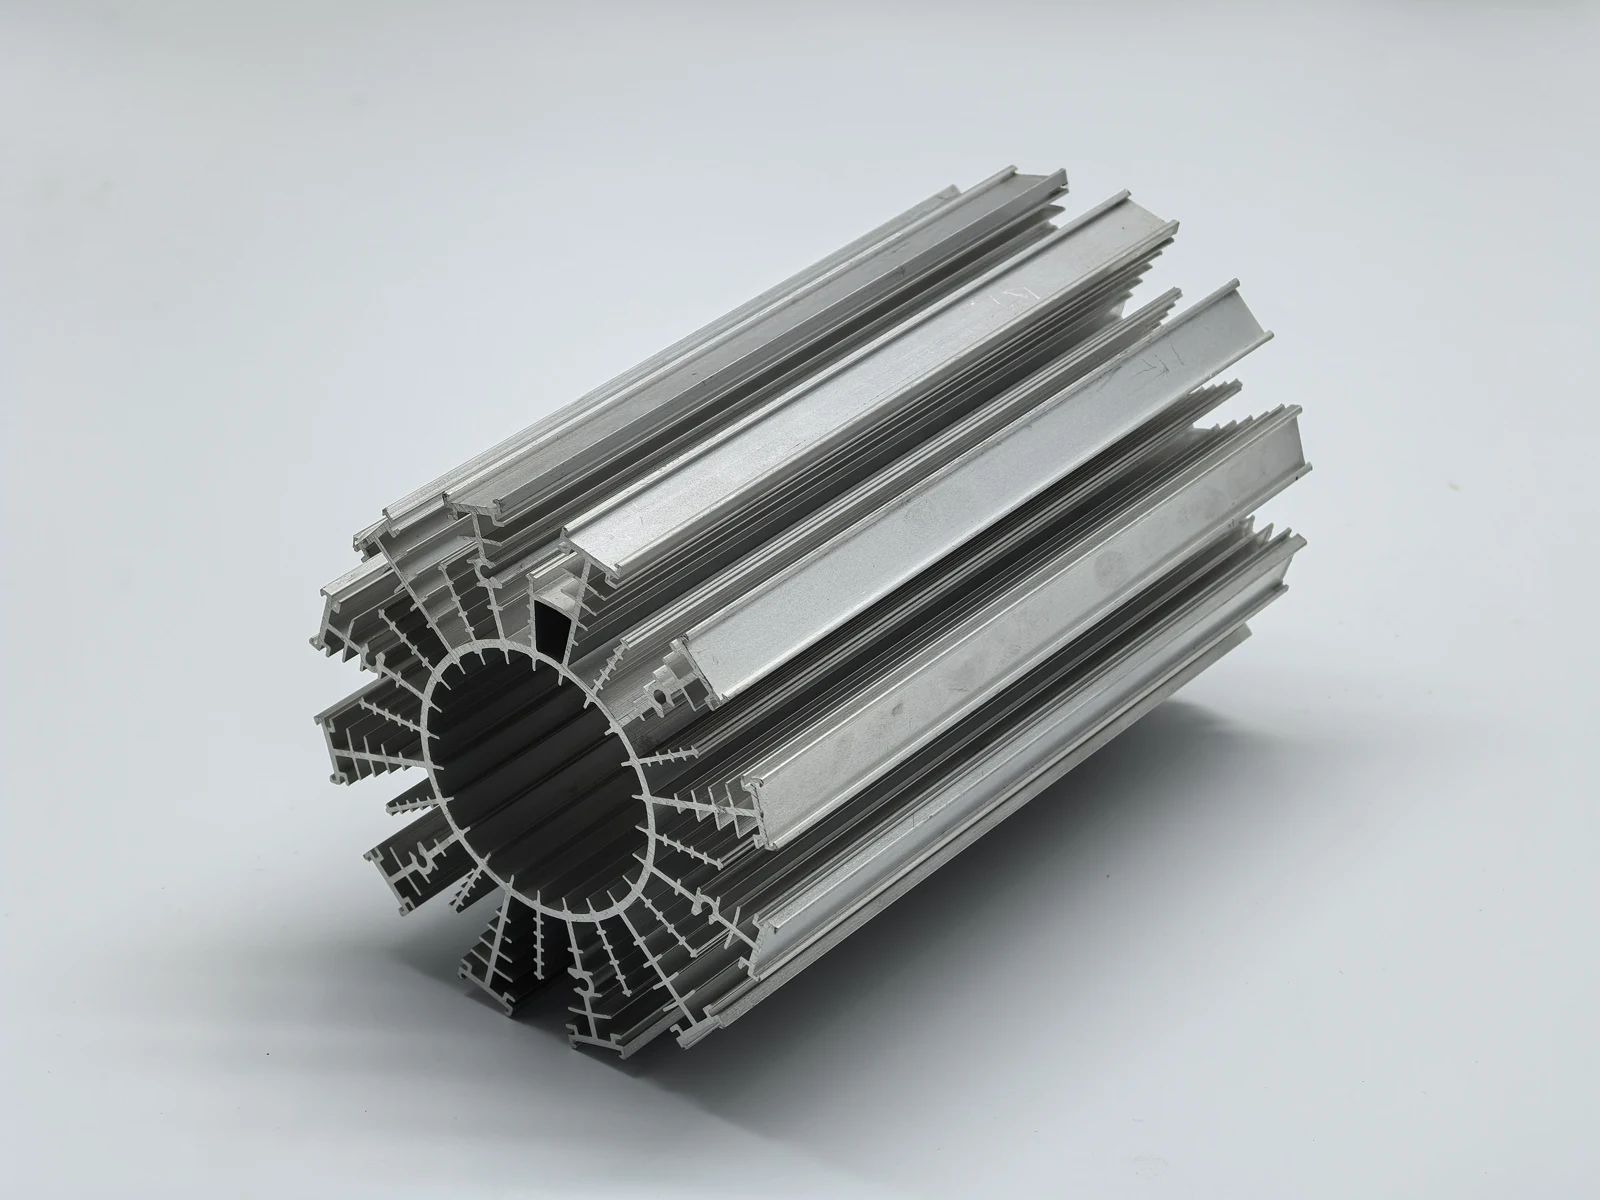
01 / YOUR ALUMINUM EXTRUSION PARTNER
From the right cross-section
to the finished part.
Extrusion forms a continuous cross-section. Secondary operations add the length, holes, threads and interfaces your assembly needs. Review the complete component before committing to tooling.
Custom profile extrusion
Solid, hollow and semi-hollow sections, reviewed for wall balance, die complexity and the intended alloy and temper.
Cutting & CNC machining
Cut-to-length profiles with drilled holes, tapped features, pockets and machined mating faces defined by your drawing.
Finishing for function
Review anodizing, powder coating or mechanical finishing together with cosmetic faces, masking and dimensional requirements.
02 / REAL EXTRUDED PROFILE EXAMPLES
A cross-section does
more than define a shape.
Fins, channels and hollow sections bring multiple functions into one profile. These supplied part photographs show examples of geometry for discussion with your engineering team.
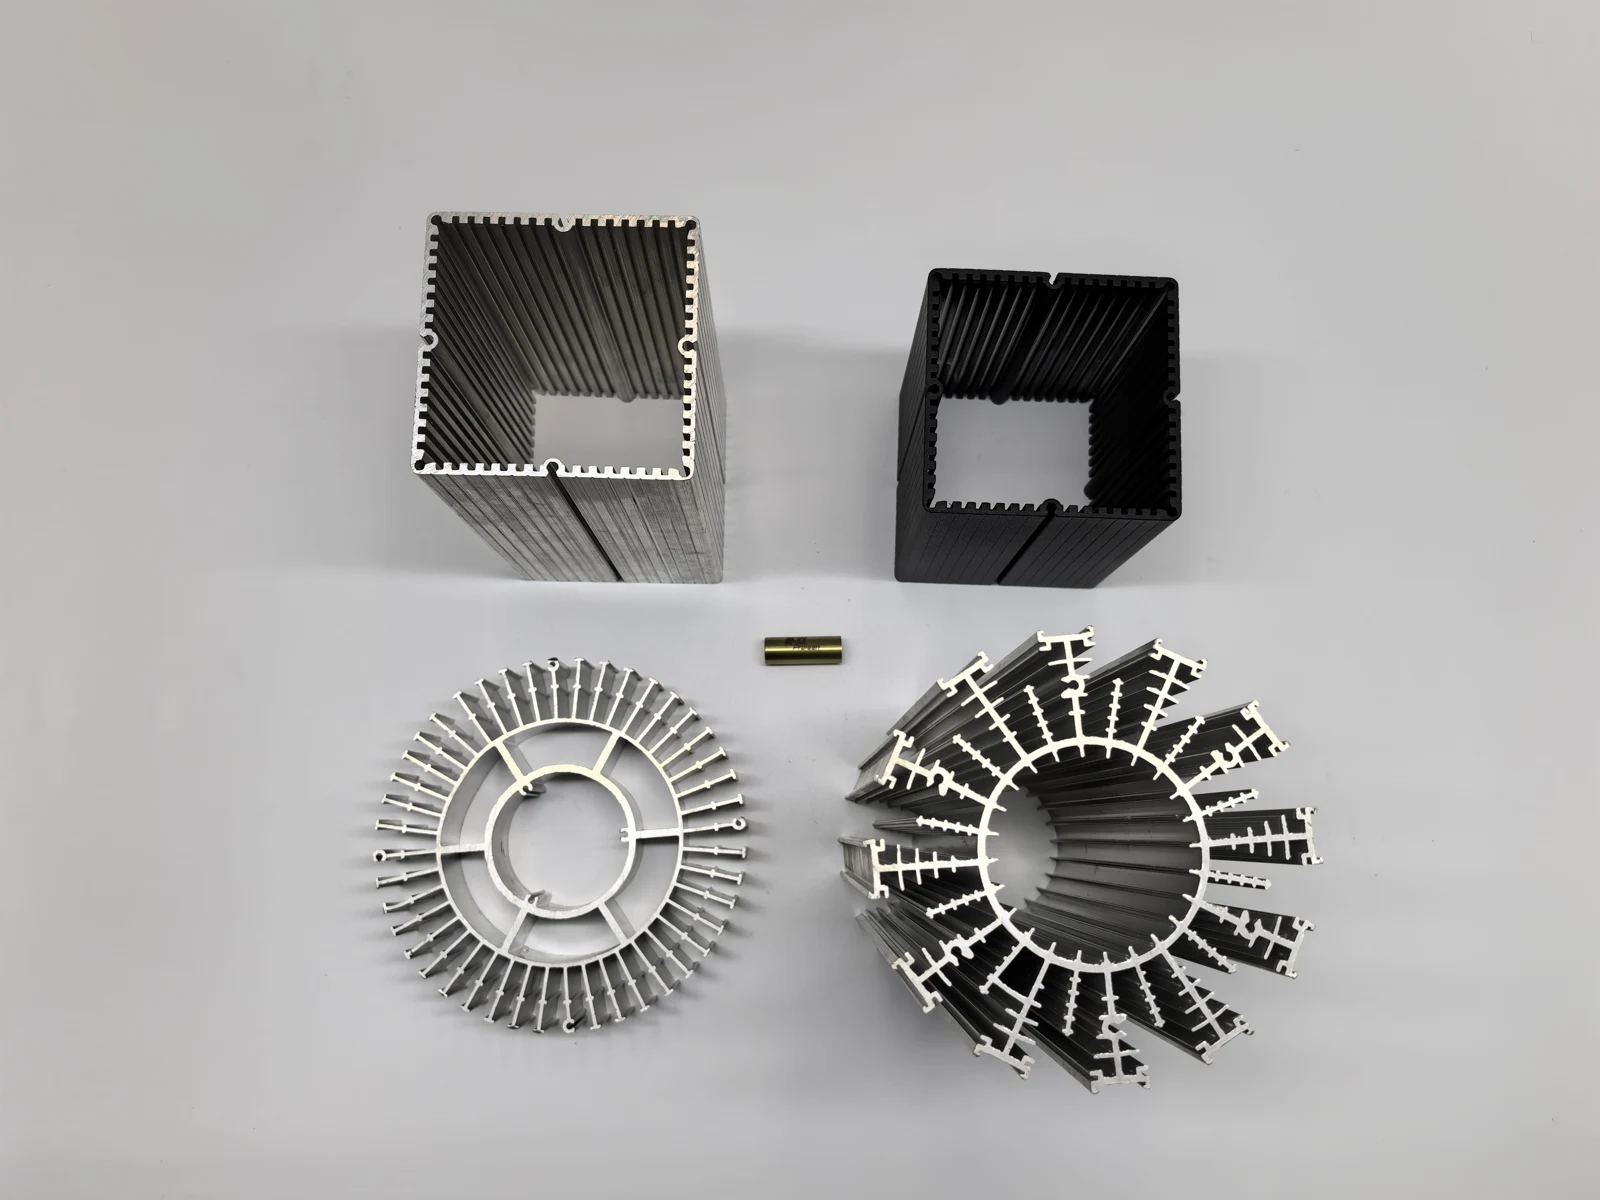
Different sections. A shared manufacturing route.
Review fin spacing, enclosed cavities, mounting channels and surface requirements as a complete profile.
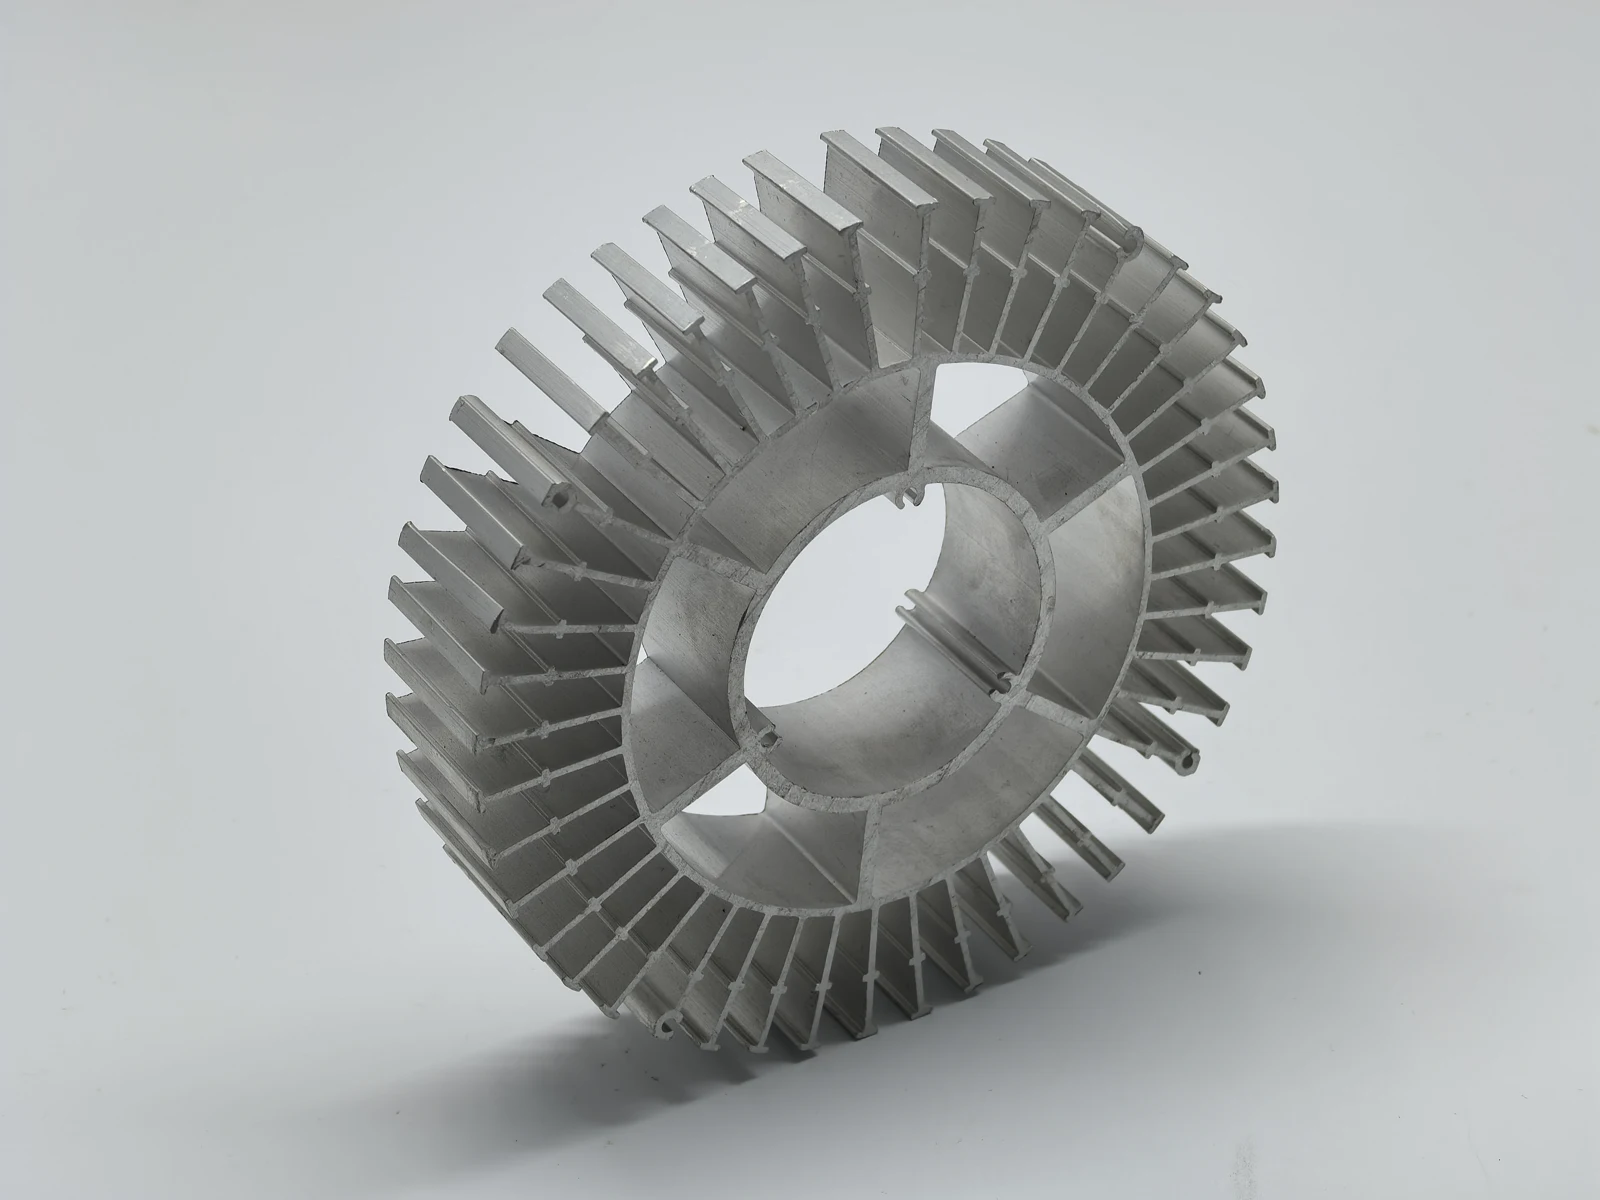
Heat sink extrusion profiles
Fin geometry and any machined contact faces need joint review. Thermal performance depends on the complete application.
Photographs illustrate sample geometry; alloy, dimensions, coating and application performance are confirmed from project documentation.
03 / ALLOY + TEMPER + FINISH
Choose material around
the job it needs to do.
Specify the alloy and temper on your drawing. Profile complexity, mechanical requirements and cosmetic finish all affect the route. Availability and suitability are reviewed with the quote.
6063 aluminum
A candidate for profiles where extrudability and surface appearance matter. Discuss thin sections, visible faces and the required temper.
6061 aluminum
A candidate where mechanical requirements and subsequent machining are priorities. Confirm that the section can be extruded in the specified condition.
Your specified alloy
Send the grade, condition and relevant material standard. Alternative alloys or tempers require engineering approval before substitution.
04 / EXTRUSION DESIGN REVIEW
Resolve the difficult details
before the die is made.
Profile size, alloy, wall distribution and feature relationships determine feasibility. Flag functional requirements so extrusion, straightening, machining and finishing can be planned together.
Wall thickness & fin spacing
Balance section walls and review narrow channels, deep fins and abrupt transitions for die strength and metal flow.
Hollow sections & die features
Review internal cavities, slot openings, corner radii and seam-sensitive features before tooling approval.
Straightness, twist & cut length
State profile length and functional alignment requirements. Define measurement references and inspection expectations.
Critical fits after machining & finishing
Identify the mating faces, bores and hole positions that need machining. Apply final tolerances to the finished condition.
There is no single tolerance for every section. Send the cross-section, alloy, length and critical dimensions for review. Extrusion tolerances and machined-feature tolerances should be specified separately.
05 / PROTOTYPES TO REPEAT ORDERS
Make the production route
part of the conversation.
For prototypes and small runs, tooling cost and material batch requirements can drive the decision. Request a route review before choosing extrusion for a low quantity.
Drawing & quote
Share your section, finished-part model, alloy, quantity and delivery target. Review die needs, secondary operations and inspection scope.
Tooling & first samples
Agree the tooling plan, sample approval criteria and any critical dimensions before approving repeat production.
Fabricate, finish & inspect
Work to the approved revision. Confirm reporting, traceability, protective packing and shipment requirements for your order.
06 / ALUMINUM EXTRUSION FAQ
Start with
clear requirements.
Answers for engineering and purchasing teams.
What do you need for a custom aluminum extrusion quote?
Send a cross-section drawing or DXF, a dimensioned PDF and a STEP model for the finished component when available. Include alloy and temper, cut length, quantity, critical tolerances, finish, inspection needs and target delivery.
Can you include aluminum extrusion cutting and fabrication?
Request cutting, drilling, tapping, milling or other secondary operations in the same RFQ. Define the finished component so profile design, datum selection and machining requirements can be reviewed together.
Can I order prototype or small-run aluminum extrusions?
Ask for a project-specific review. Die cost, profile weight, alloy and batch requirements affect feasibility and price. For early fit checks, discuss whether a machined prototype is a practical first step; it does not validate the extrusion process.
What affects die cost, minimum quantity and lead time?
Section complexity, die construction, alloy, material batch size, cut length, secondary operations, finishing and approval requirements all affect the quotation. Tooling costs, minimum quantities and schedules are confirmed after drawing review.
What finishes are available for extruded aluminum parts?
Discuss anodizing, powder coating and compatible mechanical finishes. Specify cosmetic surfaces, color references and masking. Coating thickness and any final dimensional requirements need to be considered together.
Are these aluminum extrusion or pin-fin heat sink samples?
The photographs show fins that run along the extrusion direction. They are described here as finned extrusion profiles. A discrete pin-fin geometry would require a different or additional manufacturing route.
Where is ProleanTech based?
The existing company information lists a Shenzhen factory in China. Share your destination and required delivery date so packing and shipping can be included in the project review.
LET’S MAKE YOUR NEXT PROFILE
Your cross-section.
A clear next step.
Send your drawing and finished-part requirements.
Let’s review tooling, fabrication and finishing together.
Confidential enquiries · Optional NDA available