
PROTOTYPE & BRIDGE INJECTION MOLDS
Rapid Tooling
Services
Validate your design in the intended thermoplastic. Plan the mold, trial samples and bridge batch around what you need to prove.
USEDesign validation · pilot builds · bridge supply
DEFINETooling + samples + molded batch
RELEASEApprove the revision and acceptance plan
Learn from molded parts.
Before committing to repeat production.
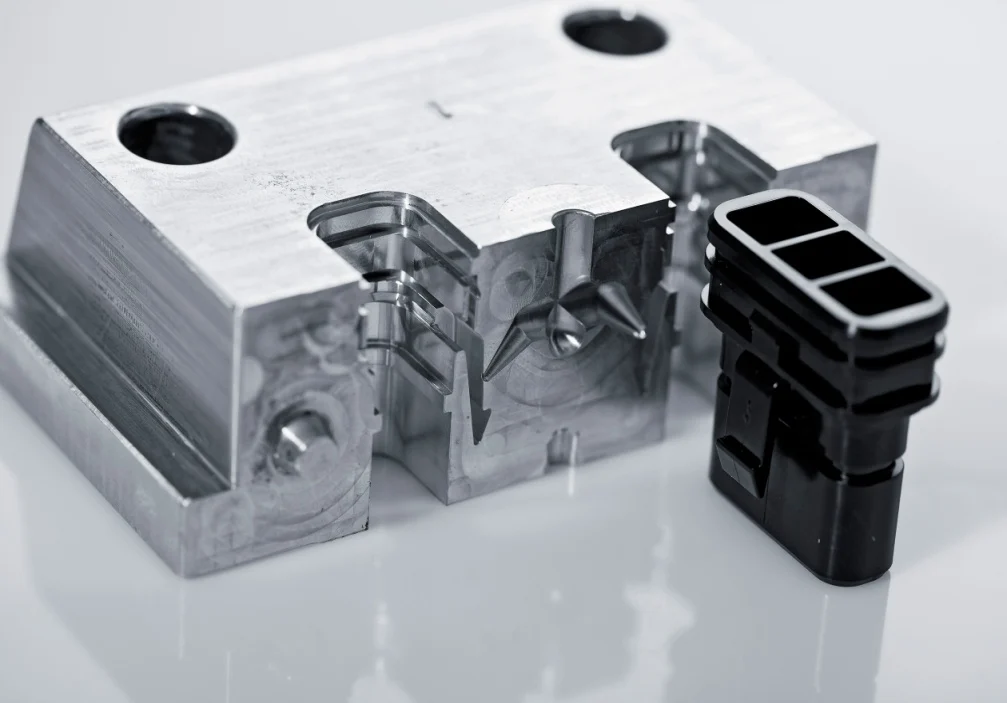
Rapid tooling creates a mold for injection-molded thermoplastic parts when you need more than a visual prototype. Use it to evaluate assembly, molded geometry and material behavior, or to support a defined interim batch. ProleanTech reviews the tool and molding scope against your design maturity, test plan and expected demand.
Resolve the open questions
Check fit, clips, bosses, wall behavior and the intended resin in molded form. Identify which dimensions are frozen and which features may change. Define the tests the samples must support before the tool design is released.
Cover a defined supply gap
Support pilot assembly or an agreed batch while the long-term production route is prepared. Share the quantity, release schedule and likely repeat orders so tool wear, capacity and revision risk can be reviewed together.
A mold is an asset.
A molded part is a deliverable.
Your order should say whether you need tooling with trial parts, tooling with a defined molded batch, or a tool-only delivery subject to a separate compatibility review. Jigs and fixtures used to hold parts are a different service scope.
- Tooling scope
- Mold design and construction, trials, approved changes, ownership and storage terms.
- Part scope
- Resin grade, revision, quantity, gate vestige, appearance, inspection and packaging.
- Transfer scope
- If required: tool documentation, receiving press interface, utilities, handling and requalification.
Choose the mold plan
for the run you actually need.
“Rapid” describes a development route, not one standard mold specification. An aluminum or steel construction, replaceable inserts and a simpler cavity strategy can each suit a project; the right combination depends on the resin, part and test objective.
| Decision | What to specify | Why it matters |
|---|---|---|
| Mold material | Proposed alloy or steel grade, insert strategy and operating conditions | Fillers, heat, local wear and repair needs affect the selection; material alone does not establish tool life. |
| Cavities & feed | Part quantity, cavity count, runner approach and acceptable gate location | A lower initial tool investment may trade against molding labor, runner waste or batch capacity. |
| Moving features | Undercuts, threads, side actions and any permitted manual operations | Simplified tooling can change handling, consistency and part cost. Agree the trade before release. |
| Expected revisions | Features likely to move, alternate inserts and dimensions to adjust after trials | Removing metal is different from adding it. A planned insert can localize a change, but cannot make every revision economical. |
| Texture & appearance | Visible faces, texture reference, parting line and ejector-mark limits | Texture influences draft and release; cosmetic acceptance needs an agreed reference and inspection conditions. |
Tool life, shot allowance, maintenance, repair responsibility and storage are project terms. Confirm them explicitly rather than inferring a guaranteed run from “aluminum,” “steel” or “rapid tooling.”
Use the intended resin.
Define what the trial must prove.
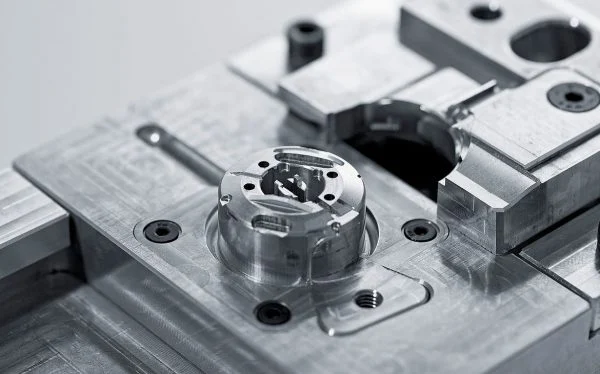
A molded sample can reveal flow, shrinkage, sink, weld lines and ejection behavior that a machined or printed model cannot reproduce. Specify the exact resin, then connect the trial to your product’s functional and dimensional requirements.
Start with a grade, not a family name
ABS, PC, PC/ABS, PP, PE, PA, POM, PET, PMMA and TPU are starting points for a material discussion. Identify manufacturer, grade, filler content, color and any required traceability. High-temperature or demanding grades need a separate feasibility review.
Control the material condition
Drying, permitted regrind, colorant and conditioning can affect results. Agree the material supply responsibility and handling requirements before trials. Customer-supplied resin requires acceptance and sufficient material for setup, samples and the batch.
Match the validation to the application
State load, temperature, chemicals, assembly method and test duration. A successful fit check does not validate long-term creep, sealing, impact or regulatory compliance. Request the material documentation and application testing your project needs.
Make the remaining design risk visible.
Send the current model and controlled drawing together. Mark the features that must stay fixed, the ones open to DFM changes and the interfaces that determine assembly success.
Walls, ribs & bosses
Review thick intersections, abrupt wall changes and local mass for sink and uneven cooling. Relate ribs and bosses to the chosen resin and assembly loads rather than applying one universal wall rule.
Draft & release
Review draw direction, texture depth, tall walls and undercuts. Agree acceptable parting lines and ejector locations. Reduced draft can complicate release and damage appearance.
Gate, flow & venting
Locate gate vestiges away from critical interfaces where practical. Consider weld lines near loaded clips, trapped air and long flow paths. Discuss analysis when flow risk warrants it; a simulation is not sample approval.
Shrinkage & datums
Define critical dimensions, reference datums and measurement condition. Grade, fiber orientation, cooling and moisture can affect dimensions. Tool dimensions and finished-part tolerances are separate requirements.
Approve samples against a plan.
Then release the agreed batch.
The first trial is a decision point. Agree the sample quantity, reports, test responsibility and approval authority before machining begins. Keep mold corrections, process adjustments and design revisions traceable.
- 01
Release the tool design
Approve the part revision, resin, mold concept and agreed DFM deviations. Record gate, parting-line, ejector and cosmetic assumptions. Define planned trials and what is included in the quotation.
- 02
Review the trial output
Identify samples by revision, trial and cavity where applicable. Review fill, flash, short shots, sink, warpage and release marks alongside a dimensional report for the agreed features.
- 03
Test, correct & resample
Evaluate assembly and application performance under the specified conditions. Log deviations and decide whether each needs a process change, mold correction or part redesign. Confirm the scope of another trial.
- 04
Approve the defined release
Record accepted samples, permitted deviations and inspection criteria. Release the approved quantity and revision. A later resin, geometry or process change requires review of the affected acceptance requirements.
Separate the tooling decision
from the price of each part.
Compare the cost of an approved delivered batch, including the learning and changes needed to reach it.
- Initial tooling
- Mold construction, cavities, actions, finish, planned trials and documentation.
- Changes & approval
- Included correction scope, design revisions, additional samples and application testing.
- Molded parts
- Resin and runner usage, molding cycle, setup, handling, trimming, inspection and packaging.
- Ongoing supply
- Repeat setups, tool wear, maintenance, storage, shipping and any eventual replacement tool.
Rapid tooling
questions, answered.
Practical decisions for prototype molds, bridge supply and molded-part validation.
What is rapid tooling for injection molding?
Rapid tooling uses a project-specific mold to produce injection-molded thermoplastic parts for design validation, pilot builds or bridge supply. The mold plan balances the test objective, expected revisions, resin and required run. It is different from printing a model or making a holding fixture.
How does prototype tooling differ from bridge tooling?
Prototype tooling prioritizes learning about the design and molding behavior. Bridge tooling supports an agreed interim supply while the design or long-term production route is finalized. The same mold may serve both purposes if its material, condition, capacity and acceptance scope support the plan.
Should the mold be aluminum or steel?
The choice depends on resin, fillers, operating temperatures, geometry, surface requirements, expected shots and revision strategy. Aluminum is not a universal rapid-tooling requirement, and steel does not automatically make a mold suitable for sustained production. Confirm the proposed grade and construction in the quotation.
Can I validate the actual production resin?
Specify the exact resin manufacturer, grade, filler, color and any documentation requirements. Availability and mold/process compatibility must be confirmed. Samples made in that grade help evaluate molded behavior, but a different gate, cooling layout or cavity count in the eventual production tool can change the result.
Are the mold and molded parts quoted separately?
Ask for separate tooling, trial, modification and molded-part charges, plus inspection and delivery scope. A tooling payment does not by itself define ownership, tool-only shipment, storage, maintenance or transfer rights. Put those terms in the order before work begins.
Can the design change after the mold is made?
Some revisions can be handled by removing metal or replacing a planned insert; others need welding, new components or a new tool. Flag likely changes before design release. Each change needs a feasibility review, cost and schedule agreement, a controlled revision and renewed approval of affected samples.
How many parts can a rapid tool produce, and how long does it take?
There is no single quantity or lead time that applies to every rapid tool. Resin abrasiveness, geometry, mold construction, trial results, maintenance and the required delivery plan all matter. Send trial and batch quantities separately; the quotation confirms the run scope, timing and assumptions.
Can I move directly from approved samples to mass production?
Sample approval releases only the scope you agreed. Before repeat production, review design freeze, demand, cavity strategy, tool condition, process stability, inspection, maintenance and ownership. A production tool with different construction or molding conditions needs its own qualification; prototype approval is not an automatic production release.
YOUR NEXT MOLDING PROJECT
Tell us what
the first batch must prove.
Share your files, test objectives and expected quantities. We’ll review the mold, material, sample and delivery scope for your quotation.
Your files stay confidential. Optional NDA available ↗