Get a Quote →

Materials · PPSU

PPSU CNC Machining Service

Machined polyphenylsulfone — the amber, high-toughness sulfone polymer bought where repeated steam sterilising, impact and heat all have to hold at once, cut to the tolerance, minimum wall and lead time the shop holds.
$$Price band
±0.25mmAchievable · ISO 2768
0.80 mmMinimum wall
3–10 daysPublished lead time
Machined engineering-plastic parts from the Prolean shop gallery

Specifications

PPSU specifications: ±0.25 mm tolerance, 0.80 mm wall, 3 to 10 days lead time

Six numbers a buyer asks for before sending a drawing — the process, the
tolerance we hold, the minimum wall, the largest envelope, the lead time and the price band.

Process
CNC mill · CNC lathe3-axis and 5-axis milling, turning
Achievable tolerance
Not lower than  ±0.25 mm (±0.010"),Based on the drawing, ISO 2768
Minimum wall
0.80 mmVaries with the wall-to-linear-dimension ratio
Maximum part size
200 × 80 × 100 cmLargest envelope quoted online
Lead time
3–10 daysComplex parts sit at the far end
Price band
$$Where PPSU sits against the other 22 materials
Read this first. Process, maximum part size and lead time are
identical on all 23 material pages — they describe the shop, not the material. Tolerance,
minimum wall and price band are the three that change from one material to the next.
This page publishes no grade list, so there is no grade table below — name the
grade you want on the drawing instead.

Machining routes

Machining routes for PPSU: milling, turning, molding and overmolding

Milling and turning are what this page is quoted on. The routes below are the ones the same material takes when the stock form, the volume or the lead time changes — each one is a service page on this site.

CNC millingQuoted here3-axis and 5-axis milling of PPSU plate and block — trays, housings and instrument parts.CNC machining →
CNC turningQuoted hereTurned bushes, sleeves and fittings from PPSU rod and tube.CNC turning →
Injection moldingMolded herePPSU is a molding resin as much as a machined one — the same part moves to a tool once the volume is there.Injection molding →
OvermoldingInsert & overmoldMetal inserts and contacts encapsulated in PPSU — a standard route for parts that are sterilised or handled repeatedly.Overmolding →
Not used for PPSU:EDM, die casting, vacuum casting and grinding. PPSU is an electrical insulator, it is soft enough to load a grinding wheel rather than cut, and the casting routes on this site are metal processes for zinc and aluminium.

Which polymer?

PPSU, PEEK or PEI: choosing a high-temperature polymer

Each answer points at a page on this site that covers it in more depth — a
comparison, a grade guide or a process page.

Will it be steam-sterilised or autoclaved again and again?
That is the question PPSU exists for. It holds its properties through repeated steam cycles — more so than PEI — which is why reusable trays and device parts are specified in it.
Compare with PEI →
Does it have to hold stiffness at the very top of the range?
Then PEEK is the page here published for the hottest service. PPSU trades a little of that for impact toughness, which is the trade it is usually chosen for.
Compare with PEEK →
Is chemical resistance the driver rather than temperature?
The chemical-resistance page sorts the polymers that survive aggressive media; PTFE is the other page here bought purely for chemical inertness.
Read the chemical-resistance guide →
Is the volume moving to a tool?
PPSU is a molding resin as much as a machined one — the same housing can move to a tool once the volume justifies it.
See all 23 materials →
Comparing PPSU with something else?Send the model and the drawing. If the material is still open, the grade call comes back with the price instead of as a separate question.
Get a quote

Machining & tolerance

Tolerancing and inspecting PPSU parts to ISO 2768

The published tolerance on this page is Not lower than  ±0.25 mm (±0.010"),
on the drawing, to ISO 2768. Where a feature needs better than that, say so on the
drawing — that conversation belongs before the tool goes in, not after.

Finishes

Finishing a PPSU part: deburring, blasting and polishing

This is the polymer set of finishes: polishing, blasting, sanding and fine machining. The metal pages list the plating and heat-treatment routes instead.

Applications

Where PPSU parts go: medical, aerospace interiors and electrical housings

  • MedicalReusable trays, instruments and device parts that are sterilised between uses
  • Aerospace interiorsInterior parts selected for low heat release and toughness
  • Electronics housingsHousings and covers that have to take impact and heat
  • AutomotiveUnder-bonnet and repeat-service parts where the same part has to survive both

All of it cut on the same floor —
see CNC machining and
how we hold tolerance.
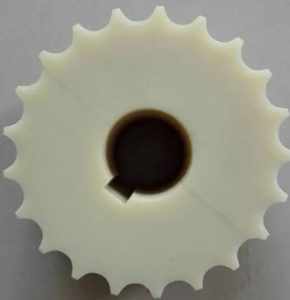
PPSU (polyphenylene sulfone) resin stock and machined components
PPSU resin stock and machined components — shop gallery image.

Further reading

PPSU in context: the sulfone and high-temperature polymers

Deeper reading from around this site — the comparisons, the standards and the
process notes behind this material.

High-temperature setSix chemical resistant plastics for CNC machiningWhich polymers survive aggressive serviceRead →
Material choiceBest plastic for machining: material selection guideHow the engineering polymers are sortedRead →
ThermoplasticsCNC machining of thermoplastics: a comprehensive guideThe family this material belongs toRead →
Other polymerPEEKThe page buyers usually compare PPSU againstRead →
TolerancesNavigating the precision of ISO 2768: a guide to standard tolerancingHow the general-tolerance standard readsRead →
Reading first, or ready to quote?The pages above set out the trade-offs. If the part is already drawn, send it and the quote comes back in one business day on a clean drawing.
Get a quote

FAQ

PPSU machining: grade, sterilising, tolerance and files

Straight answers to the questions that come up most often on a CNC quote —
with the figures published for this material, and a link for each point.

Which PPSU grades can you machine?
This page publishes no grade list, so no grade is named here. PPSU is sold as an unfilled resin and the different suppliers run slightly different melt grades; there is no filled version in common use. Name the grade or the standard on the drawing and it is confirmed in writing.
What tolerance can you hold?
±0.25 mm, on the drawing, to ISO 2768 — the figure published on this page. Where a feature needs tighter than that, mark it on the drawing so it is priced and inspected as a controlled feature.
What is the smallest wall and the largest part?
Minimum wall is 0.80 mm. Maximum envelope is 200 × 80 × 100 cm. Both are shop-wide constants, identical on all 23 material pages.
How fast is a PPSU part?
3 to 10 days, with complex parts at the far end. Post-processing, if you ask for it, is a separate step and adds to that window.
Which finish should I ask for?
The cards in the finishes section above are the polymer set — polishing, bead blasting and as-machined / deburring among them. The full list of 20 is at surface finishes.
What files should I send?
STEP, STP, IGES, IGS, SLDPRT, STL, DXF, DWG, PDF, DOCX, JPG, JPEG, PNG or ZIP. A 2D PDF plus the model is the combination that gets quoted fastest.
Is my drawing kept confidential?
Uploads stay with the people quoting and making the part. If you need a mutual NDA in place first, say so on the contact form and it is arranged before files change hands.

Next step

Send the drawing — we come back with the material call and the price

Upload the model and the 2D PDF. You get a manufacturability note, a note on the resin if the drawing leaves it open, and a price.

All uploads are secure and confidential.

  • Quoted in 1 business day on a clean drawing
  • The resin and fill stated in writing on the quote
  • First article inspected before the run