Get a Quote →

Materials · Garolite G-10

Garolite G-10 CNC Machining Service

Machined G-10 fibreglass-epoxy laminate — the woven-glass composite selected where electrical insulation and dimensional stability both matter, with the tolerance, minimum wall and lead time the shop holds.
$$$Price band
±0.125mmAchievable · ISO 2768
0.80 mmMinimum wall
3–10 daysPublished lead time
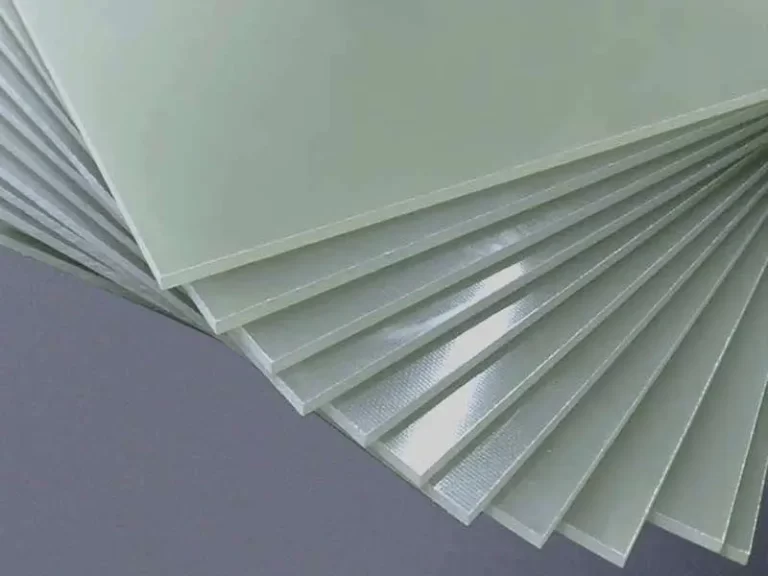
Stack of G10 FR4 fibreglass sheets used in machining applications

Specifications

G-10 specifications: ±0.125 mm tolerance, 0.80 mm wall, 3 to 10 days lead time

Six numbers a buyer asks for before sending a drawing — the process, the
tolerance we hold, the minimum wall, the largest envelope, the lead time and the price band.

Process
CNC mill · CNC lathe3-axis and 5-axis milling, turning
Achievable tolerance
Not lower than ±0.125mm (±0.005″)Based on the drawing, ISO 2768
Minimum wall
0.80 mmVaries with the wall-to-linear-dimension ratio
Maximum part size
200 × 80 × 100 cmLargest envelope quoted online
Lead time
3–10 daysComplex parts sit at the far end
Price band
$$$Where Garolite G-10 sits against the other 22 materials
Read this first. Process, maximum part size and lead time are
identical on all 23 material pages — they describe the shop, not the material. Tolerance,
minimum wall and price band are the three that change from one material to the next.
This page publishes no grade list, so there is no grade table below — name the
grade you want on the drawing instead.

Machining routes

Machining routes for G-10: milling, turning, waterjet cutting and grinding

Milling and turning are what this page is quoted on. The routes below are the ones the same material takes when the stock form, the volume or the lead time changes — each one is a service page on this site.

CNC millingQuoted here3-axis and 5-axis milling of G-10 sheet — profiles, pockets, cut-outs and drilled patterns.CNC machining →
CNC turningQuoted hereSleeves, bushes and rod parts from G-10 tube and rod stock.CNC turning →
Waterjet cuttingSheet stockThe right way to blank a laminate: an abrasive jet cuts without the heat that chars the epoxy.Waterjet cutting →
GrindingFinishing passSurface grinding to bring sheet thickness and cut edges into a tighter band. The grinding page covers composites as well as metals.Grinding →
Not used for Garolite G-10:Injection molding, die casting, vacuum casting and EDM. G-10 is a cured thermoset glass-epoxy laminate — it cannot be melted and re-formed — and the resin is an electrical insulator.

Which polymer?

G-10, FR-4 or PEEK: choosing by insulation, heat and strength

Each answer points at a page on this site that covers it in more depth — a
comparison, a grade guide or a process page.

Is it an insulator that also has to carry load?
G-10 and FR-4 are the two laminate pages on this site. G-10 is the general-purpose grade; FR-4 is the same glass weave with a flame-retardant resin system, and it has its own page here.
Compare with FR-4 →
Does it have to survive a high-temperature process or a cleanroom bake?
Then the high-temperature polymers are the comparison — PEEK and PEI are both published on this site, and both hold their dimensions far above where a laminate resin does.
Compare with PEEK →
Is it for electrical equipment rather than a structural part?
Then the comparison is with the unfilled engineering polymers: PPS and PPSU are the two pages here bought for electrical and high-temperature service.
Compare with PPS →
Jigs and fixtures rather than a product part?
That is the other job G-10 does — tooling plate and fixture stock. The design guide covers how the fixture is specified before it is cut.
See all 23 materials →
Comparing Garolite G-10 with something else?Send the model and the drawing. If the material is still open, the grade call comes back with the price instead of as a separate question.
Get a quote

Machining & tolerance

Tolerancing and inspecting G-10 parts to ISO 2768

The published tolerance on this page is Not lower than ±0.125mm (±0.005″)
on the drawing, to ISO 2768. Where a feature needs better than that, say so on the
drawing — that conversation belongs before the tool goes in, not after.

Finishes

Finishing a G-10 part: sanding, blasting and deburring

This is the polymer set of finishes: polishing, blasting, sanding and fine machining. The metal pages list the plating and heat-treatment routes instead.

Applications

Where G-10 parts go: switchgear, fixtures and engine mountings

  • Electrical boards & switchgearInsulating boards and components where the part also carries load
  • Jigs & fixturesTooling plate, fixture stock and wear pads
  • Engine mountingsMountings and spacers selected for dimensional stability
  • Precision insulating partsParts where low thermal expansion and no water uptake both matter

All of it cut on the same floor —
see CNC machining and
how we hold tolerance.
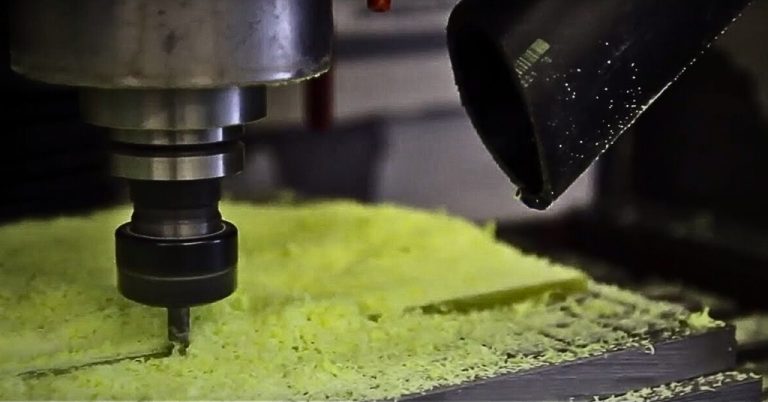
A CNC end mill cutting a stack of G10 FR4 fibreglass-epoxy laminate sheets
G-10 laminate on the machine table, as cut — shop gallery image.

Further reading

G-10 in context: the laminate family, machinability and tolerances

Deeper reading from around this site — the comparisons, the standards and the
process notes behind this material.

Composite familyCNC machining of thermoplastics: a comprehensive guideHow the composite laminates sit against the thermoplasticsRead →
Material choiceCommon materials for CNC machiningWhere the laminates sit next to the metals and the plasticsRead →
MachinabilityMachinability of material and its relation with CNC machiningWhat the cutting data is really telling youRead →
TolerancesNavigating the precision of ISO 2768: a guide to standard tolerancingHow the general-tolerance standard readsRead →
Other laminateFR-4 machining serviceThe flame-retardant sibling of the same glass weaveRead →
Reading first, or ready to quote?The pages above set out the trade-offs. If the part is already drawn, send it and the quote comes back in one business day on a clean drawing.
Get a quote

FAQ

G-10 machining: sheet stock, tolerance, lead time and files

Straight answers to the questions that come up most often on a CNC quote —
with the figures published for this material, and a link for each point.

Which grade of G-10 can you machine?
This page publishes no grade list, so no grade is named here — G-10 is a laminate designation rather than a resin grade, and the weave and resin system are set by the sheet supplier. Send the sheet specification with the drawing and it is confirmed in writing.
What tolerance can you hold?
±0.125 mm, on the drawing, to ISO 2768 — the figure published on this page. Where a feature needs tighter than that, mark it on the drawing so it is priced and inspected as a controlled feature.
What is the smallest wall and the largest part?
Minimum wall is 0.80 mm. Maximum envelope is 200 × 80 × 100 cm. Both are shop-wide constants, identical on all 23 material pages.
How fast is a G-10 part?
3 to 10 days, with complex parts at the far end. Post-processing, if you ask for it, is a separate step and adds to that window.
Which finish should I ask for?
The cards in the finishes section above are the polymer set — polishing, bead blasting and as-machined / deburring among them. The full list of 20 is at surface finishes.
What files should I send?
STEP, STP, IGES, IGS, SLDPRT, STL, DXF, DWG, PDF, DOCX, JPG, JPEG, PNG or ZIP. A 2D PDF plus the model is the combination that gets quoted fastest.
Is my drawing kept confidential?
Uploads stay with the people quoting and making the part. If you need a mutual NDA in place first, say so on the contact form and it is arranged before files change hands.

Next step

Send the drawing — we come back with the material call and the price

Upload the model and the 2D PDF. You get a manufacturability note, a note on the resin if the drawing leaves it open, and a price.

All uploads are secure and confidential.

  • Quoted in 1 business day on a clean drawing
  • The resin and fill stated in writing on the quote
  • First article inspected before the run