
CUSTOM ALUMINUM PARTS · TOOLING TO PRODUCTION
Aluminum Die
Casting Services
Lighter parts. Integrated features.
Built around your application.
Source custom aluminum alloy castings with ProleanTech. Bring tooling, CNC post-machining, surface finishing and inspection into one drawing-led manufacturing plan.
Share CAD + a dimensioned drawing. Optional NDA available →
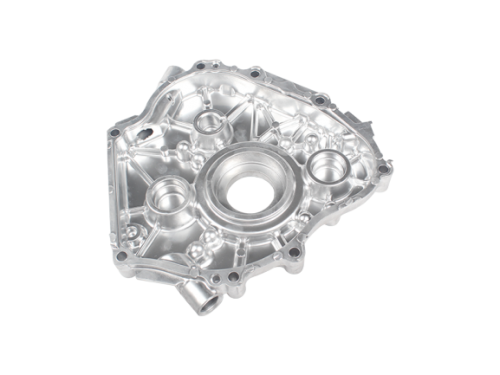
From tooling to finished partDFM · die casting · machining · finishing
Alloy matched to the applicationWeight, loading, environment and finish
Approve before productionDrawing revision · samples · inspection plan
Is aluminum die casting right for your part?
Aluminum high-pressure die casting injects molten alloy into a reusable steel die, typically using a cold-chamber process. It suits repeat production of complex metal parts when the design and demand justify dedicated tooling.
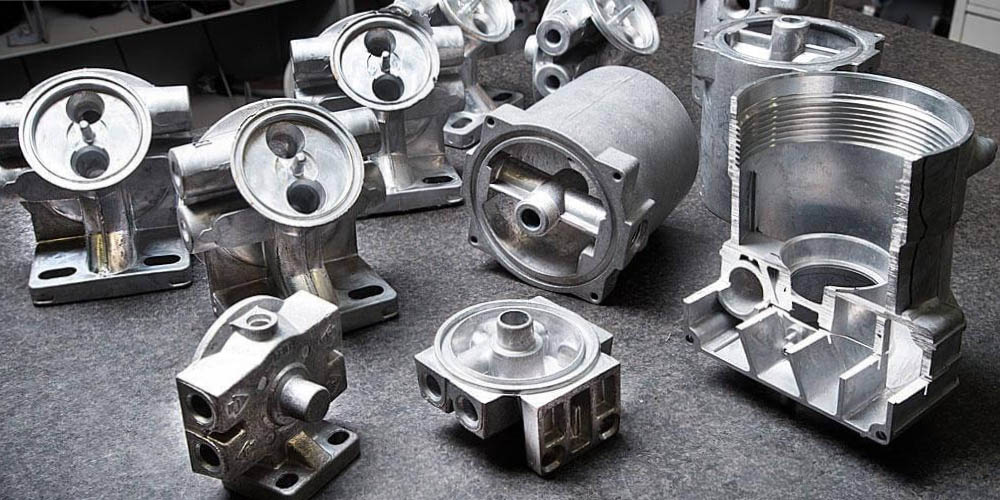
Housings, covers & enclosures
Combine ribs, bosses and mounting features in a near-net-shape part. Define connector openings, assembly interfaces and visible surfaces early.
Thermal & electrical equipment
Consider aluminum for heat-transfer components and equipment housings. Thermal performance depends on the selected alloy, geometry, surface treatment and assembly, not the material name alone.
Industrial & automotive components
Review brackets, motor or gearbox housings against load cases, fatigue, temperature and exposure. Safety-critical parts need a specific validation and documentation plan.
Stable design and repeat demand are the starting point.
For a few prototypes or frequent revisions, CNC machining may avoid early tool investment. For fine detail in smaller, heavier parts, compare zinc die casting. Casting-route selection should also account for ductility, internal soundness and heat-treatment needs.
Choose an alloy. Define its acceptance.
A380 and ADC12 are useful starting points for discussion, not interchangeable default specifications. Send the alloy standard and application requirements; availability and process suitability are confirmed at quotation.
| Alloy candidate | Why consider it | What to review |
|---|---|---|
| A380 | Common general-purpose aluminum die casting alloy, balancing castability, strength and machinability. | Loads, exposure, machining allowance and required finish. |
| ADC12 / A383 family | Frequently considered for complex die filling and detailed casting geometry. | ADC12 and A383 are separate specifications. Approve exact chemistry and any substitution. |
| A360 | Candidate where corrosion resistance and pressure-tightness requirements influence selection. | Casting conditions, sealing design and the actual leak-test requirement. |
| A413 / B390 | A413 for fluidity-focused designs; B390 for selected wear-resistant applications. | These serve different needs. Confirm grade, machinability, tooling and required properties. |
6061 and 7075 are not default HPDC alloys.
If your drawing specifies a wrought alloy or temper, review the manufacturing route before substituting a casting alloy. Mechanical properties, corrosion behavior and qualification requirements can change.
Need aluminum casting engineering consultation? Share loads, service temperature, target weight and finish.
Resolve the risks before cutting steel.
A useful DFM review connects geometry to tool design, filling, solidification, ejection and secondary operations. It should produce clear actions on the same drawing revision.
Walls, ribs & local thick sections
Favor consistent sections with gradual transitions and fillets. Thick bosses and abrupt changes can create shrinkage hot spots; thin or long flow paths can be difficult to fill. Minimum wall thickness is part-specific.
Draft, parting line & ejection
Agree the pull direction, draft, sliders and ejector locations. Mark cosmetic faces and surfaces where flash, gate trimming or witness marks would affect use.
Datums, fits & machining stock
Separate as-cast dimensions from machined tolerances. Define functional datums, bore fits, flatness and threads; allow access for workholding, cutting tools and inspection.
Porosity & sealing interfaces
Machining may expose internal pores. Identify pressure boundaries, gasket lands and threaded fluid ports before tooling. Specify test medium, pressure, duration and allowable leakage.
Have a design ready? Include the requirements that affect fit, function and acceptance.
Cast the geometry. Machine the interfaces.
A complete aluminum die casting service includes the operations needed to turn a casting into an accepted component. Confirm machining and finish requirements together, before the tool is finalized.
CNC post-machining
Machine precision bores, datum faces, threads, mounting patterns and sealing grooves where casting alone cannot meet the drawing. Review stock allowance and the risk of opening pores.
Trimming & deburring
Remove gates, runners and flash, and define safe edge conditions. Agree whether visible trim or ejector marks are acceptable on each surface.
Assembly-ready details
State insert, fastener and mating requirements. Where multiple operations affect the same interface, define inspection after the final relevant operation.
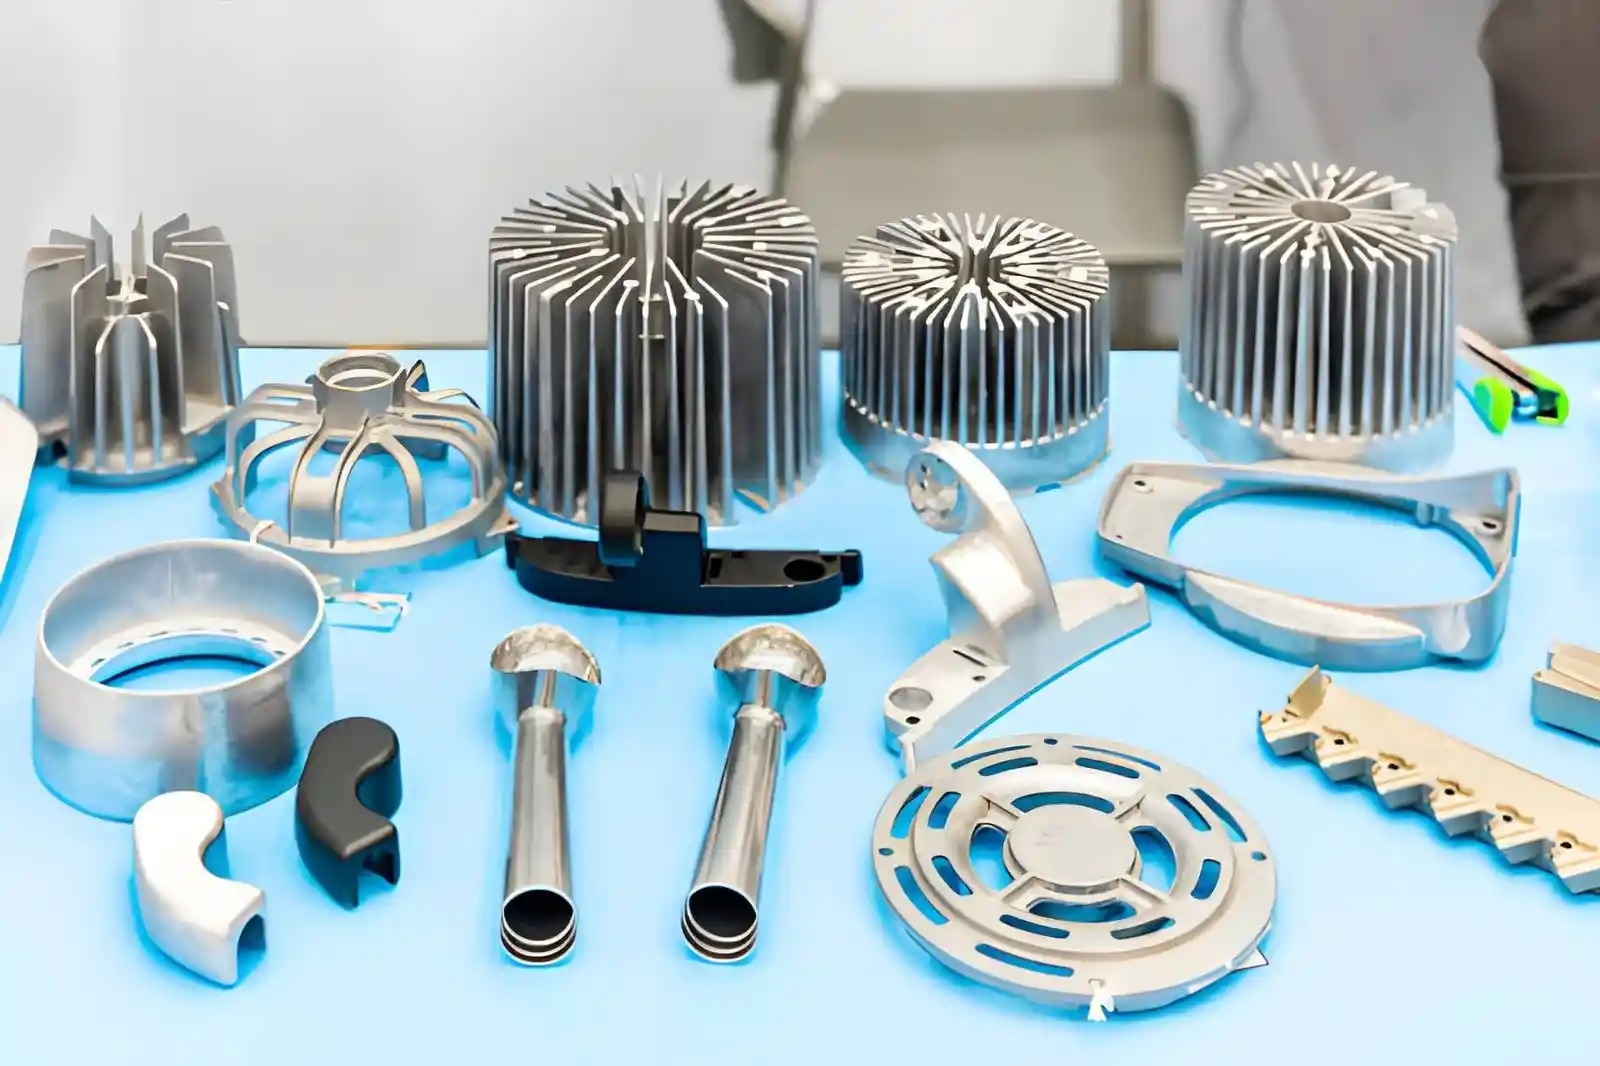
Choose the finish for the environment and the interface.
| Finish route | Useful for | Before approval |
|---|---|---|
| Bead blasting / mechanical finish | Texture control and surface preparation. | Cosmetic sample, roughness requirement and masking of fits. |
| Powder coating / paint | Color and a specified protective coating system. | Pretreatment, coating thickness, adhesion, masking and exposure tests. |
| Conversion coating | Specified corrosion protection or preparation for paint. | Exact chemistry or standard, electrical-contact areas and compliance requirements. |
| Anodizing | Selected applications after alloy and appearance review. | High-silicon die cast alloys may produce a dark or uneven appearance. Approve samples; do not expect a 6061-like cosmetic result. |
Define thread masking, coating buildup, sealing faces and final dimensional inspection. Explore surface finishing services →
Make quality measurable before production.
Agree the drawing, inspection scope and acceptance criteria before releasing tooling. A visual check alone cannot establish internal soundness, alloy chemistry or leak tightness.
Know what is being cast.
Specify alloy standard, approved substitutions and the material records needed with delivery. Agree batch identification and traceability where the program requires them.
Inspect what controls function.
Define critical characteristics, measurement method and sampling. Distinguish casting tolerances from machined tolerances; agree the applicable casting standard or drawing limits.
Test the relevant failure mode.
For sealing or internal integrity, request a project-specific leak or radiographic inspection plan. Confirm capability, scope and reporting in the quotation.
Approve first samples against the agreed requirements.
Review dimensional results, assembly fit, cosmetic samples and any agreed functional tests. Resolve deviations before batch release. For automotive or regulated programs, specify PPAP, FAI, compliance or sector documentation requirements upfront.
Understand the tooling, timing and total cost.
Compare quotations on the same scope: tooling, approved samples, finished parts, inspection and delivery. Unit casting price alone does not describe the total program cost.
- 01 / REVIEW
Confirm the manufacturing plan
Review CAD, alloy, quantities and acceptance requirements. Agree DFM actions, cavity count, slides, secondary operations and tooling scope.
- 02 / TOOL & SAMPLE
Validate before release
Manufacture the agreed tooling, run trials and assess samples. Include time for sample feedback and any tooling changes before production approval.
- 03 / PRODUCE & DELIVER
Repeat the approved revision
Release the batch against the approved drawing and inspection plan. Confirm packaging, shipping terms and the requirements for repeat orders.
| Cost or schedule driver | What to clarify |
|---|---|
| Tooling investment | Tool ownership, cavity count, tool life assumptions, maintenance, storage and modification responsibility. |
| Finished part cost | Alloy, shot weight, quantity breaks, trimming, machining, coating, inspection and packaging. |
| Lead time | Separate tooling, sampling, sample revisions, production and transit. Timing starts from the agreed approval milestone. |
| Program volume | Quote the initial order and annual demand. There is no universal MOQ or break-even quantity for every geometry. |
Ask for a quote that separates tooling, samples and production.
Aluminum die casting FAQs.
Practical answers for purchasing, engineering and supplier evaluation.
What aluminum die casting services does ProleanTech offer?
The service covers custom aluminum castings with tooling review, CNC post-machining and surface finishing. Share the drawing, alloy, quantities and acceptance requirements so the manufacturing scope can be confirmed in your quotation.
Which aluminum alloy should I specify?
A380 is a common starting point for general-purpose HPDC; ADC12 or A383 may be considered for detailed castings, and A360 for selected corrosion or pressure-related needs. Specify the exact grade and standard. Similar grades must not be substituted without approval.
What tolerances and wall thickness can you achieve?
Both depend on the feature size, geometry, die design, alloy and process. Provide a dimensioned drawing with datums and critical features. The quote should separate achievable as-cast tolerances from features requiring secondary machining; a general CNC tolerance is not a blanket casting tolerance.
Can aluminum die cast parts be pressure-tight?
They can be developed for sealing applications, but porosity and machining exposure must be considered. Define the pressure boundary, medium, test pressure, duration and allowable leakage. Approve the proposed casting and inspection route before production.
Can die cast aluminum be anodized or heat treated?
Both require alloy and process review. Anodizing high-silicon die cast alloys can give uneven cosmetic results. Conventional HPDC can contain entrapped gas that causes blistering during solution heat treatment, so do not assume a T6 route is available for every casting.
Is die casting cost-effective for low quantities?
Dedicated tooling can dominate the first-order cost. Compare the total cost over forecast demand, including machining and finishing. For small quantities or changing designs, machining or a prototype casting route may be a better starting point.
What is the lead time for tooling and aluminum parts?
Timing depends on tool complexity, sample iterations, quantity, machining, finish and inspection. Request separate tooling, sample and production schedules tied to approval milestones. A repeat order using approved tooling differs from a new-tool project.
What files do I need for an aluminum die casting quote?
Send 3D CAD and a dimensioned PDF, alloy or application requirements, initial and annual quantities, finish, critical dimensions, required inspection documents and target date. For an existing tool, include its condition, ownership and available drawings.
START WITH YOUR DRAWING
Let’s review your
next aluminum part.
Bring your geometry, demand and acceptance requirements. We’ll use them to review alloy selection, tooling, machining and finishing for quotation.
Optional NDA available · Confidential project enquiries.
For a more complete quote
- 3D CAD + dimensioned PDF
- Alloy / standard or application needs
- Initial order + annual demand
- Finish, critical fits + sealing needs
- Inspection records + target date
- Existing tooling details, if applicable