
APPLICATION / INDUSTRIAL EQUIPMENT
Industrial equipment & energyIndustrial equipment parts.
Spares, tooling and wear parts manufactured on demand.
Replacement spares, jigs, tooling and wear parts for production equipment, made to a drawing or from a sample when the original is no longer supported. One-off or repeat batches, in the material and hardness you specify.
- TYPICAL PARTS
- Spares, jigs and fixtures, wear plates, tooling bodies
- PRIMARY ROUTE
- CNC machining, sheet metal fabrication, heat treatment
- COMMON MATERIALS
- Alloy steel, stainless steel, cast iron, brass, aluminium
SPECIFICATION
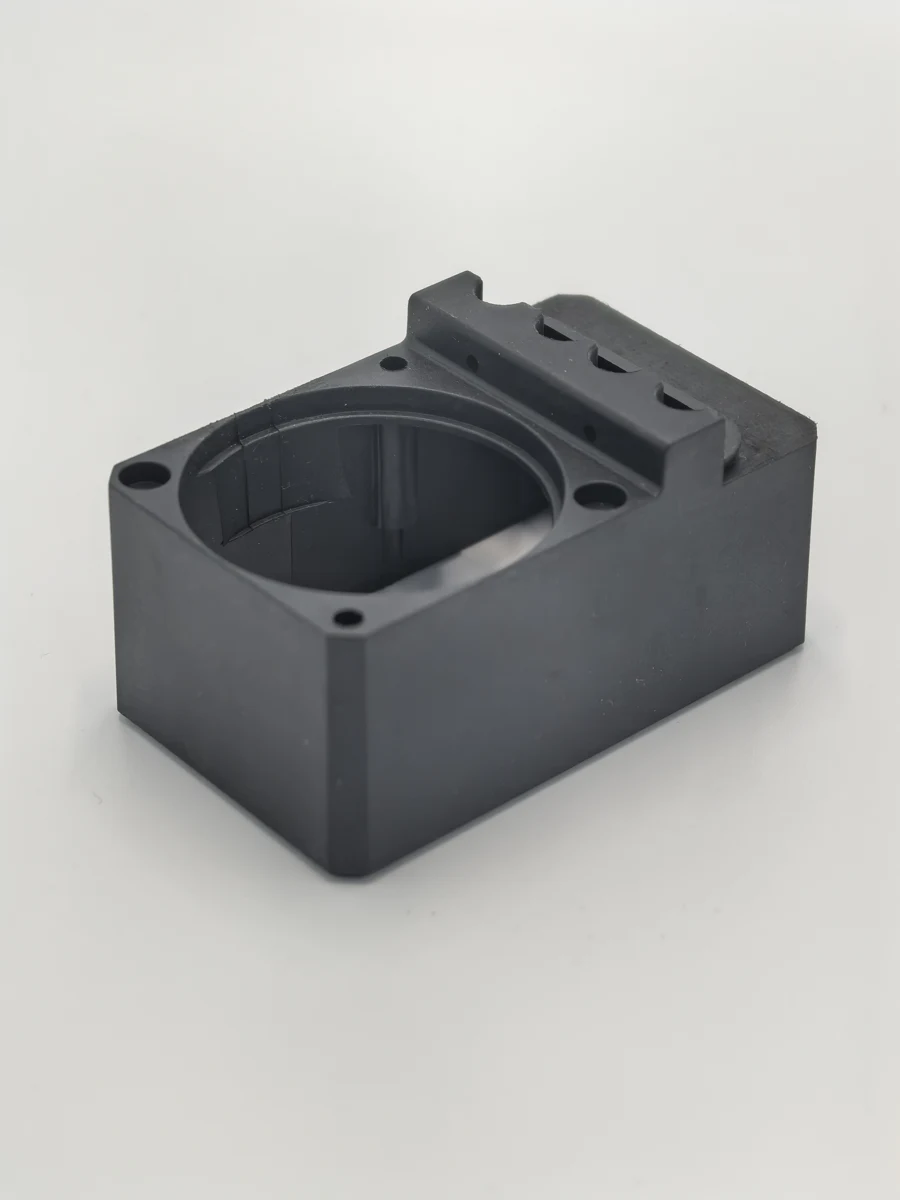
APPLICATION REQUIREMENTS
What decides the design here.
Four things shape the route before a tool is selected. If any of them is unknown at enquiry, we say so instead of assuming a default.
Read the design guideOperating conditions
Temperature, load, abrasion and what the part contacts. These decide the material and the hardness.
Drawing, sample or part number
Which of the three you have. The route and the confidence in fit depend on it.
Corrosion and environment
Exposure to coolant, washdown, weather or chemicals, and the coating that has to survive it.
Interchangeability
Whether the part must drop into an existing assembly without adjustment, and the dimensions that guarantee that.
PARTS WE MAKE
Parts for this application,
and the geometry that shapes them.
Workshop photographs of real geometry. Each one carries the route, what the machine has to reach, what is checked, and what you need to state on the drawing.
See more part geometry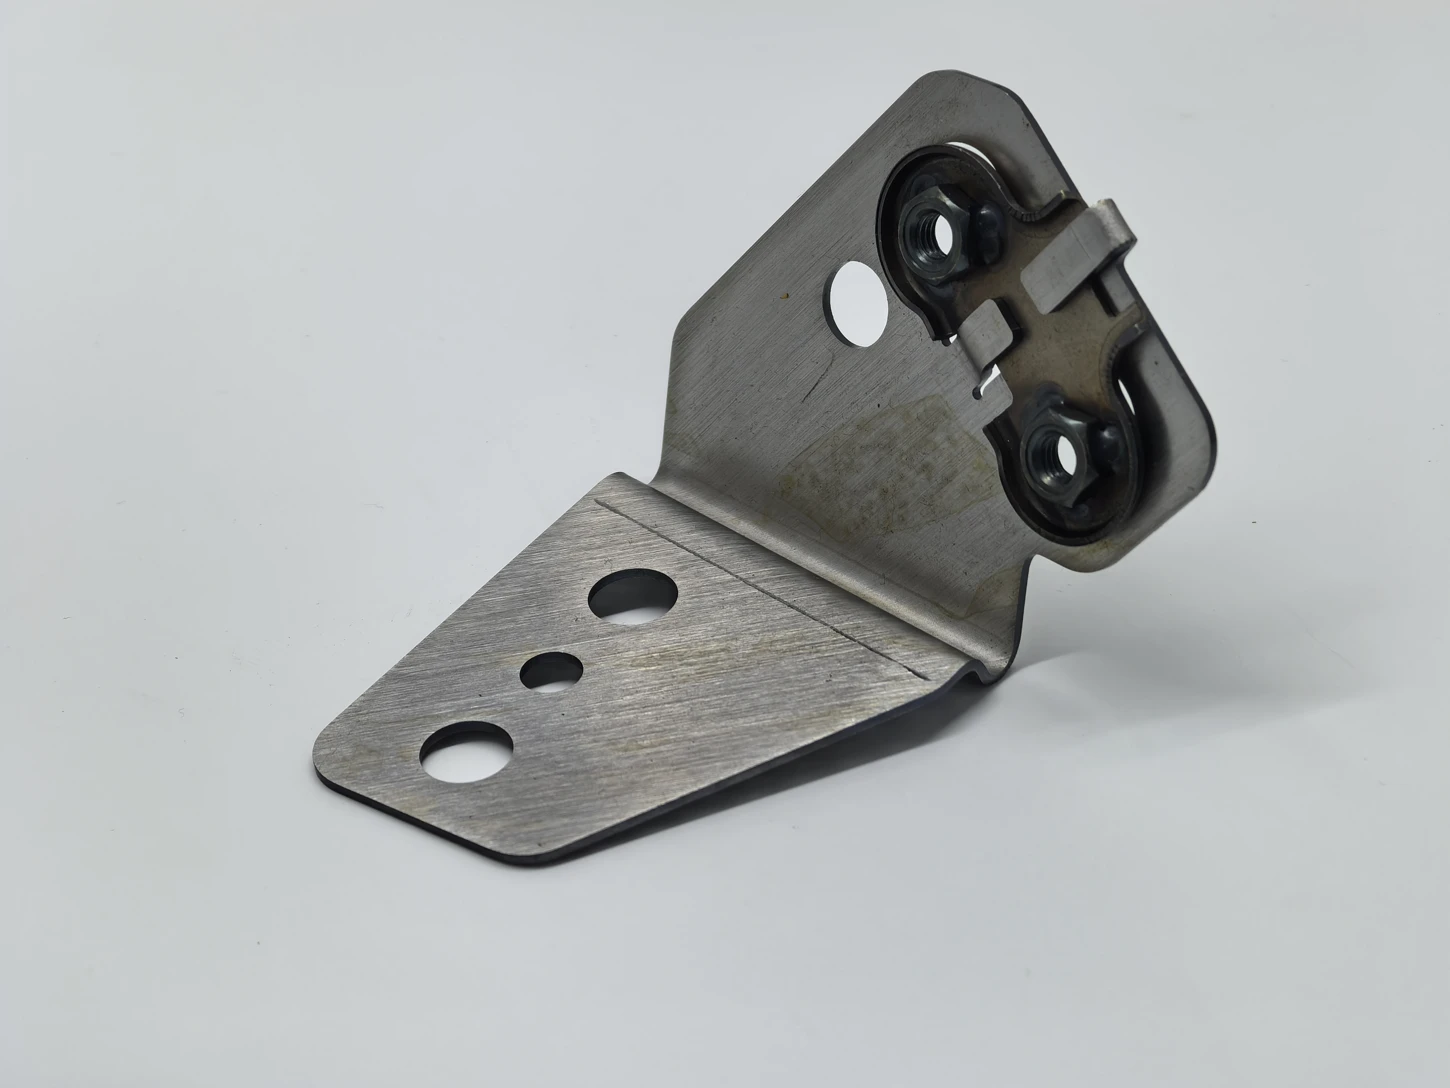
Formed guard bracket
Bend radius, hole position after forming and how the bracket meets the frame. A guard has to stay rigid after it is formed, so the material condition matters as much as the gauge.
State the bend allowance, the hole-to-bend distance and the coating requirement.
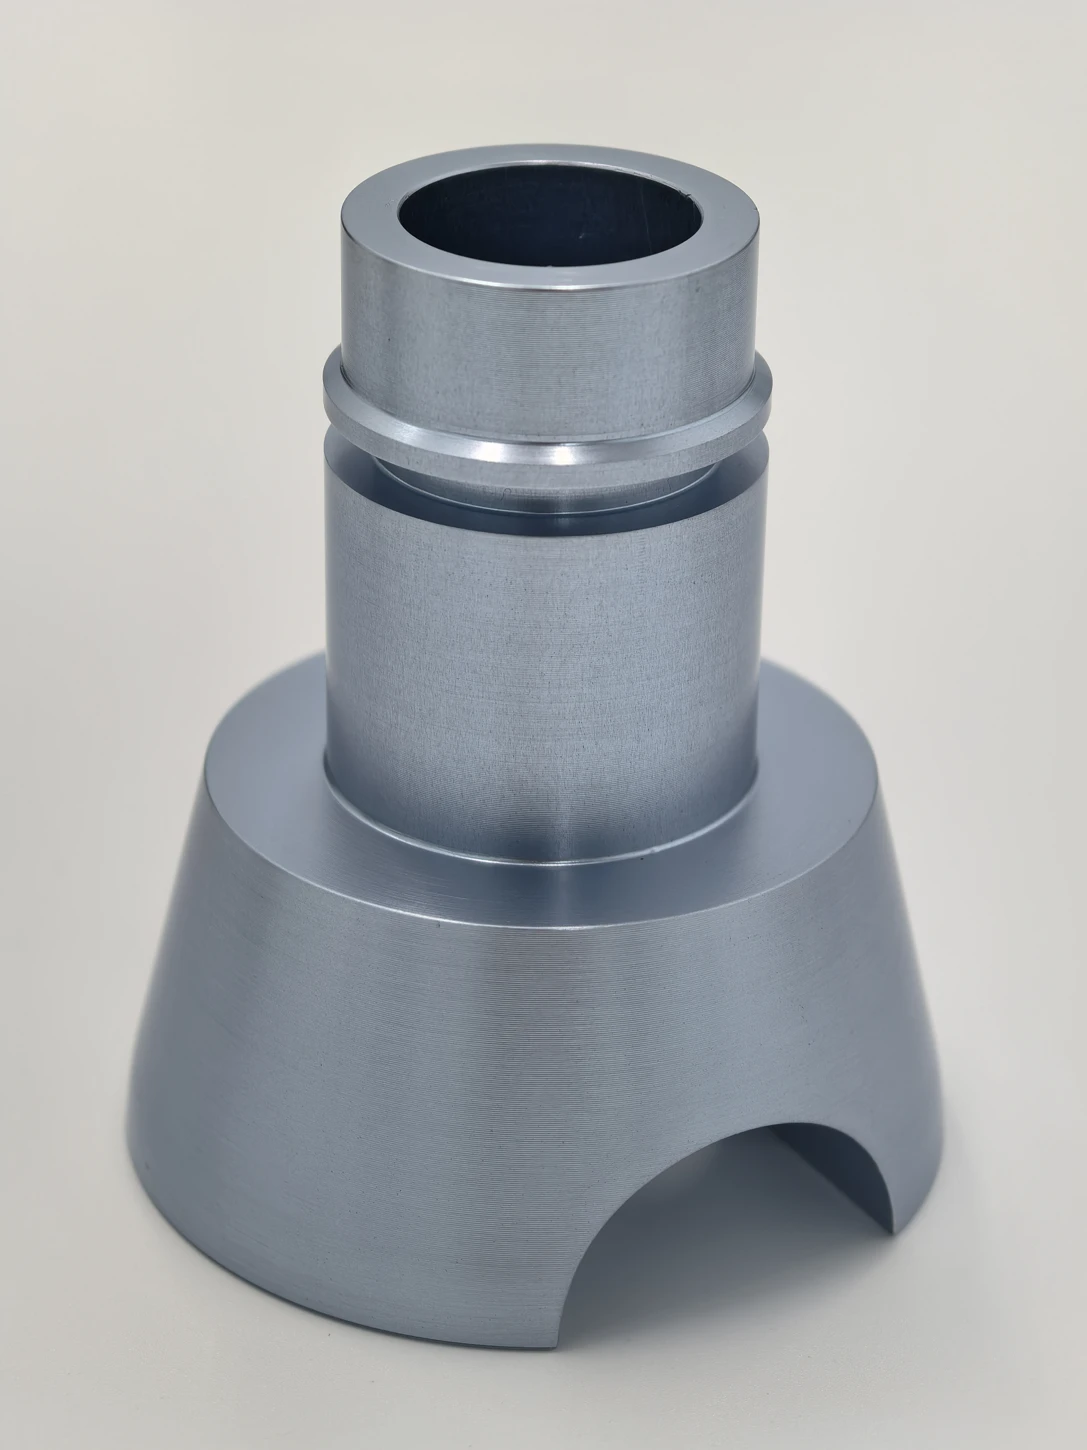
Turned wear bush
Bore size, wall section and the surface that runs against the shaft. Hardness and bore tolerance are chosen together: heat treatment moves the bore.
Call out the bore tolerance, the running surface finish and the hardness.
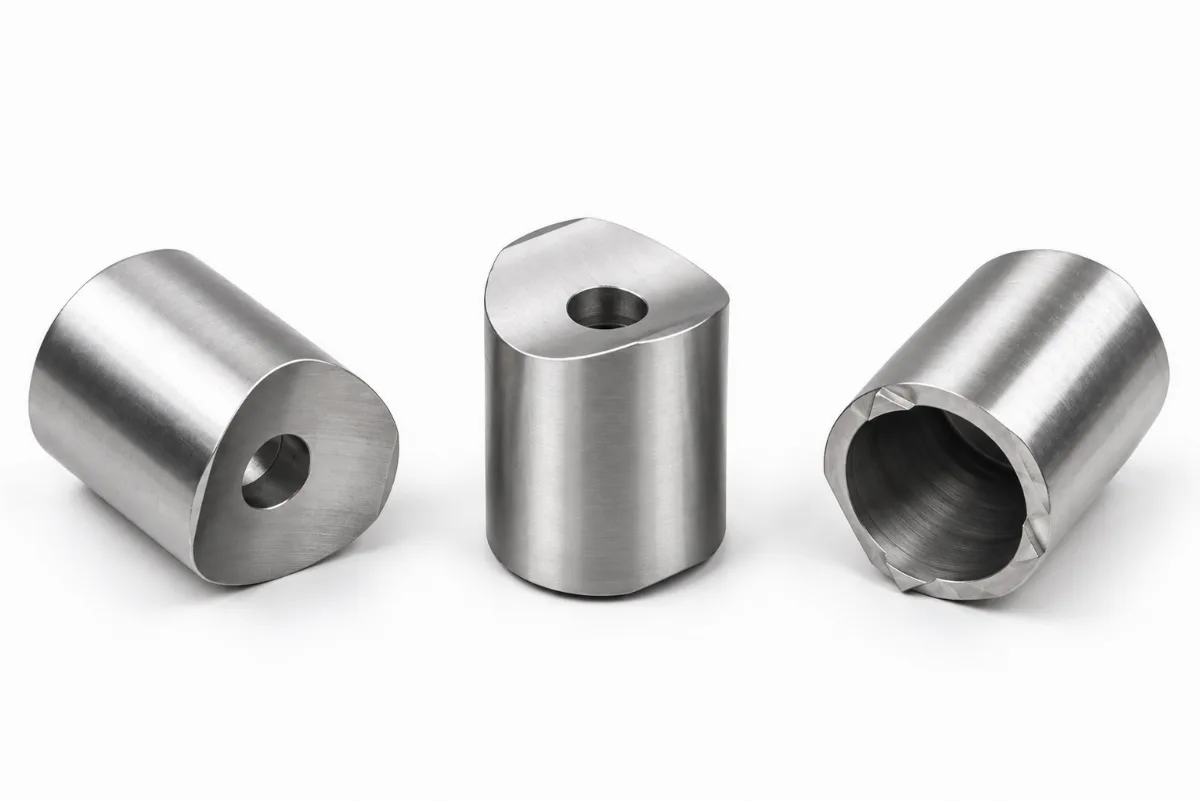
Cylindrical, knurled and formed spares
Diameters, knurl pitch and formed ends on a batch of mixed spares. Repeat orders are made to the same drawing revision so a replacement fits without fitting.
Give the drawing revision, the quantity per size and the hardness where it applies.
PROCESSES, MATERIALS AND FINISHES
The routes used for these parts.
Not every route suits every part. These are the ones that come up most for this application; the quote states the route chosen for your geometry and quantity.
All capabilitiesFINISHES AND TREATMENT
Finishing changes dimensions: coating thickness, masking and any effect on a mating fit are agreed before the route is fixed, not discovered at inspection.
INSPECTION AND DOCUMENTATION
What we measure, and what we record.
The inspection scope is agreed with the order. Anything you need recorded has to be stated before machining starts, because it cannot be reconstructed afterwards.
Tolerancing standards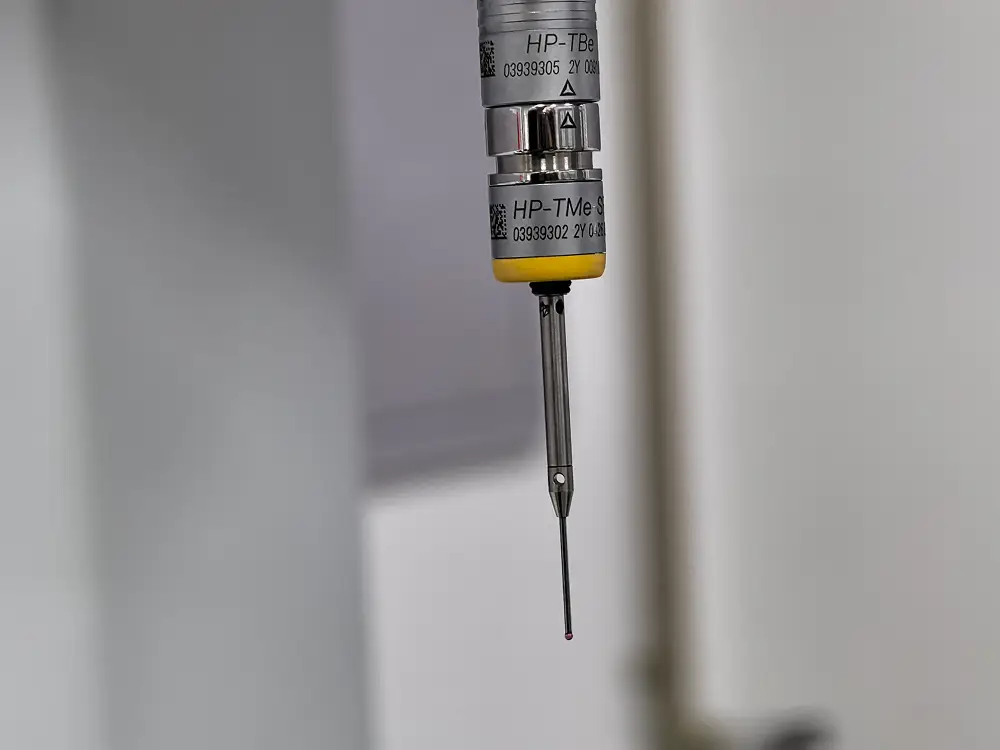
Dimensional inspection
Datums, bore sizes and mounting patterns measured against your drawing, with the method agreed before production.
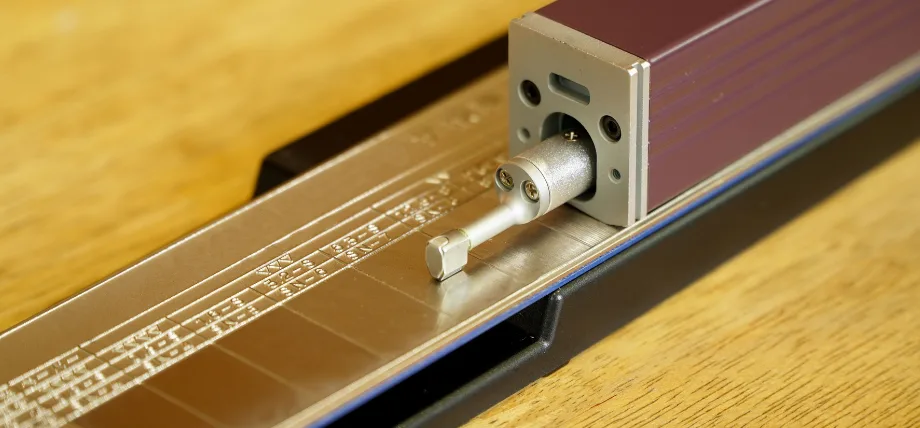
Surface roughness
Roughness measured where the drawing calls it out, on sealing, sliding and contact faces.
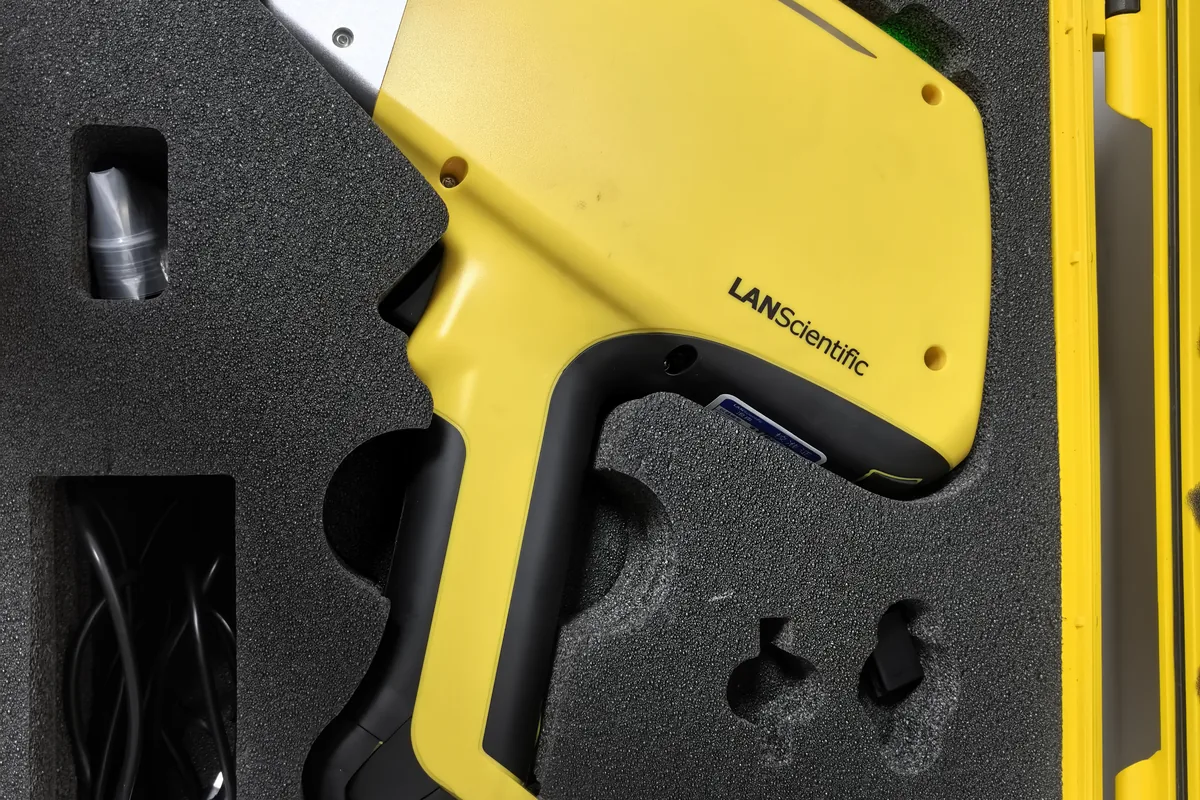
Material verification
Alloy grade checked before machining. Certificate scope is agreed with the material order, not added afterwards.
Where a programme requires verification we cannot give in-house, independent third-party testing or inspection can be arranged. The scope and the cost are agreed in the quote, not added later.
AGREED BEFORE THE ORDER STARTS
- 01Drawing revision, or the sample the part was measured from
- 02Material grade, hardness and the heat treatment specification
- 03Dimensional checks on the features that guarantee interchangeability
- 04Coating specification and corrosion requirement
- 05Batch quantity and how the order is identified
- 06Packing and rust protection for storage
APPROVED CASE STUDIES
Case studies for this application.
A case study needs approved objective, process, inspection and result records. We do not publish a project until that approval exists.
Case studies are being prepared for publication.
The part photographs above are workshop images of real geometry. They show what can be made, not a completed project: material, tolerance, quantity and delivery results are published only where the customer has approved the record. Until then, the fastest way to see whether your part fits our route is an engineering review.
QUESTIONS
Industrial equipment questions.
The questions that come up for this application. Anything not covered here goes to an engineer.
Can you make a spare from a worn sample?
Yes in many cases. A worn part gives nominal geometry, not the original tolerance. Send the drawing if one exists; otherwise we measure the sample and confirm what is inferred.
What if we only have a part number?
Send the number with any photo or dimensions. Without a drawing or sample we cannot quote a dimensional acceptance, and we will say so rather than guess.
Can you heat treat after machining?
Yes. Heat treatment changes dimensions, so the sequence and any final grinding or finishing allowance are agreed before the route is fixed.
Can you repeat a spare order later?
Yes. We keep the drawing revision and route record so a repeat batch is made to the same specification. Tell us if the revision has changed.
How is the lead time set?
From geometry, material availability, heat treatment and coating. The quote states a date for your part rather than a general promise.
START WITH YOUR DRAWING
Bring your next part
to an engineering review.
Send CAD or a drawing, quantity, material and critical requirements. We will review the manufacturing route, price and lead time.