
APPLICATION / MEDICAL
Medical equipmentMedical equipment parts.
Device housings and precision components with traceable materials.
Housings, instrument components and fixtures for medical equipment. We work to your material specification and drawing, with material traceability and the inspection records your project requires.
- TYPICAL PARTS
- Device housings, instrument components, assembly fixtures
- PRIMARY ROUTE
- CNC milling, CNC turning, Swiss turning
- COMMON MATERIALS
- Stainless steel 304 and 316L, aluminium, titanium, PEEK
SPECIFICATION
APPLICATION REQUIREMENTS
What decides the design here.
Four things shape the route before a tool is selected. If any of them is unknown at enquiry, we say so instead of assuming a default.
Read the design guideIntended use and contact conditions
Whether the component contacts the patient, a fluid path, or only the equipment structure. This drives material choice and surface requirements.
Cleaning and surface quality
Cleaning method, acceptable surface roughness and edge break. Crevices and burrs are usually the first thing a cleaning validation finds.
Material traceability
Grade, certificate source and whether the certificate has to accompany the parts.
Documentation scope
Which records your project needs: material certificate, dimensional report or a defined inspection sheet.
PARTS WE MAKE
Parts for this application,
and the geometry that shapes them.
Workshop photographs of real geometry. Each one carries the route, what the machine has to reach, what is checked, and what you need to state on the drawing.
See more part geometry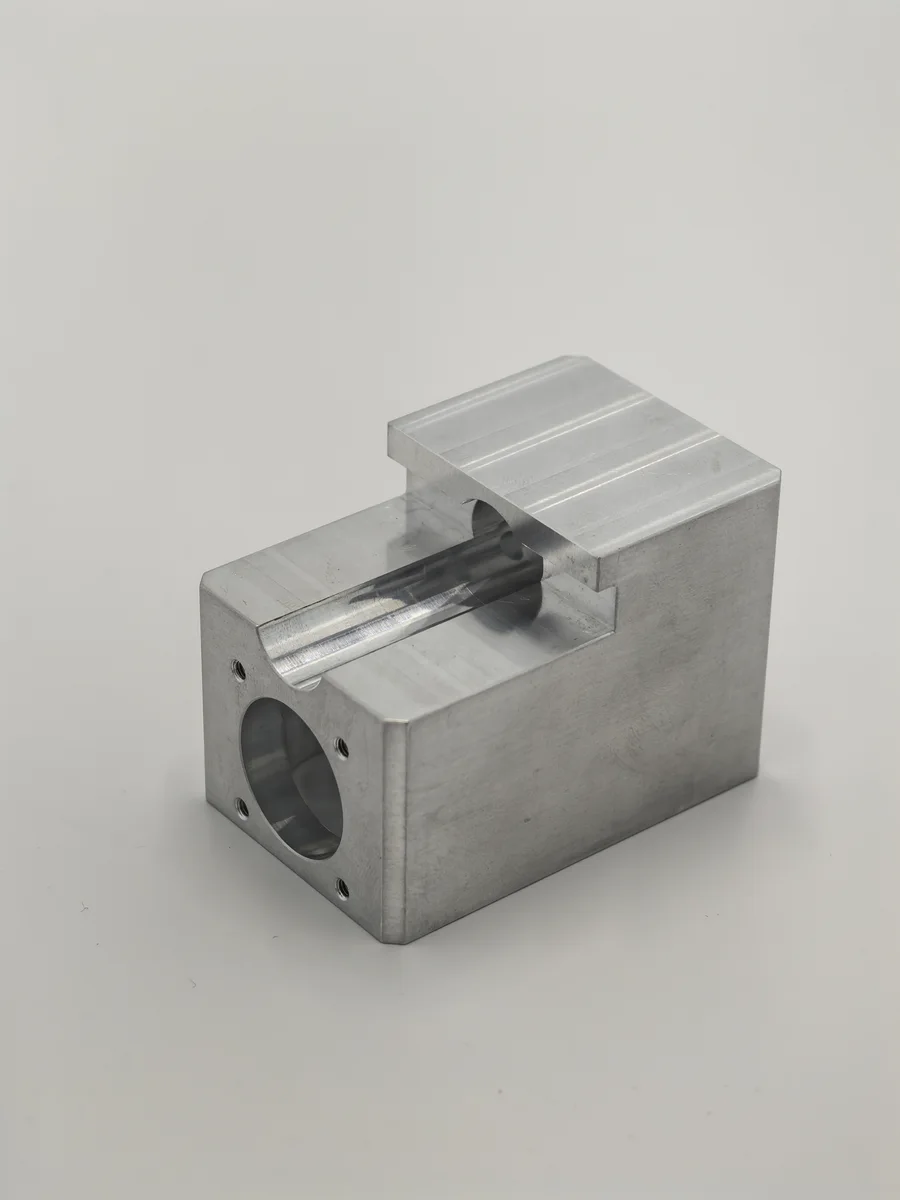
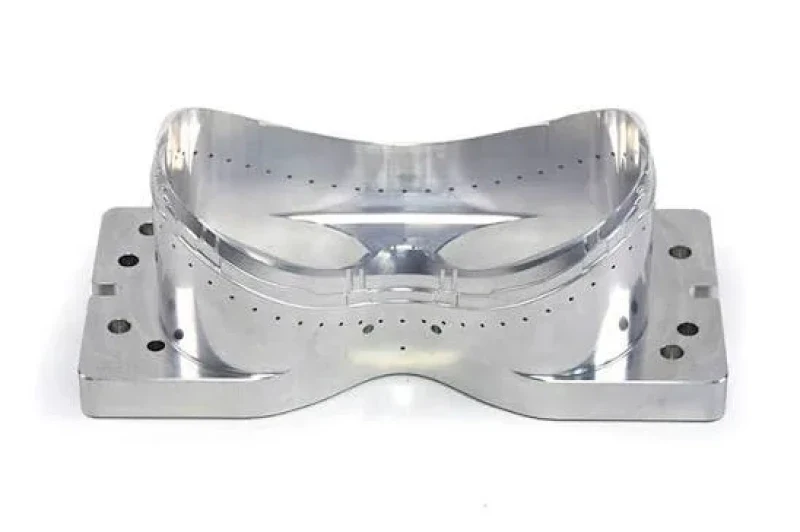
Device housing
Bores, sealing faces and the wall sections around them, plus how the housing closes. Crevices at the joint are what a cleaning validation finds first.
Specify the mating fit, the sealing face finish and any cosmetic surfaces.
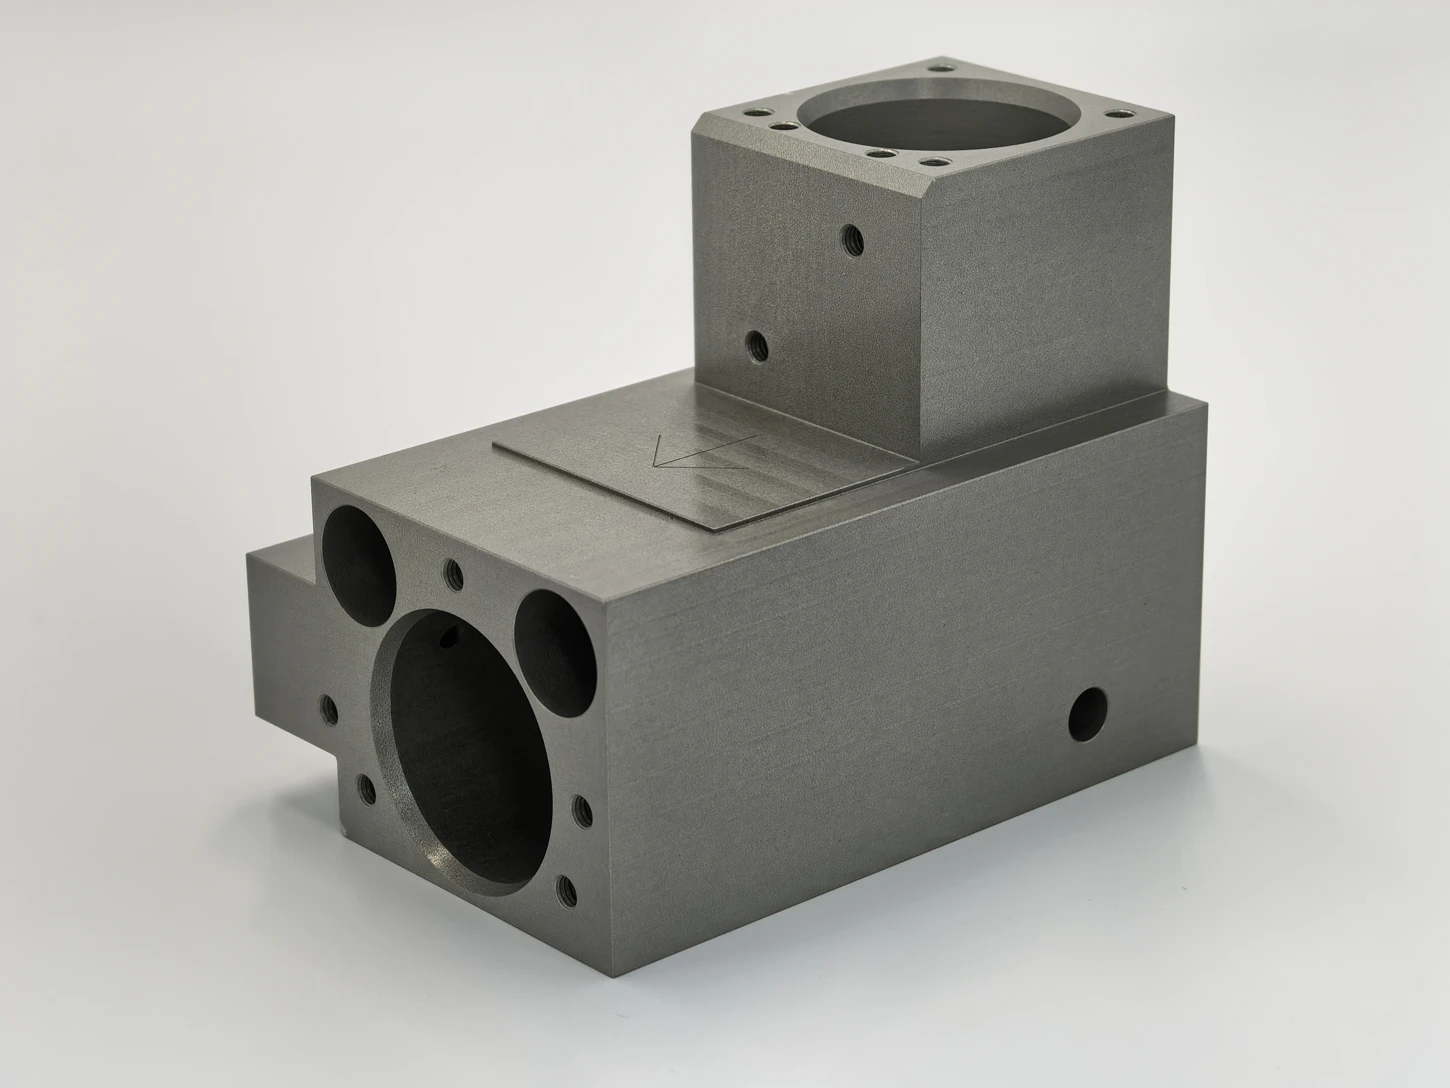
Instrument component with intersecting bores
Concentricity between intersecting bores and the mounting faces, and the burr condition at the intersection. A burr inside a bore is not a cosmetic defect.
Call out the bore sizes, the datum face and the deburring requirement.
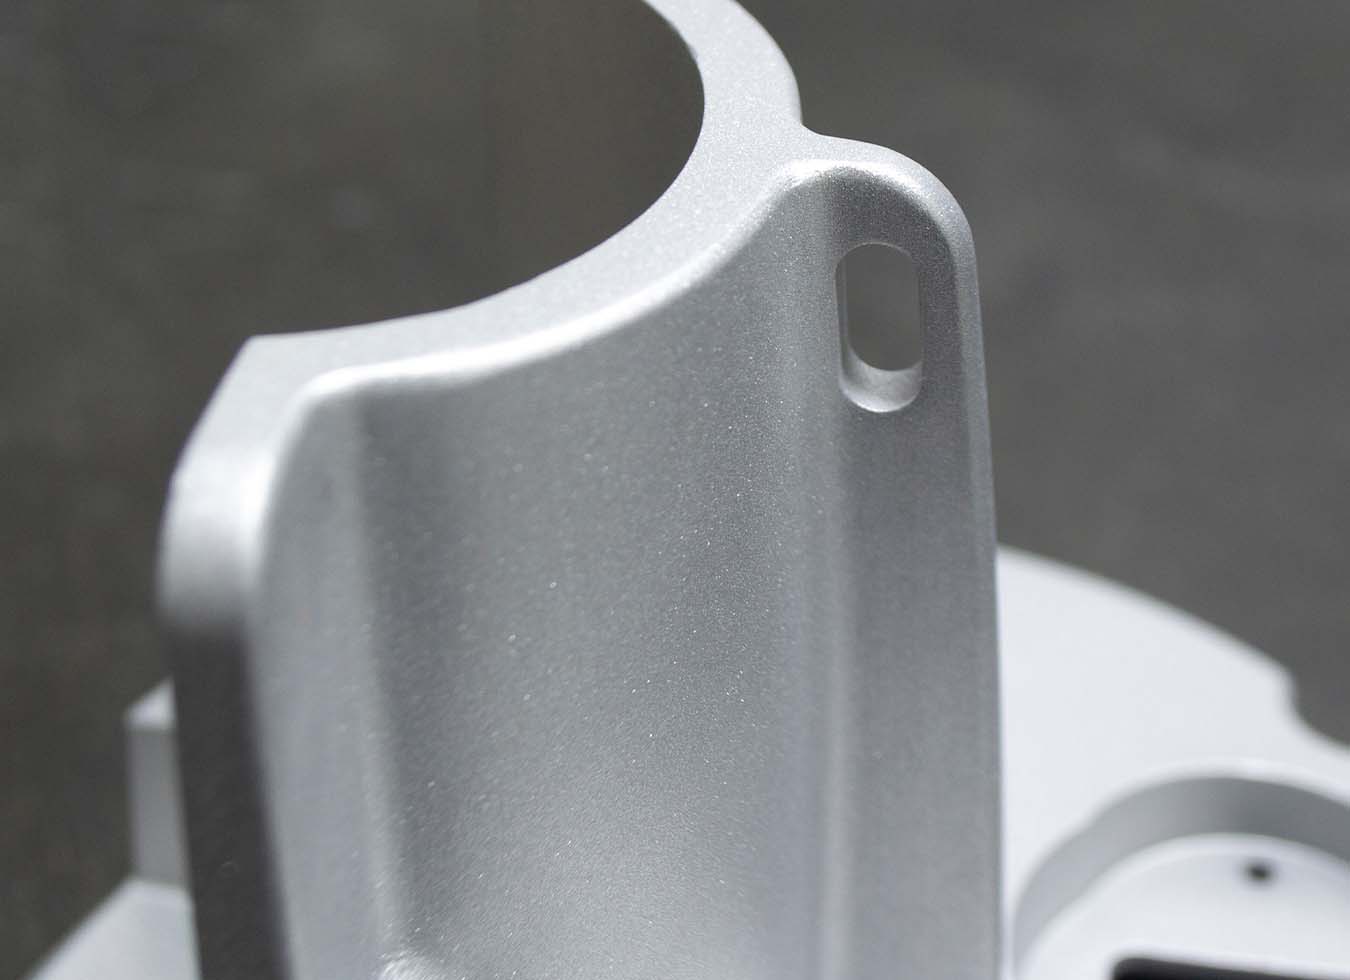
Uniform matt-finish component
A bead-blasted surface is uniform and hides tool marks, but it also rounds edges and holds residue if the roughness is not specified. Cleaning method and roughness go together.
State the roughness call-out, the cleaning method and which edges must stay sharp.
PROCESSES, MATERIALS AND FINISHES
The routes used for these parts.
Not every route suits every part. These are the ones that come up most for this application; the quote states the route chosen for your geometry and quantity.
All capabilitiesFINISHES AND TREATMENT
Finishing changes dimensions: coating thickness, masking and any effect on a mating fit are agreed before the route is fixed, not discovered at inspection.
INSPECTION AND DOCUMENTATION
What we measure, and what we record.
The inspection scope is agreed with the order. Anything you need recorded has to be stated before machining starts, because it cannot be reconstructed afterwards.
Tolerancing standards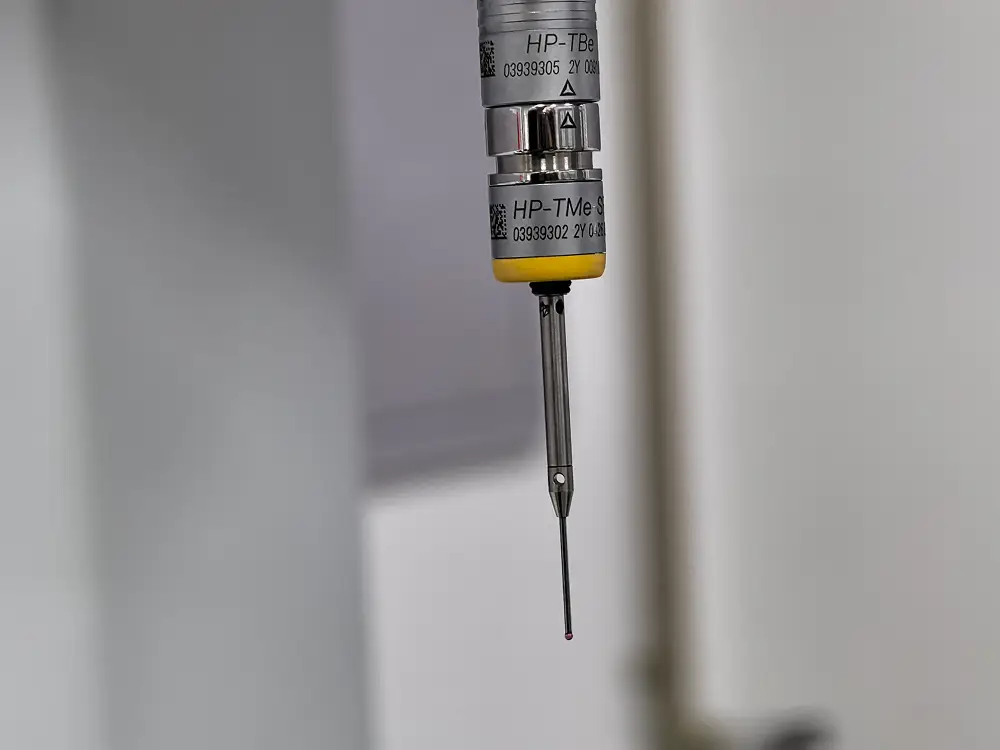
Dimensional inspection
Datums, bore sizes and mounting patterns measured against your drawing, with the method agreed before production.
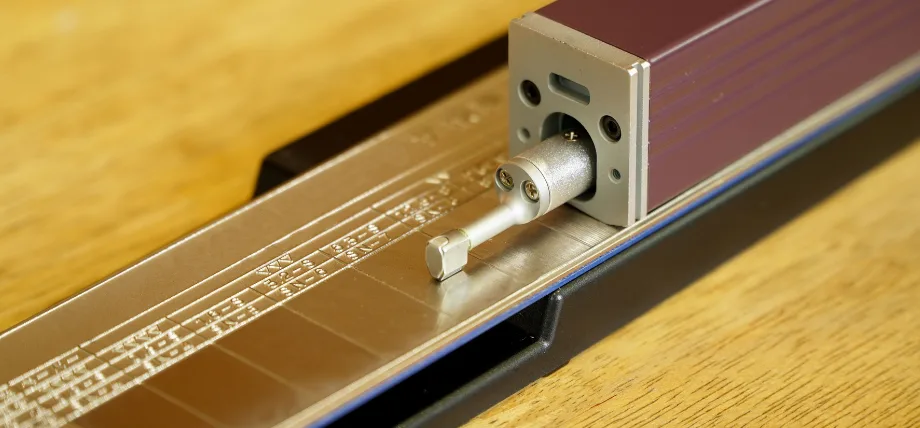
Surface roughness
Roughness measured where the drawing calls it out, on sealing, sliding and contact faces.
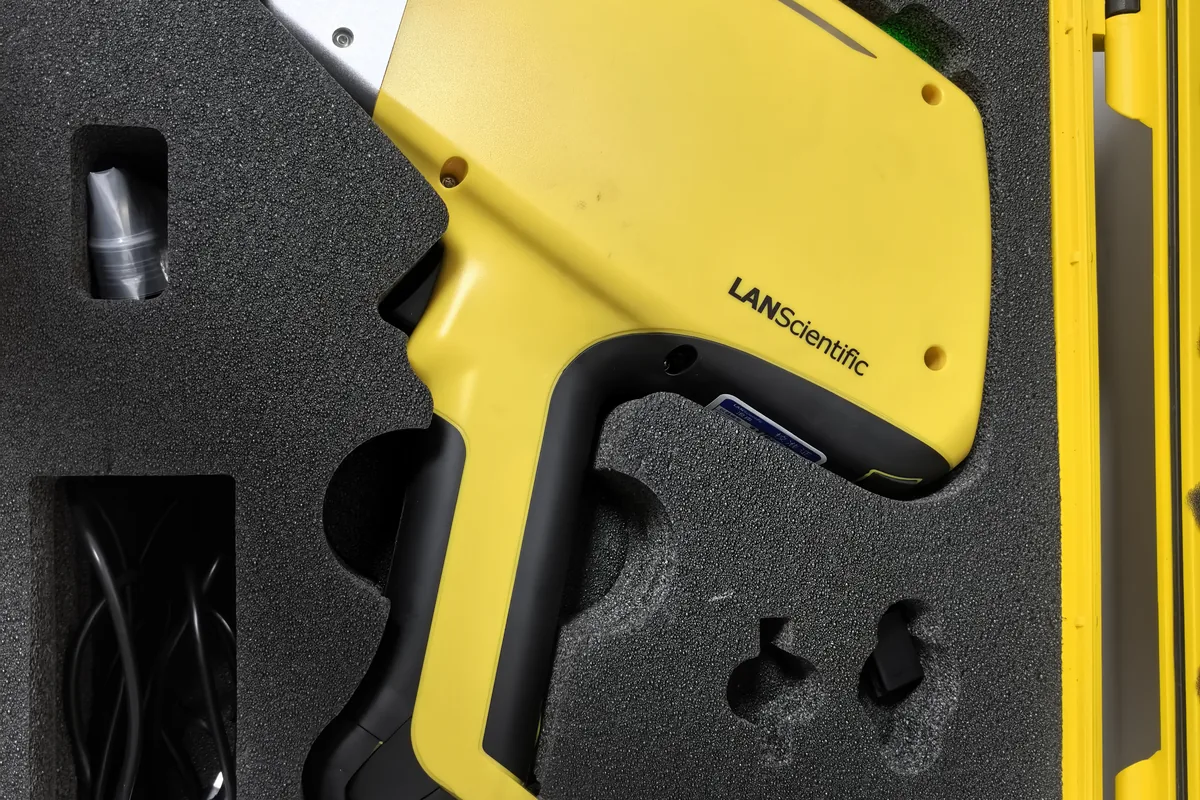
Material verification
Alloy grade checked before machining. Certificate scope is agreed with the material order, not added afterwards.
Where a programme requires verification we cannot give in-house, independent third-party testing or inspection can be arranged. The scope and the cost are agreed in the quote, not added later.
AGREED BEFORE THE ORDER STARTS
- 01Drawing revision and the intended use of the component
- 02Material grade, specification and certificate source
- 03Surface roughness call-outs on contact and cleaning faces
- 04Edge-break and deburring requirements
- 05Dimensional report scope and inspection method
- 06Cleaning, handling and packing instructions
APPROVED CASE STUDIES
Case studies for this application.
A case study needs approved objective, process, inspection and result records. We do not publish a project until that approval exists.
Case studies are being prepared for publication.
The part photographs above are workshop images of real geometry. They show what can be made, not a completed project: material, tolerance, quantity and delivery results are published only where the customer has approved the record. Until then, the fastest way to see whether your part fits our route is an engineering review.
QUESTIONS
Medical questions.
The questions that come up for this application. Anything not covered here goes to an engineer.
Are you ISO 13485 certified?
No. We hold ISO 9001:2015 through SGS. We can supply material certificates, dimensional reports and the inspection records you specify; we do not manufacture under an ISO 13485 quality system. Where your project needs independent verification, third-party testing can be arranged and the scope agreed in the quote.
Can you supply implantable or sterile components?
No. Our scope is equipment hardware and non-implantable components. Anything entering a sterile or implantable pathway is outside what we take on.
Can you provide material certificates?
Yes where the material is supplied with certification. State the certificate type when you request the quote so it can be sourced with the material.
What surface finish is realistic on a cleaning face?
It depends on the material and the geometry. Give the roughness call-out and the cleaning method, and we confirm what the route can hold before quoting.
How is the lead time set?
From geometry, material sourcing and inspection scope. Certificate and documentation requirements are part of that, so they need to be stated at enquiry.
START WITH YOUR DRAWING
Bring your next part
to an engineering review.
Send CAD or a drawing, quantity, material and critical requirements. We will review the manufacturing route, price and lead time.